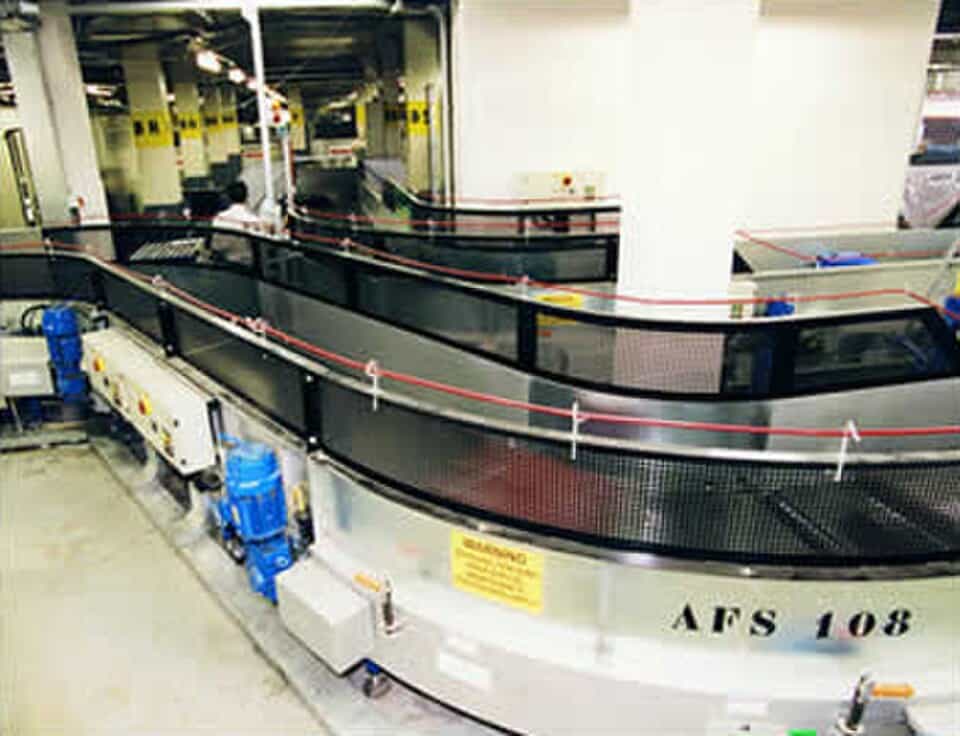
A sorter goes down. Not the entire system — just one zone, but it feeds your outbound shipping lanes. Your on-call technician is 90 minutes out. The part you need is sitting in a warehouse in another state. By the time the system comes back up, six hours have passed, two outbound trucks are gone, and your labor cost has doubled.
Here’s what makes it worse: this wasn’t a surprise. The wear pattern on that sorter had been building for months. A scheduled preventive maintenance visit would have caught it. Nobody scheduled one.
With unplanned downtime averaging $86 a minute, that six-hour outage didn’t cost a repair bill. It cost over $30,000 before anyone touched a wrench.
Reactive Maintenance Doesn’t Just Cost You a Repair Bill
The repair invoice is the smallest number in a reactive maintenance event. Three costs dwarf it, and none of them show up on the service ticket.
Throughput loss
Every hour a sortation system is down during peak can mean thousands of units stuck in queue, missed carrier pickups, and SLA penalties no repair bill accounts for. The repair is a line item; the missed trucks are a customer conversation.
Emergency parts premiums
When a critical component fails without warning, expedited freight and after-hours sourcing can multiply your parts cost three or four times over what a scheduled program would have paid for the same component. Same photo eye, same motor — triple the price, because it’s 3 AM and it’s in another state.
The damage that doesn’t announce itself
Power events, hard jams, and surge loads create secondary damage that doesn’t always show up right away. A system that came back up after an outage may be running, but not at full health — and the next failure is already building.
That last one deserves emphasis, because it’s the trap most operations fall into: “it came back up” is not the same as “it’s fine.” One means the system is running. The other means you understand what it took to get there and you have a plan to keep it running.
What a Preventive Maintenance Program Actually Looks Like
Century’s maintenance program is built around one principle: the best service call is the one you scheduled, not the one you had to make at midnight. Our field teams operate coast to coast, with experience across major conveyor brands and control systems — so we know what breaks, and when. Three components do the heavy lifting.
Scheduled PM visits tied to your duty cycle
Conveyor maintenance frequency should follow how hard the system works, not a calendar default. Operations running around the clock receive a minimum of four preventive maintenance visits per year. Each visit is a structured inspection of wear patterns — belts, bearings, photo eyes, sortation components — so failures get caught as line items on a schedule instead of emergencies on a Saturday.
Rapid response with remote diagnostics
Unplanned events still happen; a good program shrinks them. When something goes down, remote VPN diagnostics let our technicians identify the issue before a truck ever rolls — often turning a 90-minute drive plus diagnosis into a phone call plus a targeted dispatch with the right part on board.
Critical parts on hand
Known critical parts, stocked for your specific system. No scrambling for a photo eye or a motor at 3 AM when your operation can’t wait for next-day freight. The parts list comes out of the PM program itself: what’s wearing tells you what to shelve.
How to Tell Which Side of the Line You’re On
A quick self-assessment. If more than a couple of these are true, you’re running a reactive operation whether you call it that or not:
Your last three service calls were emergencies, not scheduled visits
You don’t have a documented critical-spares list for your system
Nobody can say when each zone was last formally inspected
A system that “came back up” after an event was never fully assessed afterward
Peak-season planning doesn’t include a pre-peak equipment review
None of these are equipment problems. They’re program problems — and program problems are the cheap kind to fix, because the fix is a decision, not a capital project.
Before Peak Arrives, Schedule a Service Review
The difference between planned and reactive is one phone call — the question is whether you make it before the failure or after.
A service review looks at what you have, what’s wearing, and what you should have on the shelf before you need it. No commitment required — just a clear picture of where your operation stands before peak makes the assessment for you.
When a warehouse, distribution center, or fulfillment operation needs more than a standalone conveyor, the role of a conveyor system integrator becomes especially important. A system integrator brings together conveyor equipment, controls, robotics, software, engineering, installation, and ongoing service so the individual components operate as one coordinated system.
Century Conveyor Systems approaches material handling automation as a complete system rather than simply an equipment purchase. The company describes itself as a full-service integrator for shipping warehouses, distribution centers, and fulfillment facilities, with capabilities spanning system design, validation, installation, startup support, parts, and service.
Below are frequently asked questions about Century Conveyor Systems and its role as a conveyor system integrator.
Table of Contents
What does a conveyor system integrator do?
A conveyor system integrator helps businesses design and implement a material handling system that fits the way products actually move through a facility.
Instead of treating a conveyor as an isolated piece of equipment, an integrator considers the complete workflow. That can include receiving, transportation, accumulation, picking, packing, sortation, pallet handling, order fulfillment, and shipping. The objective is to create a coordinated system in which equipment and controls work together to move products efficiently from one stage to another.
Century Conveyor Systems takes this broader approach. Its services include system design, controls engineering, control panel design and fabrication, electrical installation, mechanical engineering, mechanical installation, project management, and project phasing. The company also provides conveyor preventative maintenance, repair services, and replacement parts.
That combination is important because conveyor projects can involve many interdependent decisions. Conveyor type, product characteristics, throughput requirements, available floor space, controls, operator interaction, and downstream processes can all affect the final design.
For example, a facility handling small polybags may have different conveying requirements from one moving heavy pallets or oversized bulk products. Century identifies several conveyor technologies for different applications, including live roller, gravity, belted, modular belt, pallet, spiral, and extendable conveyors.
In other words, a conveyor system integrator is responsible for helping connect the individual pieces into a functional material handling solution—not simply supplying a conveyor section.
Why work with Century Conveyor Systems instead of purchasing individual conveyor equipment?
One of the primary advantages of working with a conveyor system integrator is having a single organization involved across multiple stages of the project.
A warehouse automation project can require mechanical equipment, electrical infrastructure, controls, software, robotics, installation, testing, and ongoing maintenance. Purchasing each component independently can leave the facility owner responsible for coordinating multiple vendors and determining how those components will interact.
Century’s approach is structured around managing the project as a complete system. The company states that it can manage projects from system design and validation through final installation, startup support, and lifetime parts and service.
This can be particularly relevant when a project involves more than conventional conveyor equipment. Century’s listed capabilities extend into programmable logic controls, warehouse management systems, warehouse control systems, robotic fulfillment, robotic palletizing, sortation, print and apply, storage systems, and retrofit and modernization.
That broader scope allows the conveyor to be considered in relation to the rest of the operation.
For example, a fulfillment center might need conveyors to transport cartons while also requiring automated sortation and robotic movement between work areas. Designing those functions independently could create compatibility or workflow challenges. An integrator can instead look at the movement of products across the entire process and determine how the different technologies should interact.
The result is a project centered on the facility’s material flow rather than on an individual piece of equipment.
What types of conveyor systems can Century Conveyor Systems integrate?
Century works with several conveyor configurations, allowing systems to be designed around the products being handled and the specific processes within a facility.
Live roller and gravity conveyors, for example, can be used in packing lines, divert lines, extendable applications, and end-of-line operations. Live roller conveyors use powered rollers, while gravity conveyors rely on gravity to move products.
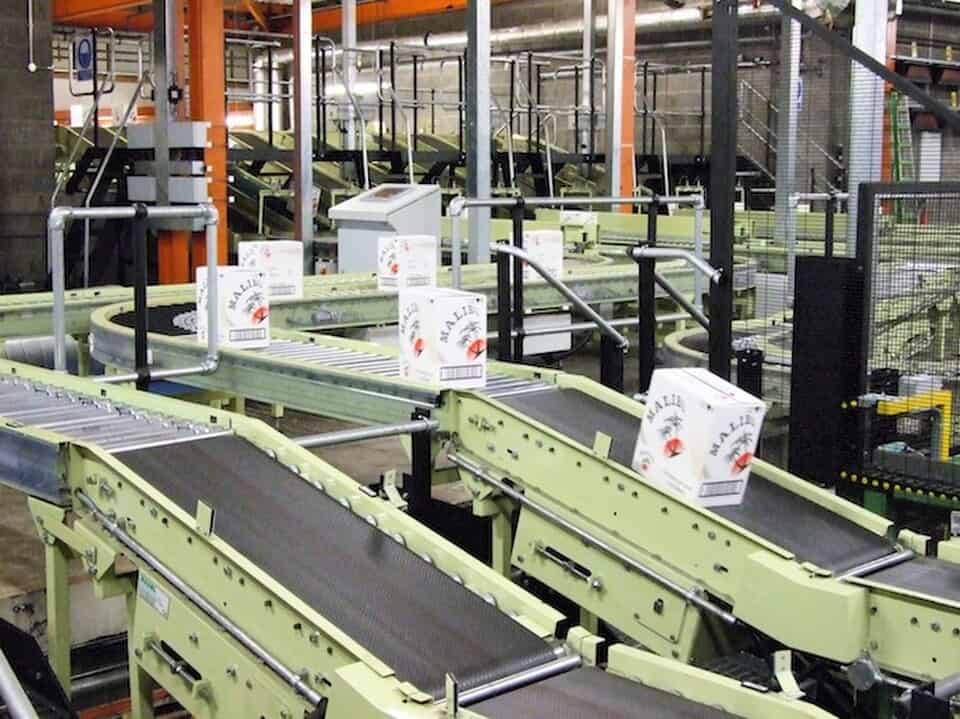
Belted conveyors provide another option when product stability is particularly important. Century notes that belt-over conveyors can be useful for small polybags, parcels, and irregular carton sizes. Their ability to handle inclines, declines, and gapping can also make them useful when faster or more controlled movement is required.
Modular belt conveyors offer another specialized approach. Their individual belt sections can be removed, cleaned, or modified, which can be valuable in applications where cleaning, traction, tight transfers, or accumulation are important considerations.
For facilities handling pallets or heavier loads, Century offers several pallet conveyor configurations, including pallet drag chain, pallet gravity, chain-driven live roller, and Poly-V conveyors.
The company also works with conveyor diverts, zero- and minimum-pressure accumulation, telescoping extendable conveyors, and spiral conveyors.
This variety matters because there is no single conveyor design that works equally well for every warehouse. Product dimensions, weight, packaging, speed, accumulation requirements, transfer points, and facility layout all influence the appropriate equipment.
A conveyor system integrator can therefore serve as the engineering layer between the operational requirement and the equipment selection.
Can a conveyor system integrator incorporate robotics into fulfillment operations?
Yes. Modern warehouse automation increasingly combines traditional conveyor systems with robotic technologies, and Century’s fulfillment solutions include both conveyors and robotic order fulfillment.
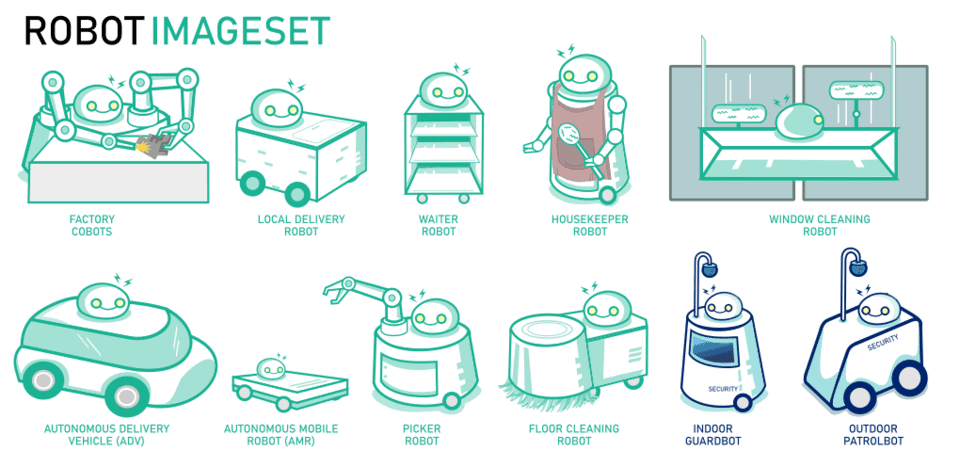
Century identifies automated guided vehicles, or AGVs, and autonomous mobile robots, or AMRs, as robotic fulfillment technologies. These systems can provide transportation capabilities within a facility and can complement conveyor-based material handling.
AGVs can follow defined navigation systems and are suited to applications involving pallets, cartons, or other materials traveling along established routes. Century notes that AGVs can also be equipped with conveyor or cart attachments depending on the products being handled.
AMRs take a different approach. Rather than following a fixed track, they use sensors and programming to navigate through a facility. This makes them useful for applications in which movement patterns need to be more flexible.
The distinction can be important when designing a fulfillment system.
A conveyor is a fixed infrastructure solution. It provides predictable transportation along an engineered route. An AMR, by contrast, can move dynamically through a facility. Combining the two can allow an operation to use fixed conveyor infrastructure where it makes sense while introducing mobile automation where flexibility is more valuable.
Century specifically identifies goods-to-person fulfillment as a use case for AMRs. In such an arrangement, robots can retrieve totes and bring them to packing lines or fulfillment personnel.
For businesses considering warehouse automation, this illustrates why choosing a conveyor system integrator can be more comprehensive than choosing a conveyor manufacturer alone. The integrator can evaluate where conveyors, robots, controls, and other technologies fit within the overall workflow.
How does Century approach order fulfillment automation?
Order fulfillment involves considerably more than transporting a box from one location to another. Products need to move through multiple stages, and each transition can influence throughput, accuracy, labor requirements, and product handling.
Century describes its order fulfillment approach around optimizing the system at each touchpoint. Its stated objectives include improving output performance, reducing errors that can contribute to returns or product breakage, and processing items faster with fewer manual interactions.
Conveyors can form the transportation backbone of this type of operation. They can move cartons between workstations, provide accumulation, create routing opportunities through diverts, and connect different parts of a warehouse.
Sortation can then direct products toward the appropriate destination. Robotic technologies can provide additional transportation or goods-to-person functionality. Controls and software can coordinate equipment and processes.
This creates a layered automation strategy rather than a single piece of machinery.
For example, a fulfillment operation might use belt conveyors for stable movement of small parcels, accumulation conveyors near packing areas, diverts to route orders, and AMRs for flexible transportation between selected zones. The exact configuration would depend on the facility and its operating requirements.
The important point is that an integrator can evaluate those technologies together.
Can Century help modernize an existing conveyor system?
A conveyor system integrator can also play a role when a company does not need an entirely new warehouse.
Existing facilities may have conveyor equipment that remains mechanically useful but lacks the controls, capacity, automation, or flexibility needed for current operations. Replacing the entire system may not always be the only approach.
Century lists retrofit and modernization among its solution capabilities. Its broader services also include controls engineering, programmable logic controls, warehouse control systems, mechanical and electrical installation, and conveyor service.
Modernization can therefore involve evaluating the existing infrastructure and identifying where improvements could have the greatest operational impact.
Depending on the project, that might mean upgrading controls, changing conveyor sections, adding automation, improving sortation, introducing robotic equipment, or modifying the system to accommodate changes in products and workflows.
The advantage of involving an integrator is that the existing system can be considered as part of the larger operation. Rather than simply replacing individual components, the project can be evaluated around the facility’s current requirements and future objectives.
What happens after a conveyor system is installed?
Installation is only one stage of a material handling automation project.
Conveyor equipment operates in demanding environments, and routine maintenance, replacement parts, troubleshooting, and repairs can become important aspects of keeping a facility running.
Century provides conveyor system integrator service and parts capabilities in addition to its engineering and installation services. The company states that it has a conveyor maintenance and service department, service vehicles, and more than 40 years of conveyor experience. Its listed services include preventative maintenance, repair, replacement parts, and equipment installation.
This ongoing support is another reason the role of a conveyor system integrator can extend well beyond the initial project.
A system integrator that understands the original design has context about how the equipment, controls, and related technologies were intended to operate. That knowledge can be useful when maintenance or modifications become necessary later.
Century also describes a parts ordering portal designed to give participating customers visibility into relevant system parts and part numbers, with the goal of simplifying the process of identifying and requesting replacement components.
For a facility dependent on automated material handling, lifecycle support can be an important part of the overall system strategy.
Is Century Conveyor Systems’s conveyor system integrator suitable for large warehouse automation projects?
Century positions itself as a turnkey automation integrator for warehouses, distribution centers, and fulfillment facilities. Its capabilities cover multiple areas of material handling automation, including conveyor systems, sortation, robotic fulfillment, robotic palletizing, controls and software, storage systems, print and apply, and service.
The company’s website also reports more than 1,500 installations over the preceding five years and identifies offices in New Jersey, California, and Kentucky.
Project scale, however, is only one consideration when evaluating an integrator. The more important question is whether the integrator’s engineering, automation, installation, controls, and support capabilities correspond with the requirements of the particular facility.
A warehouse may need a straightforward conveyor expansion, while another operation may require a combination of conveyor transportation, sortation, robotics, warehouse controls, and pallet automation.
A consultation can help establish which combination of technologies is appropriate.
What should a company discuss with a conveyor system integrator before starting a project?
The most productive conversations usually begin with the operation rather than a specific piece of equipment.
A company evaluating automation should be prepared to discuss the products being handled, package dimensions, product weights, current throughput, desired throughput, order profiles, facility dimensions, existing equipment, staffing, bottlenecks, accumulation requirements, shipping processes, and future growth.
It is also useful to identify whether the project involves a new facility, an expansion, or modernization of an existing system.
From there, an integrator can evaluate potential combinations of equipment and automation.
Century’s stated approach of “Design. Build. Support.” reflects this project lifecycle. The company describes capabilities covering system design and validation, installation and startup, and continuing parts and service.
For a business searching for a conveyor system integrator, this broader perspective is ultimately the key consideration: the conveyor should be designed around the material flow and operational objectives of the facility, rather than selecting equipment first and attempting to make it fit afterward.
What makes a conveyor system integrator important for the future of warehouse automation?
Warehouse automation continues to expand beyond conventional conveyor transportation. Facilities increasingly have to consider robotics, controls, software, sortation, goods-to-person processes, automated palletizing, and other technologies alongside traditional conveying.
That makes conveyor system integrator important.
Century Conveyor Systems’s conveyor system interrogators provides capabilities across these different categories, including conventional conveyor systems, robotic fulfillment, palletizing, controls and software, sortation, storage, and ongoing service. Its order fulfillment solutions also demonstrate how fixed conveyor infrastructure can work alongside mobile robotics such as AGVs and AMRs.
The practical value of an integrator is therefore its ability to view automation as a connected system.
For a facility planning a new material handling project, expanding an existing operation, or modernizing an aging system, working with a conveyor system integrator can provide a way to address engineering, equipment, controls, installation, and lifecycle support within one broader project framework.
Century Conveyor Systems’ approach centers on that full-system perspective, helping warehouses and distribution facilities move from individual automation components toward an integrated material handling operation.
Warehouse operations are under constant pressure to move products faster and adapt to changing order volumes. That is where automation in warehousing becomes an important part of modern material handling strategy.
For companies evaluating warehouse automation, the challenge is rarely finding a single piece of equipment. A successful automated operation requires multiple systems to work together—from conveyors and sortation equipment to robotics, controls, warehouse software, storage systems, and ongoing service.
Century Conveyor Systems approaches automation as an integrated material handling solution. The company designs and implements automated systems for warehouses, distribution centers, and fulfillment facilities, with capabilities that extend from system design and controls engineering through installation, startup, service, and parts support.
Below are some of the most common questions about Century Conveyor Systems and its approach to automation in warehousing.
Table of Contents
What does automation in warehousing mean for Century Conveyor Systems?
For Century Conveyor Systems, automation in warehousing is about creating a connected material handling system that moves products through a facility with less unnecessary manual intervention.
Rather than treating automation as one machine or one conveyor, Century works across multiple stages of warehouse operations. Its solutions include conveyor systems, sortation, robotic fulfillment, robotic palletizing, controls and software, storage modules, print-and-apply equipment, and related service and maintenance capabilities.
The company describes itself as a full-service system integrator for shipping warehouses, distribution centers, and fulfillment facilities. Its engineers can design, validate, and implement turnkey systems intended to improve output while reducing labor requirements.
That integrated approach matters because warehouse processes are interconnected. A conveyor that moves cartons efficiently is only one part of the operation. Products may also need to be inducted, accumulated, diverted, sorted, picked, packed, labeled, palletized, and transported to shipping. Automation has to account for how each of those activities affects the others.
Century’s approach therefore centers on designing an automation system around the specific flow of goods through a facility rather than treating individual pieces of equipment as isolated upgrades.
How can Century Conveyor Systems automate the movement of products inside a warehouse?
Conveyors form one of the core elements of Century’s approach to warehouse automation. They provide a continuous method for moving cartons, packages, pallets, and other materials between operational areas.
Century offers several conveyor configurations because different products and warehouse processes require different handling characteristics. Live roller and gravity conveyors, for example, can be useful in packing lines, divert areas, extendable applications, and end-of-line operations. Belted conveyors can provide stable handling for smaller parcels, polybags, and irregular carton sizes. Modular belt conveyors offer another option where cleaning, maintenance, traction, or specialized handling requirements are important.
The company also provides conveyor diverts that can route products from one line to another. This can allow cartons to be directed toward specific processing or shipping destinations without necessarily requiring a large standalone sortation system for every application.
Accumulation is another important consideration. Zero-pressure and minimum-pressure conveyor systems can help manage product spacing and reduce contact between items. This is particularly relevant when fragile products need to be moved without unnecessary collisions.
For warehouses handling pallets or oversized loads, Century also provides pallet conveyor solutions, including drag chain, gravity, chain-driven live roller, and Poly-V configurations.
The key point is that conveyor automation is not simply about moving products from Point A to Point B. The conveyor configuration, speed, accumulation strategy, product characteristics, and interaction with other equipment all influence how effectively the overall warehouse operates.
How does robotic automation fit into Century Conveyor Systems’ warehouse solutions?
Robotics provides another layer of automation in warehousing, particularly for facilities that need greater flexibility in transporting goods.
Century’s robotic fulfillment solutions include automated guided vehicles (AGVs) and autonomous mobile robots (AMRs). Both can transport materials around a facility, but they operate differently.
AGVs generally follow defined routes using technologies such as magnetic tape, QR codes, inductive wires, or laser-based systems. They can be configured to transport pallets, cartons, and other materials along established paths. Century notes that AGVs can also be fitted with conveyor or cart attachments and can interface with conveyor systems.
AMRs provide a different approach. Rather than following a fixed track, they use sensors and programming to navigate through a facility. That makes them suitable for environments where routes may need to change or where goods need to be transported between different locations.
Century identifies goods-to-person fulfillment as a key application for AMRs. Instead of requiring an employee to travel throughout a warehouse to retrieve inventory, an AMR can transport totes, cartons, or carts to a workstation or packing area.
This distinction is important when evaluating automation. A fixed conveyor may be appropriate for predictable, high-volume transportation between established points, while mobile robotics can provide additional flexibility where warehouse layouts, workflows, or transportation requirements change.
Can automation in warehousing help improve order fulfillment?
Yes. Order fulfillment is one of the central applications for automation in warehousing, and Century specifically focuses on automating the movement of products throughout the fulfillment process.
Order fulfillment encompasses the activities that occur between receiving an order and getting the product to the shipping dock. Depending on the facility, that can involve picking, transportation, accumulation, sortation, packing, labeling, and loading.
Century’s order fulfillment approach is designed around improving output performance, reducing errors that can contribute to returns or product damage, and processing items with fewer manual interactions.
Conveyor automation can help establish predictable product movement between work areas. Sortation equipment can direct products toward appropriate destinations. Robotic systems can transport totes or cartons. Print-and-apply equipment can automate labeling-related processes, while palletizing systems can automate the placement and preparation of products on pallets.
The value comes from coordinating these technologies rather than simply adding automation wherever space is available.
A warehouse that automates one isolated process may still have bottlenecks elsewhere. For example, faster picking does not necessarily improve total throughput if products then accumulate at packing or shipping. A properly engineered fulfillment system considers the entire flow so that individual improvements support the performance of the broader operation.
What types of automation in warehousing equipment does Century Conveyor Systems offer?
Century’s range of solutions covers several major areas of warehouse material handling.
Conveyor systems are available for cartons, parcels, pallets, and other loads. Sortation systems can distribute products to different destinations. Robotic fulfillment solutions provide automated transportation through AGVs and AMRs.
The company also works with robotic palletizing and depalletizing systems, including robotic arms and cells as well as associated shrink-wrapping and strapping equipment. These technologies can automate repetitive pallet-handling tasks at the beginning or end of a material flow.
Controls and software provide another critical layer. Century lists control panel fabrication, programmable logic controls, warehouse management systems, and warehouse control systems among its capabilities.
Storage solutions include shelving and racking, ergonomic picking and packing systems, automated storage and retrieval systems, mezzanines, platforms, and warehouse structures.
There are also print-and-apply solutions, including case formers, sealers, erectors, dunnage dispensers, fillers, tapers, shipping label applicators, and related terminals.
This breadth allows a warehouse project to address multiple stages of material handling through a coordinated automation strategy instead of relying on disconnected equipment suppliers for every portion of the system.
How does Century approach controls and automation in warehousing software?
Physical automation equipment needs a control layer to coordinate how products move through a warehouse. This is why controls and software are an important part of Century’s automation capabilities.
The company works with programmable logic controls, control panel fabrication, warehouse management systems, and warehouse control systems.
In an automated warehouse, these technologies can help coordinate equipment and communicate information about material movement. The control system can be responsible for determining how equipment responds to sensors, product locations, routing requirements, and other operational inputs.
This is particularly important as a facility becomes more automated. Adding conveyors, robots, sortation, or other machinery without considering how those systems communicate can create operational complexity rather than eliminating it.
Century’s system-integration model brings engineering, controls, equipment, installation, and project management into the same overall project. That provides a framework for considering the control architecture alongside the physical warehouse layout.
For businesses planning automation, this is an important distinction: the goal is not simply to purchase automated equipment, but to create a system in which the equipment, controls, software, and warehouse processes operate together.
Can Century automate an existing warehouse, or is automation in warehousing only for new facilities?
Automation in warehousing does not necessarily require building an entirely new facility. Existing operations can also be candidates for modernization.
Century lists retrofit and modernization among its solution capabilities. This is relevant for companies that already have conveyor systems, controls, storage equipment, or other material handling infrastructure but need to increase capacity or update outdated technology.
A retrofit can take many forms. A warehouse might replace or modify existing conveyors, add new automation to an established line, update controls, introduce robotics, improve sortation, or change the way products move between existing workstations.
The appropriate strategy depends on the condition of the existing system, available floor space, throughput requirements, product characteristics, and the desired future-state operation.
Modernization can also allow businesses to approach automation incrementally. Instead of attempting to replace an entire material handling system at once, certain processes may be upgraded while other infrastructure remains in service.
That makes system assessment an important starting point. Before determining which equipment to add, an integrator can evaluate how the current operation works and identify where automation can fit into the existing environment.
How does Century address maintenance after an automated system is installed?
Automation does not end when equipment is installed and started. Long-term maintenance is an important part of warehouse automation because a conveyor or robotic system that is unavailable cannot provide its intended operational value.
Century provides conveyor repair, preventative maintenance, replacement parts, equipment installation, and service capabilities. The company also identifies 24/7 support, conveyor preventative maintenance, electrical installation, mechanical installation, and project management among its services.
Its service department supports conveyor maintenance and repair, and the company provides replacement conveyor parts and equipment.
This ongoing support can be particularly important in automated facilities because equipment is often interconnected. A problem with one component can affect material flow elsewhere in the system.
Preventative maintenance can help identify wear or developing equipment issues before they become larger operational interruptions. Parts availability can also matter when a component needs to be replaced.
For businesses evaluating automation, service should therefore be considered alongside equipment specifications. The long-term performance of an automated warehouse depends not only on how the system is designed, but also on how it is maintained and supported after commissioning.
What makes Century Conveyor Systems’ approach different from simply buying automation in warehousing equipment?
The distinction is primarily the integration process.
A warehouse can purchase individual conveyors, robots, sorters, controls, or storage systems from different vendors. However, individual equipment purchases do not automatically create an efficient automated workflow.
Century positions itself as a turnkey system integrator, meaning the company can participate across system design, validation, installation, startup support, and ongoing service.
That approach allows the warehouse’s operational requirements to remain central to equipment decisions.
For example, a project might combine conveyors with robotic fulfillment, controls, sortation, pallet handling, storage systems, and print-and-apply equipment. Each technology performs a different job, but the warehouse needs them to function as one material handling process.
The engineering process therefore becomes just as important as the equipment itself. Product dimensions, weights, throughput requirements, facility layout, accumulation requirements, operator interaction, shipping patterns, and future capacity can all influence the final system.
This is one reason automation in warehousing is best considered a systems-engineering challenge rather than simply an equipment-purchasing exercise.
Is automation in warehousing scalable as a company’s needs change?
Scalability is a significant consideration when designing automation, particularly for businesses whose order volumes or product mix can change over time.
Century identifies its robotic fulfillment systems as scalable, noting that additional systems can be implemented as needed. AMRs in particular can provide flexibility because they are not permanently fixed to a conveyor route in the same way as traditional equipment.
Conveyor systems can also be designed with different sections and functions, allowing a warehouse to create a material flow suited to its current requirements while considering future expansion.
Scalability does not mean that every warehouse should automate everything immediately. Instead, it means the initial system should be designed with realistic future requirements in mind.
For example, a facility may initially automate transportation between picking and packing while leaving certain processes manual. As order volume grows, additional robotics, sortation, conveyor capacity, storage automation, or packaging equipment may be incorporated.
A scalable approach can therefore help businesses avoid designing a system that meets today’s requirements but creates significant constraints when the operation expands.
What should a warehouse consider before investing in automation?
The most important starting point is understanding the warehouse’s actual material flow.
Businesses should consider what products they handle, how those products enter and leave the facility, how many orders are processed, where bottlenecks occur, how much manual transportation is involved, what types of errors occur, and what future capacity is expected.
Product characteristics also matter. Cartons, polybags, pallets, drums, oversized products, fragile items, and irregular packages may require different handling methods.
The physical facility is another consideration. Available floor space, ceiling height, existing structures, dock configuration, electrical infrastructure, and current equipment can all affect automation design.
Finally, the warehouse should consider the complete lifecycle of the system. Installation, controls, training, preventative maintenance, replacement parts, service, and future modifications can influence the long-term effectiveness of the investment.
Century’s capabilities span system design, mechanical and electrical installation, controls engineering, project management, automation solutions, and service. That broad scope reflects an important principle of automation in warehousing: the objective is not simply to make individual tasks automatic. It is to create a material handling environment that can reliably move products through the facility while supporting the warehouse’s operational and business requirements.
How can a company begin planning automation in warehousing with Century Conveyor Systems?
The starting point is a discussion about the facility’s current operation and its desired future state.
Century invites businesses to provide project details when beginning an automation optimization project. From there, an automation-focused approach can consider the warehouse layout, material flow, throughput requirements, equipment needs, controls, installation requirements, and ongoing support.
For organizations considering automation in warehousing, the most useful project conversations typically begin with the problem rather than a particular machine.
Instead of starting with “Which conveyor should we buy?” a business can start with questions such as: Where is our operation constrained? Which processes require excessive manual handling? Where do products accumulate? Where do errors occur? What happens when order volume increases? Which processes need to become more flexible? What capacity will the facility require in the future?
Those answers can then guide the selection of conveyors, sortation, robotics, controls, storage, palletizing, print-and-apply equipment, or other automation technologies.
Century Conveyor Systems’ role as an automation in warehousing and material handling integrator is built around that broader process—from designing and validating the system through installation, startup, service, and parts support.
For warehouses looking to modernize, the central question is therefore not simply whether automation should be added. It is how automation can be engineered around the facility’s products, processes, people, space, throughput requirements, and long-term goals. That systems-level perspective is at the heart of effective automation in warehousing.
An accumulation conveyor holds product in line without crushing it. Compare zero-pressure, minimum-pressure, MDR, and pneumatic types, and size the buffer.
More than 90% of Fortune 500 companies rely on at least one 3PL partner for fulfillment. 3PL and contract fulfillment demand is the number-one driver of new large-warehouse leasing activity in the U.S. The sector is growing — and the operators winning that growth all have something in common that has nothing to do with sales.
Winning a new 3PL contract is one thing. Building the operation behind it is another.
The 3PLs that keep customers longest are the ones with systems that can grow with them. When the customer’s volume doubles, the operation adapts. When a second customer comes into the building, the controls handle it. When the contract changes, the equipment doesn’t get ripped out.
That kind of flexibility isn’t an accident. It’s an engineering decision made before the first conveyor goes in — and it’s the difference between buying equipment and building a platform.
What Most 3PL Systems Are Not Built to Handle
Three operational pressures consistently separate the 3PLs that grow from the ones that plateau.
Speed to operational
New customer contracts come with aggressive go-live timelines. A prospective customer choosing between operators is also choosing between start dates — and a system that takes 14 months to build loses deals before the conversation starts. Fulfillment center automation only helps you win business if it can be deployed at the pace that business moves.
Multi-customer controls
This is the one that catches operators by surprise. Customer A runs one WMS. Customer B runs another. If your controls layer can only talk to one warehouse management system at a time, every new account means a custom integration project — or worse, a full rebuild. The floor should not have to choose which customer’s system drives it.
Volume that wasn’t in the original plan
A customer that signed at 5,000 orders a day is now moving 12,000. That’s the outcome every 3PL wants — and a fixed system built to the original spec can’t absorb it without a capital project. When growth requires re-engineering, growth stalls.
If any of these sound familiar, the issue isn’t the equipment you bought. It’s that it was bought as equipment, not designed as a platform.
The Platform Approach: Design for Day One, Engineer for What’s Next
We don’t start with the largest system that fits the building. We start with what the customer actually needs on day one, and design from there for what comes next. Four capabilities make that possible in a 3PL environment.
AMRs and modular conveyor
Autonomous mobile robots and modular conveyor lines can be reconfigured as customer mix, volume, and product profile change — no permanent commitment to a fixed layout. When a new account brings a different carton profile or a different pick path, the system moves with it instead of becoming the obstacle.
Put walls and shipping sortation
Fulfillment operations serve retail, DTC, and B2B out of the same building, which means mixed SKUs, mixed cartons, and mixed compliance requirements on every shift. Put walls handle order consolidation across that mix; automated shipping sortation routes finished orders to the right carrier lane without a dedicated team per channel.
WCS/WES controls that speak multiple WMS
A warehouse execution system that integrates with multiple WMS environments simultaneously is the core of multi-customer flexibility. Customer A and Customer B keep their own systems; the WES orchestrates the floor underneath both. Onboarding a new account becomes a configuration exercise, not a controls rebuild.
Rapid-deploy systems
Deployment timelines should match the pace of 3PL business. We’ve taken systems from site walk to go-live on aggressive schedules for operators who couldn’t wait 18 months for a traditional build — because in contract fulfillment, the operator who can say yes to the start date wins the contract.
The Best Time to Design for Flexibility
The best time to design a flexible system is before the first system is in the ground. The second-best time is before the next customer, the next expansion, or the next equipment replacement — because every fixed decision you make now is a constraint you’ll negotiate around later.
Century has been part of those decisions for 3PLs across the country: opening-day installations, multi-phase expansions, and platforms built around a single customer relationship that kept growing.
Planning a new 3PL facility, onboarding a new customer, or replacing equipment that wasn’t built to scale?Start the conversation — an engineering conversation, not a pitch.
Rick Maldonado leads business development for Century Conveyor Systems and works directly with operations teams on fulfillment projects across the country.
A conveyor belt cleaner can play an important role in keeping a material handling system operating efficiently, particularly in warehouses, distribution centers, fulfillment facilities, and other environments where conveyors move products continuously. When conveyor equipment is integrated into a larger automated operation, cleanliness and maintenance become part of a much bigger consideration: maintaining reliable material flow from one stage of the operation to the next.
Century Conveyor Systems specializes in conveyor and material handling automation for warehouses, distribution centers, shipping operations, and fulfillment facilities. Its approach includes system design, installation, controls, maintenance, repair, replacement parts, and ongoing support. That broader perspective is useful when evaluating equipment such as a conveyor belt cleaner because the cleaner is not an isolated component—it needs to work as part of the conveyor system and the facility around it.
The following FAQ explains what businesses should understand about conveyor belt cleaners and how the topic relates to Century Conveyor Systems’ conveyor and fulfillment solutions.
Table of Contents
What is a conveyor belt cleaner?
A conveyor belt cleaner is a device or maintenance component designed to help remove material, debris, residue, or other unwanted buildup from a conveyor belt during operation or maintenance.
The basic purpose is straightforward: a conveyor belt transports products, and material can sometimes remain on or around the belt after the product has moved onward. Without appropriate cleaning and maintenance, accumulated material can interfere with conveyor performance, contribute to wear, or create housekeeping challenges.
The specific type of cleaning equipment required depends heavily on the conveyor’s application. A conveyor handling packaged goods in a distribution center can have very different cleaning requirements from a conveyor used for bulk material or food-related applications.
This is why selecting a conveyor belt cleaner should generally begin with understanding the complete conveyor application rather than choosing a component based only on the belt itself.
Why is conveyor belt cleaning important in an automated material handling system?
Conveyor systems are often central to automated material movement. Century describes warehouse conveyor systems as the backbone of automated operations, where conveyors continuously move products through processing, sortation, and distribution activities.
That means an issue affecting one section of a conveyor can potentially affect processes farther downstream. In an automated environment, equipment is interconnected, so maintaining the conveyor is about more than keeping an individual belt visually clean.
Regular attention to conveyor cleanliness can support several operational objectives:
Maintaining consistent product movement
Reducing the accumulation of unwanted material
Supporting preventative maintenance practices
Helping protect conveyor components from unnecessary buildup
Maintaining an orderly work environment
Supporting reliable operation across connected conveyor sections
Century offers conveyor preventative maintenance as well as conveyor repair and parts services. Its maintenance approach recognizes that conveyor equipment needs ongoing care after installation, rather than being treated as a one-time capital investment.
Does Century Conveyor Systems offer a specific conveyor belt cleaner?
Century Conveyor Systems’ published website describes a broad range of conveyor systems, service capabilities, and material handling solutions. Its offerings include belt and roller conveyors, sortation conveyors, modular belt conveyors, pallet handling systems, conveyor service, preventative maintenance, repair, and replacement parts.
The company information available publicly does not identify a single product specifically branded as a “Century Conveyor Systems conveyor belt cleaner.” Therefore, businesses should not assume that the phrase refers to one standardized Century product.
Instead, a conveyor belt cleaning requirement should be evaluated within the context of the conveyor system being designed, installed, serviced, or modernized.
This distinction matters because the appropriate cleaning method can depend on factors such as belt construction, conveyed products, conveyor configuration, operating environment, production requirements, and the type of residue being removed.
How does a conveyor belt cleaner fit into Century’s broader conveyor services?
One of the important considerations when evaluating conveyor cleaning equipment is the relationship between the component and the rest of the conveyor.
Century describes itself as a full-service material handling integrator. Its services cover system design and validation, installation, startup support, controls engineering, mechanical engineering, project management, preventative maintenance, repair, and parts.
That makes maintenance part of the overall lifecycle of a conveyor system.
A conveyor belt cleaner may therefore be considered alongside other maintenance and service requirements rather than as a standalone purchase. If a facility is experiencing belt contamination, tracking problems, buildup, or recurring maintenance issues, the underlying conveyor configuration may also deserve evaluation.
A comprehensive approach can help determine whether cleaning equipment, maintenance, replacement parts, adjustments, or a larger system modification is appropriate.
What types of conveyors does Century work with?
Century’s order fulfillment information describes several conveyor configurations, including live roller and gravity conveyors, belted conveyors, modular belt conveyors, conveyor diverts, zero- and minimum-pressure accumulation conveyors, extendable conveyors, spiral conveyors, and pallet conveyors.
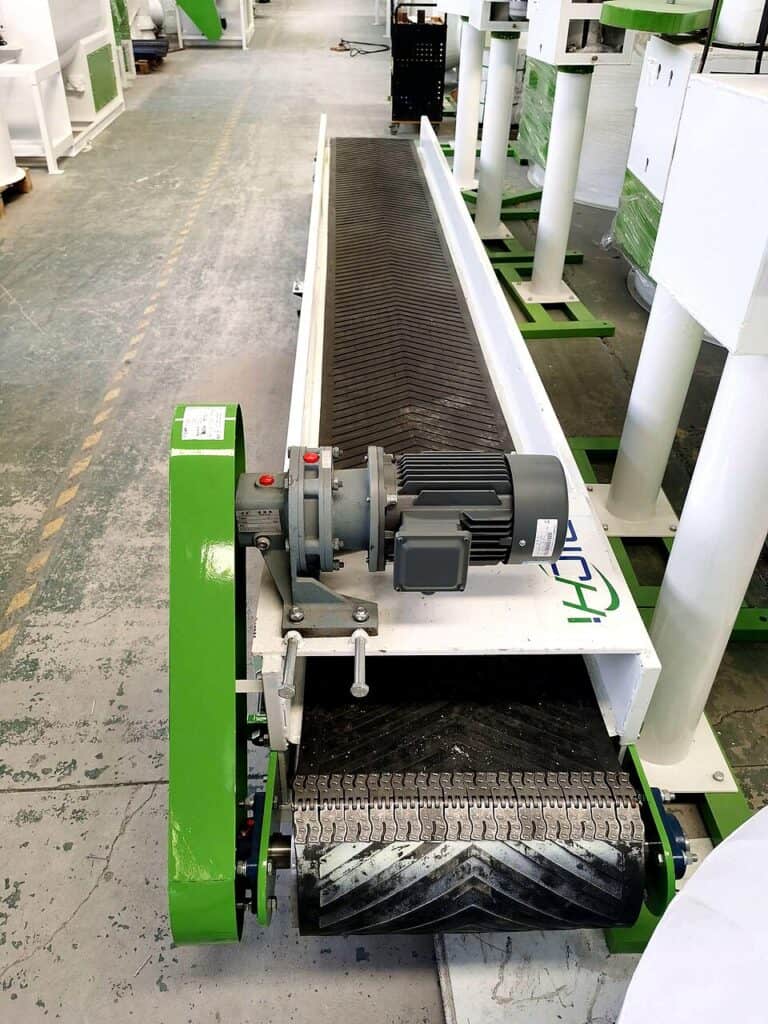
Belted conveyors are particularly relevant to a conveyor belt cleaner discussion. Century explains that belt-over conveyors use belts wrapped over the slider or rollers of a conveyor bed. These systems can provide stable conveyance for small polybags, parcels, and irregular carton sizes, while also supporting applications such as inclines, declines, and gapping.
Modular belt conveyors use individual belt sections rather than a single vulcanized rubber belt. According to Century, these modular belts can be removed, cleaned, or modified more easily and can be useful in applications requiring additional traction, tight transfers, or easier accumulation handling.
These differences demonstrate why there is no universal conveyor belt cleaning solution. The belt’s construction and the way the conveyor operates can influence what type of cleaning and maintenance approach makes sense.
Is a conveyor belt cleaner useful for fulfillment centers?
It can be, depending on the products, conveyor design, and operating environment.
Fulfillment centers place significant demands on material handling equipment because products may move through numerous stages between order receipt and shipment. Century describes order fulfillment as a process that extends from receiving an order through processing and ultimately moving the item to the shipping dock.
Conveyor systems can automate movement between these stages, reducing manual interactions and helping facilities process products efficiently.
In that environment, maintaining conveyor equipment is part of maintaining the overall material flow. A conveyor belt cleaner can be one component of a broader maintenance strategy where appropriate.
However, cleaning requirements for a fulfillment center handling cartons and polybags may differ substantially from requirements for another industry. The right solution should be based on the actual material being conveyed and the conveyor system’s operating conditions.
How should a business choose the right conveyor belt cleaner?
The first step is to define the application.
Important questions include:
What type of belt is being used? Belt construction can influence which cleaning methods are appropriate.
What products travel on the conveyor? Cartons, polybags, food products, pallets, bulk materials, and other products can create very different cleaning requirements.
What type of residue or debris needs to be removed? Dust, product fragments, packaging material, moisture, adhesive residue, and other contaminants may require different approaches.
How fast does the conveyor operate? Operating speed can influence how and when cleaning equipment can be used.
Where is the conveyor located in the process? A conveyor at an induction station may have different requirements from one positioned near packing or shipping.
How does the cleaning method affect maintenance? A solution should ideally fit into the facility’s existing maintenance program rather than create an additional source of complexity.
Century’s engineering and service capabilities can be relevant when these questions involve the conveyor system as a whole. The company provides system design, mechanical engineering, installation, preventative maintenance, repair, and parts support.
Can conveyor belt cleaning be part of preventative maintenance?
Yes. Cleaning and inspection can form part of a broader preventative maintenance program.
Preventative maintenance is intended to identify and address developing issues before they become larger operational problems. For conveyor equipment, this can involve inspecting components, identifying wear, checking alignment and tracking, addressing buildup, replacing worn parts, and maintaining equipment according to its operating requirements.
Century specifically lists conveyor preventative maintenance among its services and also provides conveyor repair and replacement parts.
A belt cleaner does not replace preventative maintenance. Instead, where appropriate, it can complement a maintenance program by helping manage material accumulation and supporting the cleanliness of the conveyor belt.
The most effective maintenance program is typically one that considers the complete conveyor rather than focusing on a single component.
Can a conveyor belt cleaner help reduce conveyor downtime?
Potentially, although the effect depends on the cause of downtime and the application.
If material buildup contributes to operational issues, keeping the belt cleaner may help address one factor contributing to those problems. But downtime can have many causes, including worn components, mechanical failures, tracking problems, electrical issues, controls problems, overloaded equipment, or inadequate maintenance.
Century’s approach covers multiple areas of conveyor support, including mechanical and electrical installation, controls engineering, preventative maintenance, repair services, and replacement parts.
This broader capability is important because simply installing a conveyor belt cleaner will not resolve every conveyor performance problem. If a facility experiences repeated downtime, the underlying cause should be identified before selecting a particular maintenance component.
What role does conveyor design play in belt cleaning?
Conveyor design can have a major effect on maintenance requirements.
Century explains that warehouse conveyor systems are engineered around the functions they need to perform. Different sections may be selected for processing, transportation, accumulation, sortation, loading, or other operational requirements.
For example, belted conveyors can provide stability for small or irregular packages, while modular belts offer a different construction and can be removed and cleaned more easily. Conveyor diverts, accumulation systems, spirals, extendables, and pallet conveyors introduce additional mechanical considerations.
Consequently, cleaning should be considered as part of the system’s design and operating requirements.
For a new facility, this means maintenance access and cleaning requirements can be considered during system planning. For an existing facility, the same principle can help identify whether a modification or modernization project would improve maintainability.
Is a conveyor belt cleaner enough to maintain a conveyor system?
No. A conveyor belt cleaner is only one potential component of a much larger maintenance strategy.
A complete conveyor maintenance program can involve routine inspections, cleaning, lubrication where applicable, component replacement, belt tracking checks, mechanical inspections, electrical inspections, controls maintenance, and prompt repair of developing problems.
Century provides conveyor service and parts support as part of its broader offering. The company states that it has an established conveyor maintenance and service department, along with replacement conveyor parts and equipment.
For facilities that depend heavily on automated material handling, this broader approach can be particularly important. A conveyor is a system of interacting mechanical, electrical, and control components, so maintenance decisions should account for those relationships.
How does conveyor maintenance support order fulfillment?
Order fulfillment depends on moving products through a series of operational steps. Century describes its fulfillment solutions as being designed to optimize output performance, reduce errors that can result in returns or product damage, and process items faster with fewer manual interactions.
Conveyors are an important part of that process because they provide continuous movement between operational areas.
Maintaining those conveyors helps facilities preserve the equipment’s intended operating conditions. Cleaning is one aspect of that maintenance, while inspections, repairs, replacement parts, controls, and system optimization address other aspects.
The goal is not simply to keep a belt clean. The larger objective is to maintain dependable material movement throughout the fulfillment operation.
When should a company contact Century Conveyor Systems about a conveyor belt cleaner?
A business should consider discussing the requirement with a conveyor specialist when cleaning becomes a recurring maintenance issue, when buildup is affecting conveyor operation, when an existing belt or conveyor is being replaced, or when a new automated material handling system is being designed.
It can also make sense to seek engineering input when a facility is experiencing repeated conveyor problems and is unsure whether cleaning, maintenance, replacement parts, modernization, or a larger system change is required.
Century provides conveyor system design as well as service, repair, preventative maintenance, parts, mechanical engineering, controls engineering, and installation. That range of capabilities allows a conveyor belt cleaning requirement to be considered within the larger material handling system.
What should businesses remember about conveyor belt cleaners?
The most important point is that a conveyor belt cleaner should be evaluated as part of the conveyor system, not as an isolated component.
Century Conveyor Systems works with multiple conveyor configurations and provides broader material handling engineering and service capabilities for warehouses, distribution centers, and fulfillment facilities. Its published solutions include belted and modular belt conveyors as well as numerous other conveyor technologies.
For an existing operation, the right cleaning approach depends on the belt, conveyed materials, operating environment, and maintenance requirements. For a new installation, cleaning and maintenance considerations can be incorporated into the system design from the beginning.
Ultimately, effective conveyor maintenance combines the right equipment with appropriate system design, inspection, preventative maintenance, repair, and parts support. A conveyor belt cleaner may be an important part of that equation, but its value is greatest when it is selected and maintained as part of a complete material handling strategy.
Modern warehouses, distribution centers, and fulfillment facilities depend on conveying systems movement to keep orders flowing. As product volumes increase and customer expectations for fast shipping continue to rise, businesses are looking beyond manual transportation methods and investing in automated conveying systems.
Century Conveyor Systems provides engineered material handling and automation solutions designed around the way products move through a facility. Rather than treating a conveyor as an isolated piece of equipment, Century approaches conveying as part of a broader operational system that can incorporate conveyors, sortation, robotics, controls, software, storage, and other automation technologies.
This FAQ explains how Century Conveyor Systems approaches conveying systems, the different technologies available, and how those technologies can support order fulfillment and warehouse operations.
Table of Contents
What are conveying systems, and how does Century Conveyor Systems approach them?
Conveying systems are material handling solutions designed to move products from one location to another within a facility. Depending on the application, they can transport cartons, totes, pallets, polybags, drums, oversized products, and other materials between different stages of an operation.
At Century Conveyor Systems, conveying systems are designed around the specific requirements of the facility rather than selected as a generic piece of equipment. The company describes its approach as turnkey system integration, meaning the project can encompass system design, validation, installation, startup, controls, automation, and ongoing service.
This distinction matters because the most appropriate conveyor depends on more than the physical product being moved. Factors such as product dimensions, weight, required speed, accumulation needs, facility layout, manual workstations, sortation requirements, and future automation plans can all influence the design.
For example, a packing area may benefit from live roller or gravity conveyors that interface effectively with manual induction. A line handling small or irregular parcels may require belted conveying for greater product stability. A high-output pallet operation may need chain-driven live roller equipment or another heavy-duty pallet conveying solution.
The objective is to create a coordinated flow through the facility instead of simply placing conveyor sections wherever space is available.
What types of conveying systems does Century Conveyor Systems provide?
Century works with several types of conveying systems, with each technology suited to different material handling requirements.
Live Roller and Gravity Conveyors
Live roller conveyors use powered rollers to move products, while gravity conveyors rely on gravity rather than a motor. According to Century, these systems can be used in areas such as packing lines, divert lines, extendable conveyor applications, and end-of-line operations.
Gravity conveying can be useful where powered transportation is unnecessary, while live roller equipment can provide controlled powered movement where the application calls for it.
Belted Conveyors
Belted conveyors provide a stable conveying surface for products that may not move effectively on rollers. Century specifically identifies belt-over applications as useful for small polybags, parcels, and irregular carton sizes.
Belted conveying can also provide advantages for inclines, declines, gapping, and applications where maintaining product stability is important.
Modular Belt Conveyors
Modular belts are constructed from individual sections rather than one continuous vulcanized belt. The modular construction can make individual sections easier to remove, clean, or modify.
Century identifies modular belt conveying as a solution for specialized handling applications, including operations requiring additional traction, tight transfers, or easier accumulation. The company also notes applications involving food handling and other specialized product flows.
Conveyor Diverts
Diverts allow products to move from one conveyor line to another without necessarily requiring a large standalone sortation system.
Depending on the application, divert mechanisms can include roller-ball systems, skate wheels, rising platforms, swinging arms, push trays, and other configurations. This gives system designers different ways to route cartons to their intended destinations.
Zero- and Minimum-Pressure Conveyors
Accumulation is an important consideration when products need to wait temporarily without disrupting the rest of a line.
Century describes zero-pressure accumulation as a configuration designed to keep products from touching one another. Minimum-pressure accumulation allows products to slow down and lightly contact each other.
These technologies can be particularly useful when products are fragile or when controlled spacing is necessary before another stage of fulfillment.
Extendable Conveyors
Extendable conveyors can telescope into and out of areas such as trailers. They can help bring the conveying point closer to the associate loading or unloading the vehicle.
Century identifies both gravity-powered and powered extendable configurations. Gravity versions can use skate wheels, while powered versions can use telescoping belts.
Spiral Conveyors
Spiral conveying systems move products vertically through a gradual curved incline. This allows a facility to connect different elevations without relying exclusively on long straight inclines or other vertical transportation methods.
For facilities where floor space is limited, vertical conveying can be an important part of the overall layout.
Pallet Conveyors
Pallet conveying systems are designed for heavier and larger loads. Century identifies several pallet-handling technologies, including pallet drag chain conveyors, pallet gravity conveyors, chain-driven live roller conveyors, and Poly-V conveyor sections.
The appropriate configuration depends on factors such as pallet characteristics, weight, throughput, staging requirements, and the desired movement pattern.
Together, these options allow conveying systems to be configured around the requirements of individual areas rather than forcing every product through the same conveyor technology.
Why are conveying systems important for order fulfillment?
Order fulfillment involves much more than transporting a package from point A to point B. Products may need to move through receiving, storage, picking, packing, labeling, sortation, and shipping before an order leaves the facility.
Century describes warehouse conveyor systems as the backbone of automated operations because they provide continuous movement between these different stages.
The value of conveying systems comes from connecting processes. When products must be manually transported between workstations, employees can spend significant amounts of time moving material instead of performing tasks that directly contribute to order processing.
An engineered conveyor system can automate much of that transportation.
For example, products can move from one processing station to another without requiring an employee to push a cart or carry individual packages across the facility. Conveyors can also be combined with accumulation, diverting, sortation, scanning, controls, and other technologies to coordinate how products move through the operation.
Century’s order fulfillment approach focuses on optimizing output, reducing errors that can contribute to returns or product damage, and processing items with fewer manual interactions.
The result is not simply a faster conveyor. It is a material flow strategy in which transportation becomes an integrated part of the fulfillment process.
How can Century’s conveying systems work with warehouse robotics?
Conveyors and robotics do not necessarily compete for the same role. In an automated fulfillment environment, they can perform complementary functions.
Century offers robotic fulfillment solutions involving automated guided vehicles (AGVs) and autonomous mobile robots (AMRs).
AGVs generally follow defined navigation methods and are suited to applications involving repeatable routes. Century notes that AGVs can transport pallets, cartons, and non-conveyable products and can be equipped with attachments that allow them to interface with the material being handled.
AMRs offer a different type of flexibility. They navigate without fixed tracks and use sensors and programming to move through a facility. This makes them suitable for applications in which products or totes need to travel through changing routes.
For example, an AMR can support goods-to-person fulfillment by retrieving totes and bringing them to packing or order fulfillment personnel.
Conveyors can provide the fixed, continuous transportation infrastructure within an operation, while robots can provide flexible transportation where fixed conveyor paths may not be practical.
This combination is particularly relevant to facilities that want automation without relying exclusively on permanently installed transportation equipment.
Can conveying systems be customized for different products and workflows?
Yes. Customization is one of the most important considerations when designing a conveying system.
A carton, polybag, pallet, drum, and irregularly shaped package can have very different conveying requirements. Even two facilities handling similar products may require different designs because their layouts, throughput requirements, labor models, storage systems, and order profiles differ.
Century’s system engineering approach accounts for these differences when designing material handling solutions.
For smaller parcels, a belted conveyor may provide the stability required to maintain consistent movement. For palletized products, heavy-duty conveying technologies may be more appropriate. In another section of the facility, gravity conveying may be sufficient for staging or manual operations.
Conveyor diverts can create routing points, accumulation sections can regulate product flow, and spiral conveyors can connect different levels.
This modular approach means the conveying system can be built around the workflow instead of forcing the workflow to conform to one conveyor type.
How do conveying systems support automation beyond transportation?
A conveyor is only one part of a modern material handling ecosystem.
Century’s broader solutions include sortation systems, robotic palletizing, controls and software, print-and-apply equipment, storage systems, and other automation technologies.
Controls can coordinate conveyor movements and equipment interactions, while warehouse management and warehouse control systems can help connect operational requirements with physical material movement.
Sortation equipment can direct products toward different destinations. Print-and-apply equipment can support labeling processes. Robotic palletizing can automate the handling of completed cases or other loads.
This interconnected approach is important because adding a conveyor does not automatically create an automated warehouse. Automation depends on how individual technologies communicate and work together.
For example, a product may enter the facility, travel through a conveyor network, be routed through a divert or sortation system, receive a label, and eventually reach a packing or shipping area. Each stage has a specific function, but the conveying system provides the physical movement that connects those processes.
What should a company consider before investing in conveying systems?
The first consideration should be the operational problem the conveying system is intended to solve.
Companies should evaluate the types of products being moved, their dimensions and weights, current and projected throughput, facility layout, accumulation requirements, manual touchpoints, destinations, and integration requirements.
It is also important to consider what the facility may look like several years after installation. A conveyor designed only around today’s volume may require substantial modification if product volumes, SKU profiles, or fulfillment processes change.
Other questions include:
Where are the largest sources of manual transportation?
Which products require special handling?
Where are bottlenecks occurring?
How much accumulation is required?
Are products fragile or irregularly shaped?
Will robotics eventually be added?
Does the system need to interface with existing controls or software?
Could the facility require additional capacity later?
What maintenance and replacement-parts support will be needed?
Answering these questions before equipment selection helps create a system based on operational requirements rather than simply selecting a conveyor based on its physical specifications.
Does Century Conveyor Systems provide support after installation?
Century’s services extend beyond system design and installation. The company states that it provides ongoing parts and service support, including conveyor repair and preventative maintenance.
This is an important consideration for facilities that depend on conveying systems as part of daily operations. Conveyor equipment can become a critical link between receiving, fulfillment, packing, and shipping, so maintenance becomes part of maintaining overall operational continuity.
Century lists services including conveyor preventative maintenance, repair and parts, mechanical and electrical installation, controls engineering, project management, and 24/7 support.
A lifecycle approach also means that the relationship does not necessarily end when a new conveyor system is started. Maintenance, replacement parts, troubleshooting, modernization, and future automation can all become part of the system’s operating life.
How can conveying systems prepare a warehouse for future automation?
A well-designed conveying system can provide a foundation for additional automation.
Century notes that automation can be added to conveyor lines and describes its robotic fulfillment solutions as scalable, allowing additional systems to be implemented as needed.
This is particularly relevant for businesses that are automating in stages. A company may initially automate transportation between a few high-volume work areas and later add robotics, sortation, automated storage, palletizing, or other technologies.
Planning for that progression from the beginning can help avoid designing a system that works only as a standalone conveyor installation.
Future-oriented conveying design can consider available space, controls architecture, connection points, throughput requirements, product changes, and potential integration with robotic equipment.
The goal is not necessarily to automate every process immediately. Instead, the conveying infrastructure can be designed as part of a broader material handling strategy that can evolve as operational requirements change.
What makes Century Conveyor Systems a systems integrator rather than simply a conveyor provider?
The distinction comes down to the scope of the solution.
Century describes itself as a full-service integrator that can combine conveyor systems with robotics, warehouse management systems, reporting software, storage, sortation, controls, and other material handling technologies.
That means the focus is on the complete workflow rather than on selling a single conveyor component.
A project can begin with system design and validation and continue through equipment integration, installation, startup, service, and maintenance. This gives businesses one broader framework for addressing the movement of materials throughout their facilities.
For an operation considering conveying systems, that approach can be useful when the material flow problem involves more than transportation alone. If bottlenecks involve picking, sortation, packing, storage, palletizing, or software coordination, the conveyor may need to be designed alongside those processes.
What is the main takeaway about Century Conveyor Systems’ conveying systems?
Conveying systems can serve as the physical foundation connecting different stages of a modern warehouse or fulfillment operation. The most effective solution depends on the products being moved, the required throughput, facility layout, accumulation needs, automation objectives, and long-term plans.
Century Conveyor Systems approaches conveying as part of a larger material handling system. Its solutions encompass technologies ranging from belt, roller, gravity, modular, spiral, extendable, divert, and pallet conveyors to robotics, sortation, controls, software, and ongoing service.
For businesses evaluating conveying systems, the central question is therefore not simply which conveyor to purchase. It is how material should move through the facility today, how that movement can be automated, and how the system can support the operation as requirements evolve.
By engineering conveying around the broader workflow, businesses can create a material handling environment in which transportation, automation, and fulfillment processes operate as connected parts of the same system.
Hardware distributors, fastener companies, and industrial supply operations carry tens of thousands of SKUs. Fifty thousand is common. Sixty thousand isn’t unusual. Every one of those items needs accurate storage, retrieval, and labeling — and in most of these buildings, a person is still walking to a bin to pick it by hand.
Here’s the strange part: these are probably the most automation-ready companies that haven’t automated yet. The operational profile is almost perfectly matched to proven technology. It’s not that automation doesn’t work for high-mix distribution. It’s that nobody has shown these operations a system that fits how they actually work today and where they’re going next.
This article lays out what that profile looks like, the four pressure points that eventually force the automation decision, and which picking methods actually fit a high-SKU operation.
The High-Mix Profile: Why These Operations Are Built for Automation
The characteristics of hardware and fastener distribution are unmistakable:
Extremely high SKU counts — 50,000+, with a long tail of slow movers
Small items stored in bins or drawers
Piece-picking across multiple zones
Mixed carton sizes going to retail stores and e-commerce orders out of the same building
Constant pressure on inventory accuracy
Every one of those characteristics has a proven automation answer. Yet the typical pick error rate in a manual high-SKU environment runs 2 to 5 percent. At 50,000 SKUs and real order volume, that’s tens of thousands of incorrect orders a year — each one generating a return, a re-ship, a replenishment error, or an unhappy retail account.
Meanwhile, goods-to-person automation typically delivers a 60%+ reduction in labor per pick in exactly these environments. The math has been working for years. What’s usually missing is a design that starts from the operation’s actual inventory profile instead of a product brochure.
The Four Pressure Points That Drive the Automation Decision
In our work with high-mix distributors, the decision to automate almost never comes from a single failure. It comes from four pressures compounding until the status quo costs more than the system that would fix it.
1. Inventory accuracy
When you carry 60,000 SKUs and pick by hand, small errors compound. A bin that’s off by ten pieces creates downstream problems in customer orders, replenishment, and returns processing — and nobody catches it until a customer does. Goods-to-person picking eliminates most of that at the source, because the system tracks every retrieval and presentation instead of relying on a picker’s count.
2. Labor spent on low-velocity SKUs
High-SKU operations have a long tail of items that move slowly. Keeping a picker walking to those locations all day is one of the most inefficient things a warehouse can do — you’re paying travel time for items that might get picked twice a week. Zone-based carton flow for fast movers and goods-to-person for the long tail both attack this directly.
3. Mixed carton and order profiles
Retail replenishment, e-commerce, and contractor orders all move through the same building with different carton sizes and different compliance requirements. Handled manually, that means dedicated teams per channel or constant channel-switching. Shipping sortation driven by a warehouse control system makes it manageable in one flow.
4. Replenishment timing
In a high-SKU pick environment, keeping bins stocked without disrupting active picking is a logistics problem in its own right. WCS-controlled replenishment logic handles it automatically — no second team working around the first, no stockouts discovered mid-wave.
If two or more of these are recurring conversations in your operation, the picking method is the underlying issue — not the people running it.
Warehouse Picking Methods That Fit High-SKU Operations
The right system for a 60,000-SKU hardware distributor looks different from the right system for a 5,000-SKU consumer goods operation. Order picking methods aren’t interchangeable — they’re matched to inventory profile, order mix, and throughput. Four capabilities matter most in high-SKU environments.
Goods-to-person picking
AMR-driven storage and retrieval that brings inventory to the picker instead of sending the picker to inventory. Floor travel — the largest single component of manual pick labor — drops dramatically, and pick accuracy rises because the system presents exactly one location at a time. For the long tail of slow-moving SKUs that defines high-mix distribution, goods-to-person automation is usually the highest-leverage move available.
Carton-flow pick modules with zone picking
For high-velocity SKUs, zone-based pick modules with carton flow rack shelving concentrate thousands of facings into a compact footprint. Pick-to-light guidance takes the search out of each pick, and tote conveyor integration does the horizontal travel between zones. Critically, this handles the density of a hardware or fastener operation without requiring a complete facility rebuild.
Shipping sortation and WCS controls
Controls-driven sortation routes completed orders to the correct carrier lane, pack station, or staging area automatically. The warehouse control system underneath handles replenishment logic, wave management, and real-time visibility across every zone — the connective tissue that lets retail, e-commerce, and contractor orders share one building without sharing each other’s problems.
Scan, label, and verify
Scan tunnels, dimensioning, and print-and-apply labeling built into the outbound line. For operations serving retail accounts with compliance labeling requirements, this is not optional — and it cannot be an afterthought bolted on after the system is designed. Chargebacks are how retail partners tell you your labeling process needs work.
How to Know It’s Time
Some practical diagnostics for a high-SKU operation still picking manually:
Your SKU count has grown significantly since your current pick setup was designed
Inventory accuracy is a recurring issue that never quite gets resolved
Pickers spend a visible share of the day walking to slow-moving locations
Peak requires temp labor just to hold your normal error rate
Retail compliance chargebacks are trending the wrong direction
Replenishment regularly interrupts active picking
None of these fix themselves at higher volume. They scale with it.
Start With a Site Walk
If your operation carries more SKUs than your current picking system was designed for, the conversation is worth having. A site walk takes an hour. The analysis that comes out of it usually pays for itself before a system is even specified — because it tells you which picking method fits your actual inventory profile, which parts of your operation should stay exactly as they are, and where the practical upgrade path runs.
Ready to look at your operation?Schedule a site walk — no pitch, just an engineering conversation about how your building actually works.
Rick Maldonado works with distribution operations across the country on automation projects ranging from single-zone retrofits to full facility designs.
Warehouse operations are under constant pressure to move to automated solutions, fulfill orders faster, control operating costs, and maintain accuracy as customer expectations continue to rise. For distribution centers and fulfillment facilities, automated solutions can provide a way to improve material flow while reducing dependence on repetitive manual handling.
Century Conveyor Systems specializes in automated material handling and turnkey system integration for warehouses, distribution centers, shipping operations, and fulfillment facilities. Its approach brings together conveyor systems, robotic fulfillment, robotic palletizing, controls and software, sortation, storage systems, print-and-apply equipment, and ongoing service capabilities.
The following FAQ explains what makes Century Conveyor Systems’ automated solutions different and how the company’s approach can address several common warehouse and distribution challenges.
Table of Contents
What are Century Conveyor Systems’ automated solutions?
Century Conveyor Systems’ automated solutions are engineered material handling systems designed to improve how products, cartons, totes, pallets, and other items move through a warehouse or distribution facility.
Rather than treating automation as a single piece of equipment, Century approaches it as an integrated system. Depending on the requirements of a facility, that system can include conveyor equipment, robotic technologies, sortation, pallet handling, warehouse controls, software, storage systems, and other material handling technologies.
This matters because warehouse automation works best when individual components operate as part of a coordinated process. A conveyor may transport an item, for example, while a control system determines where it needs to go and a sortation device directs it to the appropriate destination.
Century’s role as a system integrator means the company can work across these different technologies and manage the project from system design and validation through installation, startup support, parts, and service.
Why would a warehouse need automated solutions?
The biggest reason is that growing operational demands can eventually exceed what manual processes can efficiently handle.
A facility may be dealing with increasing order volumes, longer travel distances, labor-intensive picking, repetitive pallet movement, congested work areas, or a growing need to process products consistently throughout the day. Simply adding more manual labor does not necessarily solve those problems.
Automation can instead change the way work moves through the facility.
Century’s order fulfillment approach focuses on optimizing warehouse touchpoints to improve output, reduce errors that can lead to returns or damaged products, and process items more quickly with fewer manual interactions.
That makes automated solutions particularly relevant for organizations looking beyond short-term labor adjustments and toward a more scalable material handling strategy.
How do conveyor systems fit into Century’s automated solutions?
Conveyors are one of the foundational technologies in a warehouse automation system because they provide a consistent method for moving products between operational areas.
Century offers several conveyor configurations, including live roller, gravity, belted, modular belt, pallet, spiral, and other specialized conveyor applications. The appropriate technology depends on factors such as the product being handled, desired throughput, available floor space, accumulation requirements, and the way different workstations interact.
For example, belted conveyors can provide stable transportation for small polybags, parcels, and irregular cartons. Gravity and live roller conveyors can be useful in areas that need to interface with manual induction or packing processes. Spiral conveyors can move products between levels while conserving valuable floor space.
The key advantage is not simply having a conveyor. It is having the right conveyor configuration integrated into the overall material flow.
Can automated solutions reduce manual material handling?
Yes. Reducing unnecessary manual transportation is one of the central opportunities provided by warehouse automation.
In a traditional facility, employees may spend substantial portions of their shifts walking, transporting cartons, moving pallets, retrieving inventory, or carrying products between process steps. These activities consume time without necessarily adding value to the product itself.
Century’s automated solutions can shift some of that transportation work to conveyors, automated guided vehicles, autonomous mobile robots, and other equipment.
The result can be a workflow in which employees spend more time performing tasks that require human judgment or interaction while automated equipment handles repetitive transportation.
This is particularly relevant to goods-to-person operations, where automation can bring inventory or totes to workers rather than requiring workers to repeatedly travel to retrieve products.
What role do robots play in Century’s automated solutions?
Robotics provide another layer of flexibility beyond fixed conveyor infrastructure.
Century identifies two major categories of warehouse robots: automated guided vehicles (AGVs) and autonomous mobile robots (AMRs).
AGVs can be used to transport pallets, cartons, or other loads along defined routes. Depending on the application, they can use technologies such as magnetic tape, QR codes, inductive wires, or laser-based navigation.
AMRs operate differently. They are trackless and use sensors and programming to navigate through a facility. This allows them to move more freely and makes them particularly useful for applications where transportation paths may need to be flexible.
For example, AMRs can transport totes or carts through a distribution facility and can support goods-to-person workflows by retrieving inventory and delivering it to packing or fulfillment personnel.
The important distinction is that robotics do not necessarily replace conveyor automation. In many facilities, robots and conveyors can complement one another.
Are Century’s automated solutions scalable?
Scalability is one of the most important considerations when investing in warehouse automation.
A company may know that its order volume will increase but may not know exactly how quickly that growth will occur. Installing a system designed only for today’s workload can create limitations later, while investing too heavily in capacity too early can create unnecessary costs.
Century highlights scalability as a benefit of its robotic fulfillment solutions. Additional robotic systems can be implemented as operational requirements change, allowing an organization to expand its automation strategy over time.
This can be particularly useful for businesses experiencing seasonal demand, expanding product lines, entering new markets, or increasing fulfillment volumes.
A scalable approach also encourages companies to think beyond a single automation project. Instead, the initial system can become the foundation for future improvements.
How can automated solutions improve order fulfillment?
Order fulfillment involves a chain of activities that begins when an order is received and continues until the completed shipment reaches the shipping dock.
Every handoff represents an opportunity for delay, damage, misrouting, or unnecessary labor.
Century’s fulfillment systems are designed to address the flow between these stages. Conveyors can transport cartons and other products, accumulation systems can manage spacing, diverts can route products toward different destinations, and robotic systems can automate transportation within the facility.
Sortation can further separate products according to their destination or processing requirements.
When these technologies are properly coordinated, the facility can create a more predictable flow of materials instead of relying on employees to manually coordinate every movement.
That consistency is one of the major reasons automated solutions can have an impact beyond simple transportation speed.
Can automation help reduce product damage and fulfillment errors?
Automation can contribute to greater consistency in product handling, which can help address certain causes of damage and fulfillment errors.
Century specifically emphasizes reducing errors that can result in returns or item breakage as part of its order fulfillment strategy.
One example is zero-pressure accumulation. These conveyor systems use sensors and other equipment to create controlled spacing between products so that items do not collide with one another. This can be especially useful when handling fragile products.
Automated diverts and sortation systems can also help direct products to the appropriate lines or destinations without requiring every carton to be manually redirected.
Automation does not eliminate every possible source of error, but designing the material flow around controlled, repeatable processes can reduce the number of manual interactions where mistakes may occur.
What makes Century’s approach different from simply buying automation equipment?
The difference is system integration.
A warehouse can purchase individual conveyors, robots, controls, or storage products from different suppliers, but those components still need to work together as a functional system.
Century positions itself as a full-service integrator rather than simply an equipment provider. Its process includes system design, validation, implementation, installation, startup support, and ongoing parts and service.
That integrated approach is important because the success of an automation project depends on more than the specifications of individual machines.
The equipment needs to fit the physical facility, the products being handled, the required throughput, the workforce, the operational processes, and the software and controls governing the system.
In other words, effective automated solutions are designed around the operation rather than added to it as disconnected equipment.
Can Century automated solutions work with existing warehouse infrastructure?
They can be designed around a facility’s existing requirements, and automation does not necessarily mean replacing every component already in operation.
Century offers retrofit and modernization capabilities in addition to new automation systems. This is significant for organizations that already have conveyor equipment or other material handling infrastructure but need greater capacity, improved controls, updated technology, or additional automation.
A modernization strategy can allow a company to address specific limitations rather than starting from scratch.
For example, an existing conveyor line might be supplemented with new controls, sortation, robotic transportation, or other equipment. The right approach depends on the condition of the current system and the organization’s operational goals.
This flexibility can make automated solutions relevant to both new facilities and established warehouses.
What types of products can Century’s automated solutions handle?
The company’s solutions are designed for a broad range of material handling applications. Century states that it can engineer systems for items that go into boxes, pallets, totes, drums, or polybags.
That breadth matters because different products create different engineering requirements.
Small parcels may require stable belted conveyance. Heavy pallets may require specialized pallet conveyor equipment. Fragile products may benefit from controlled accumulation. Irregular products may need a different handling method than standardized cartons.
Rather than applying one automation technology to every product, the system can be designed around the characteristics of the items moving through the facility.
This product-specific approach is an important consideration when evaluating automated solutions.
How do controls and software contribute to automation?
Physical equipment is only part of a modern automated material handling system. Controls and software help coordinate what the equipment actually does.
Century provides capabilities involving control panels, programmable logic controls, warehouse management systems, and warehouse control systems.
These technologies can help connect the movement of physical products with the information required to manage that movement.
For example, a conveyor system needs to know when products should move, stop, accumulate, divert, or proceed to another processing area. Coordinating those actions requires controls and programming.
The result is a system in which equipment and operational information work together rather than existing as isolated components.
Are automated solutions only appropriate for large distribution centers?
No. The appropriate level of automation depends on the operation rather than simply the size of the building.
A large distribution center may benefit from extensive conveyor networks, sophisticated sortation, robotic fulfillment, pallet automation, and integrated software. A smaller operation may benefit from targeted automation addressing its biggest bottleneck.
The principle is to identify where automation can provide the greatest operational improvement.
For some facilities, that might mean automating carton transportation. For others, robotic fulfillment could be more valuable. Another operation may need better pallet movement, sortation, storage, or controls.
Century’s range of solutions allows automation to be considered as a collection of technologies that can be configured around the specific needs of the facility.
What should a company consider before investing in automated solutions?
A company should begin with the operational problem rather than the technology.
Important questions include:
What products need to be handled?
How much volume moves through the facility?
What is the current and expected future throughput?
Where are the biggest bottlenecks?
How much manual transportation is currently required?
Which processes generate the most errors or product damage?
How much floor space is available?
Which existing systems can be retained or modernized?
How much scalability will be required in the future?
How should the automated system interact with warehouse management and control software?
These questions help determine whether conveyors, robotics, sortation, pallet handling, storage systems, controls, or a combination of technologies make the most sense.
The goal should not be to automate everything simply because automation is available. The goal should be to create a material handling system that solves measurable operational problems.
How can a company get started with Century Conveyor Systems?
The first step is to discuss the facility, its current processes, and its automation objectives with Century.
A project can be evaluated based on the specific products being handled, throughput requirements, facility layout, existing equipment, labor considerations, and future growth.
From there, an automation strategy can be developed around the operational requirements.
For companies considering automated solutions, this approach can be more valuable than choosing equipment first and attempting to make the operation fit afterward. The right system starts with understanding how materials move through the facility and identifying where technology can make that movement faster, more consistent, and more efficient.
What is the biggest advantage of Century’s automated solutions?
Ultimately, the biggest advantage is the ability to combine multiple automation technologies into a coordinated material handling strategy.
Conveyors can provide continuous product movement. Sortation can direct products to their destinations. Robotics can provide flexible transportation. Palletizing equipment can automate demanding end-of-line tasks. Controls and software can coordinate equipment and information. Storage systems can improve how inventory is organized and accessed.
Individually, each technology addresses a specific problem. Together, they can create a more connected fulfillment operation.
That is the central idea behind Century Conveyor Systems’ automated solutions: automation should not be viewed simply as a collection of machines. It should be engineered as an integrated system designed around the way a warehouse actually operates.
For distribution centers and fulfillment facilities looking to increase throughput, reduce unnecessary manual handling, improve consistency, and prepare for future growth, a carefully engineered automation strategy can provide a foundation for long-term operational efficiency.
Material handlers are at the heart of an efficient warehouse or distribution operation. Every carton, pallet, tote, package, and other product must move through a facility reliably and efficiently before it reaches its final destination. A material handler plays an important role in that process, but modern material handling increasingly involves more than manual movement. Conveyor systems, automated guided vehicles, autonomous mobile robots, sortation equipment, and other technologies can work together to create a faster and more reliable material flow.
Century Conveyor Systems helps businesses develop material handling and order fulfillment solutions designed around the specific requirements of their facilities. Rather than treating every warehouse the same, Century can engineer systems around factors such as product type, throughput, available space, handling requirements, and the amount of automation desired.
The following FAQ explains what a material handler means in a modern distribution environment and how Century Conveyor Systems approaches material handling as part of a larger automated fulfillment strategy.
Table of Contents
What is a material handler?
A material handler is a person, machine, or automated system responsible for moving, positioning, transporting, or otherwise managing products and materials within a facility.
Traditionally, material handlers have included warehouse employees who move cartons, pallets, totes, and other products between receiving, storage, picking, packing, and shipping areas. However, modern warehouses increasingly use automated equipment to perform many of these same transportation functions.
For Century Conveyor Systems, material handling can encompass a much broader system of technologies. Conveyor equipment can continuously move products between operational areas, while robotic solutions such as automated guided vehicles (AGVs) and autonomous mobile robots (AMRs) can transport products without requiring every movement to be performed manually.
This distinction is important because a material handler does not necessarily have to be a person. In an automated warehouse, the material-handling function can be distributed across conveyors, robots, controls, sortation equipment, and employees working together.
How does Century Conveyor Systems approach material handling?
Century approaches material handling as part of the overall flow of a warehouse rather than as an isolated transportation task.
The objective is to understand how products move through a facility from the point they enter the operation through processing and ultimately to shipping. An effective material-handling solution should help reduce unnecessary movement, improve throughput, minimize handling errors, and support consistent order fulfillment.
This can involve combining multiple technologies rather than relying on a single piece of equipment. For example, conveyors may provide continuous transportation between workstations, while robotic equipment handles flexible movements that would be difficult or inefficient to accomplish with fixed conveyor infrastructure.
Century’s capabilities include conveyor systems, robotic fulfillment, controls engineering, mechanical engineering, project management, installation, maintenance, modernization, and other services that can support a complete automation project.
The result is a material-handling strategy designed around the operation instead of simply adding equipment to an existing floor plan.
What types of conveyor systems can support a material handler?
Different products require different methods of transportation, so there is no universal conveyor configuration for every material handler or warehouse.
Century works with several conveyor technologies, including live roller and gravity conveyors, belted conveyors, modular belt conveyors, conveyor diverts, accumulation conveyors, extendable conveyors, spiral conveyors, and pallet conveyor systems.
Live roller conveyors, for example, can be useful in packing lines, divert applications, and other areas where powered movement is needed. Gravity conveyors can provide a simpler approach where powered transportation is unnecessary.
Belted conveyors can provide stable transportation for small packages, polybags, irregular cartons, and other products that may not move as reliably on rollers. Modular belt systems offer additional flexibility because individual belt sections can be removed, cleaned, or modified.
For palletized materials and heavier loads, specialized pallet conveyor systems can provide the stability and durability needed for the application.
The important consideration is matching the conveyor technology to the material being handled, the required throughput, and the movement that needs to occur.
Can a material handler system reduce manual interactions?
Yes. One of the major objectives of warehouse automation is to reduce unnecessary manual interactions with products.
Manual handling can require employees to repeatedly walk, lift, carry, transfer, and reposition products. As order volumes increase, these repetitive movements can become a significant part of the fulfillment process.
A properly engineered material-handling system can automate many transportation steps. Conveyors can move products continuously between designated areas, while robotic systems can transport totes, cartons, pallets, or carts throughout a facility.
Reducing manual transportation does not necessarily mean eliminating employees. Instead, it can allow employees to spend more time performing tasks that require judgment, exception handling, customer-specific processing, or other activities that are difficult to automate.
Century’s order fulfillment approach focuses on processing items faster with fewer manual interactions while also working to reduce errors and product damage.
How can material handling affect order fulfillment?
Material handling has a direct effect on how quickly and consistently orders move through a warehouse.
An order fulfillment process includes numerous individual steps, from receiving an order and retrieving the appropriate products to packing and moving completed orders toward the shipping area. Delays in one part of that process can affect everything downstream.
A material-handling system can connect these stages so products move efficiently from one process to another.
For example, conveyors can transport cartons from picking areas toward packing stations. Diverts can direct products onto different lines based on their destination or processing requirements. Accumulation conveyors can help manage spacing between products. Extendable conveyors can assist with loading activities by bringing transportation equipment directly into a trailer.
When these technologies are designed as part of one coordinated system, material movement becomes an integrated component of fulfillment rather than a series of disconnected manual tasks.
Why is product stability important for a material handler?
A material handler must account for the physical characteristics of the products being transported.
Small packages, polybags, irregular cartons, fragile products, heavy pallets, and oversized loads can all behave differently while moving through a warehouse. A conveyor that works well for one product may not be appropriate for another.
Belted conveyor systems can provide greater stability for certain small or irregular products. Accumulation systems can also be configured to control how products interact with one another.
Zero-pressure accumulation is particularly useful when products should not touch during accumulation. Minimum-pressure accumulation, meanwhile, allows products to slow down and make light contact.
These distinctions can help protect products from unnecessary collisions and damage while also keeping material moving efficiently through the operation.
Can a material handler system handle pallets as well as cartons?
Yes. Material-handling systems can be designed for a wide range of load types, including individual cartons and palletized products.
Pallet handling requires equipment capable of supporting substantially heavier and larger loads than many traditional carton conveyors. Century offers several pallet conveyor approaches, including pallet drag chain, pallet gravity, chain-driven live roller, and Poly-V conveyor sections.
The appropriate technology depends on factors such as pallet weight, load characteristics, required throughput, and whether pallets need to be accumulated, staged, transported, or transferred between processes.
For high-output pallet operations, powered live roller systems can provide the ability to move multiple pallets through an operation. Other configurations can be used for staging or end-of-line accumulation.
This makes material handling adaptable to facilities that manage both individual packages and larger unit loads.
How do robots function as material handlers?
Robots can perform many of the transportation tasks traditionally associated with a human material handler or lift truck.
Century’s robotic fulfillment solutions include automated guided vehicles and autonomous mobile robots.
An AGV typically follows a defined navigation method, such as magnetic tape, QR codes, inductive wires, or laser-based systems. This makes AGVs well suited to applications involving predictable routes and transportation of pallets, cartons, or other loads.
AMRs take a more flexible approach. Rather than following a fixed track, they use sensors and onboard programming to navigate through a facility. This allows them to move totes, cartons, or carts through changing routes.
For goods-to-person operations, AMRs can retrieve inventory containers and bring them to packing or fulfillment personnel. This can reduce the amount of walking required from employees while maintaining flexibility as operational requirements change.
Is a material handler solution scalable?
Scalability is one of the most important considerations when investing in warehouse automation.
A system that works for today’s order volume may not be sufficient if a business expands, adds new product lines, opens additional sales channels, or experiences seasonal increases in demand.
Century’s robotic fulfillment approach emphasizes scalability, particularly because additional robotic units can potentially be implemented as requirements grow. This can provide a different path to expansion compared with systems that require extensive permanent infrastructure.
Conveyor systems can also be designed with future automation opportunities in mind. Additional technologies can potentially be incorporated into a conveyor line as operational requirements change.
The goal is not simply to automate today’s workload. A well-planned material-handling strategy should give a facility room to evolve.
What makes Century Conveyor Systems different from simply buying material-handling equipment?
Equipment is only one component of an effective material-handling solution.
The challenge is determining how different pieces of equipment should work together within the facility. Conveyor selection, product characteristics, controls, layout, throughput requirements, installation, maintenance, and future expansion can all influence the success of an automation project.
Century Conveyor Systems provides engineering and implementation capabilities that span multiple parts of the project. Its services include concepts and design, controls engineering, control panel design and fabrication, mechanical engineering, electrical and mechanical installation, project management, preventative maintenance, repairs, and modernization.
That broader approach can be particularly valuable when a business needs more than an individual conveyor or robot. Instead of viewing a material handler as a standalone piece of equipment, Century can approach material movement as part of the facility’s complete fulfillment architecture.
When should a company consider automating its material handling?
Automation may be worth considering when manual transportation is becoming a constraint on productivity, accuracy, capacity, or consistency.
Signs can include employees spending excessive time walking between work areas, increasing order volumes, repetitive transportation tasks, product damage caused by unnecessary handling, difficulty maintaining throughput during peak periods, or a need to improve the consistency of fulfillment operations.
Automation can also make sense when a facility needs to use its available space more effectively. Technologies such as spiral conveyors can move products between levels while occupying less floor space than some alternative configurations.
The right decision depends on the facility and its operational goals. A material-handling assessment should consider current processes as well as anticipated future requirements.
What should a company consider when selecting a material handler solution?
The most important consideration is that the solution should match the operation.
Companies should evaluate what products need to be moved, how much those products weigh, how frequently they need to move, where they need to go, how quickly they need to get there, and how much human interaction is appropriate.
Throughput is another critical consideration. A system designed for low-volume operations may not perform effectively in a high-output distribution environment.
Facility layout also matters. Available floor space, building height, existing equipment, workstations, loading areas, and traffic patterns can all affect the design.
Finally, companies should consider maintenance and future expansion. A material-handling system is a long-term investment, so reliability, serviceability, and the ability to adapt can be just as important as initial performance.
Can Century Conveyor Systems help modernize an existing material-handling operation?
Yes. Material-handling automation does not necessarily require building an entirely new facility.
Existing conveyor systems and other equipment can sometimes be upgraded, expanded, or integrated with newer technologies. Modernization can be particularly useful when an existing operation is functional but no longer provides the speed, flexibility, or control required by current business demands.
Century offers retrofit and modernization capabilities as part of its broader automation services.
This approach can allow a business to improve an existing material-handling infrastructure rather than treating every automation project as a complete replacement.
What is the main benefit of working with Century on material handling?
The central benefit is the ability to approach material movement as an integrated part of warehouse performance.
A material handler should do more than move an item from one location to another. The overall system should help products move through the facility efficiently, safely, consistently, and with as little unnecessary handling as practical.
Century Conveyor Systems combines conveyor technologies, robotic fulfillment solutions, engineering, controls, installation, service, and modernization to address those requirements.
For companies looking to improve order fulfillment, the material handler is therefore not just an employee, conveyor, or robot. It is part of a larger system designed to connect the different stages of warehouse operations.
How can a company get started with a Century Conveyor Systems material-handling project?
The first step is to evaluate the existing operation and identify where material movement creates bottlenecks, unnecessary manual work, delays, errors, or capacity limitations.
From there, a material-handling strategy can be developed around the facility’s specific products, processes, throughput requirements, available space, and future goals.
Century Conveyor Systems can engineer solutions involving conveyor systems, robotic order fulfillment, controls, and related automation technologies. The company also provides project management, installation, service, and modernization capabilities to support implementation beyond the initial system design.
Ultimately, the best material handler solution is one that fits the way a facility actually operates. By combining the appropriate transportation technology with thoughtful engineering and automation planning, businesses can create a more efficient path from receiving and processing through fulfillment and shipping.