
How a vertical lift module works, what it stores well, how it compares with carousels and shelving, and how a VLM connects to conveyor and your WMS.
Continue reading
How a vertical lift module works, what it stores well, how it compares with carousels and shelving, and how a VLM connects to conveyor and your WMS.
Continue reading
Pallet racking types compared: selective, double-deep, drive-in, push-back, pallet flow, and more, with how to match rack to your inventory and your building.
Continue reading
In material handling there’s no slow season. Here’s why we asked our customers where they want to hear from us, and what we’re doing with the answer.
Continue reading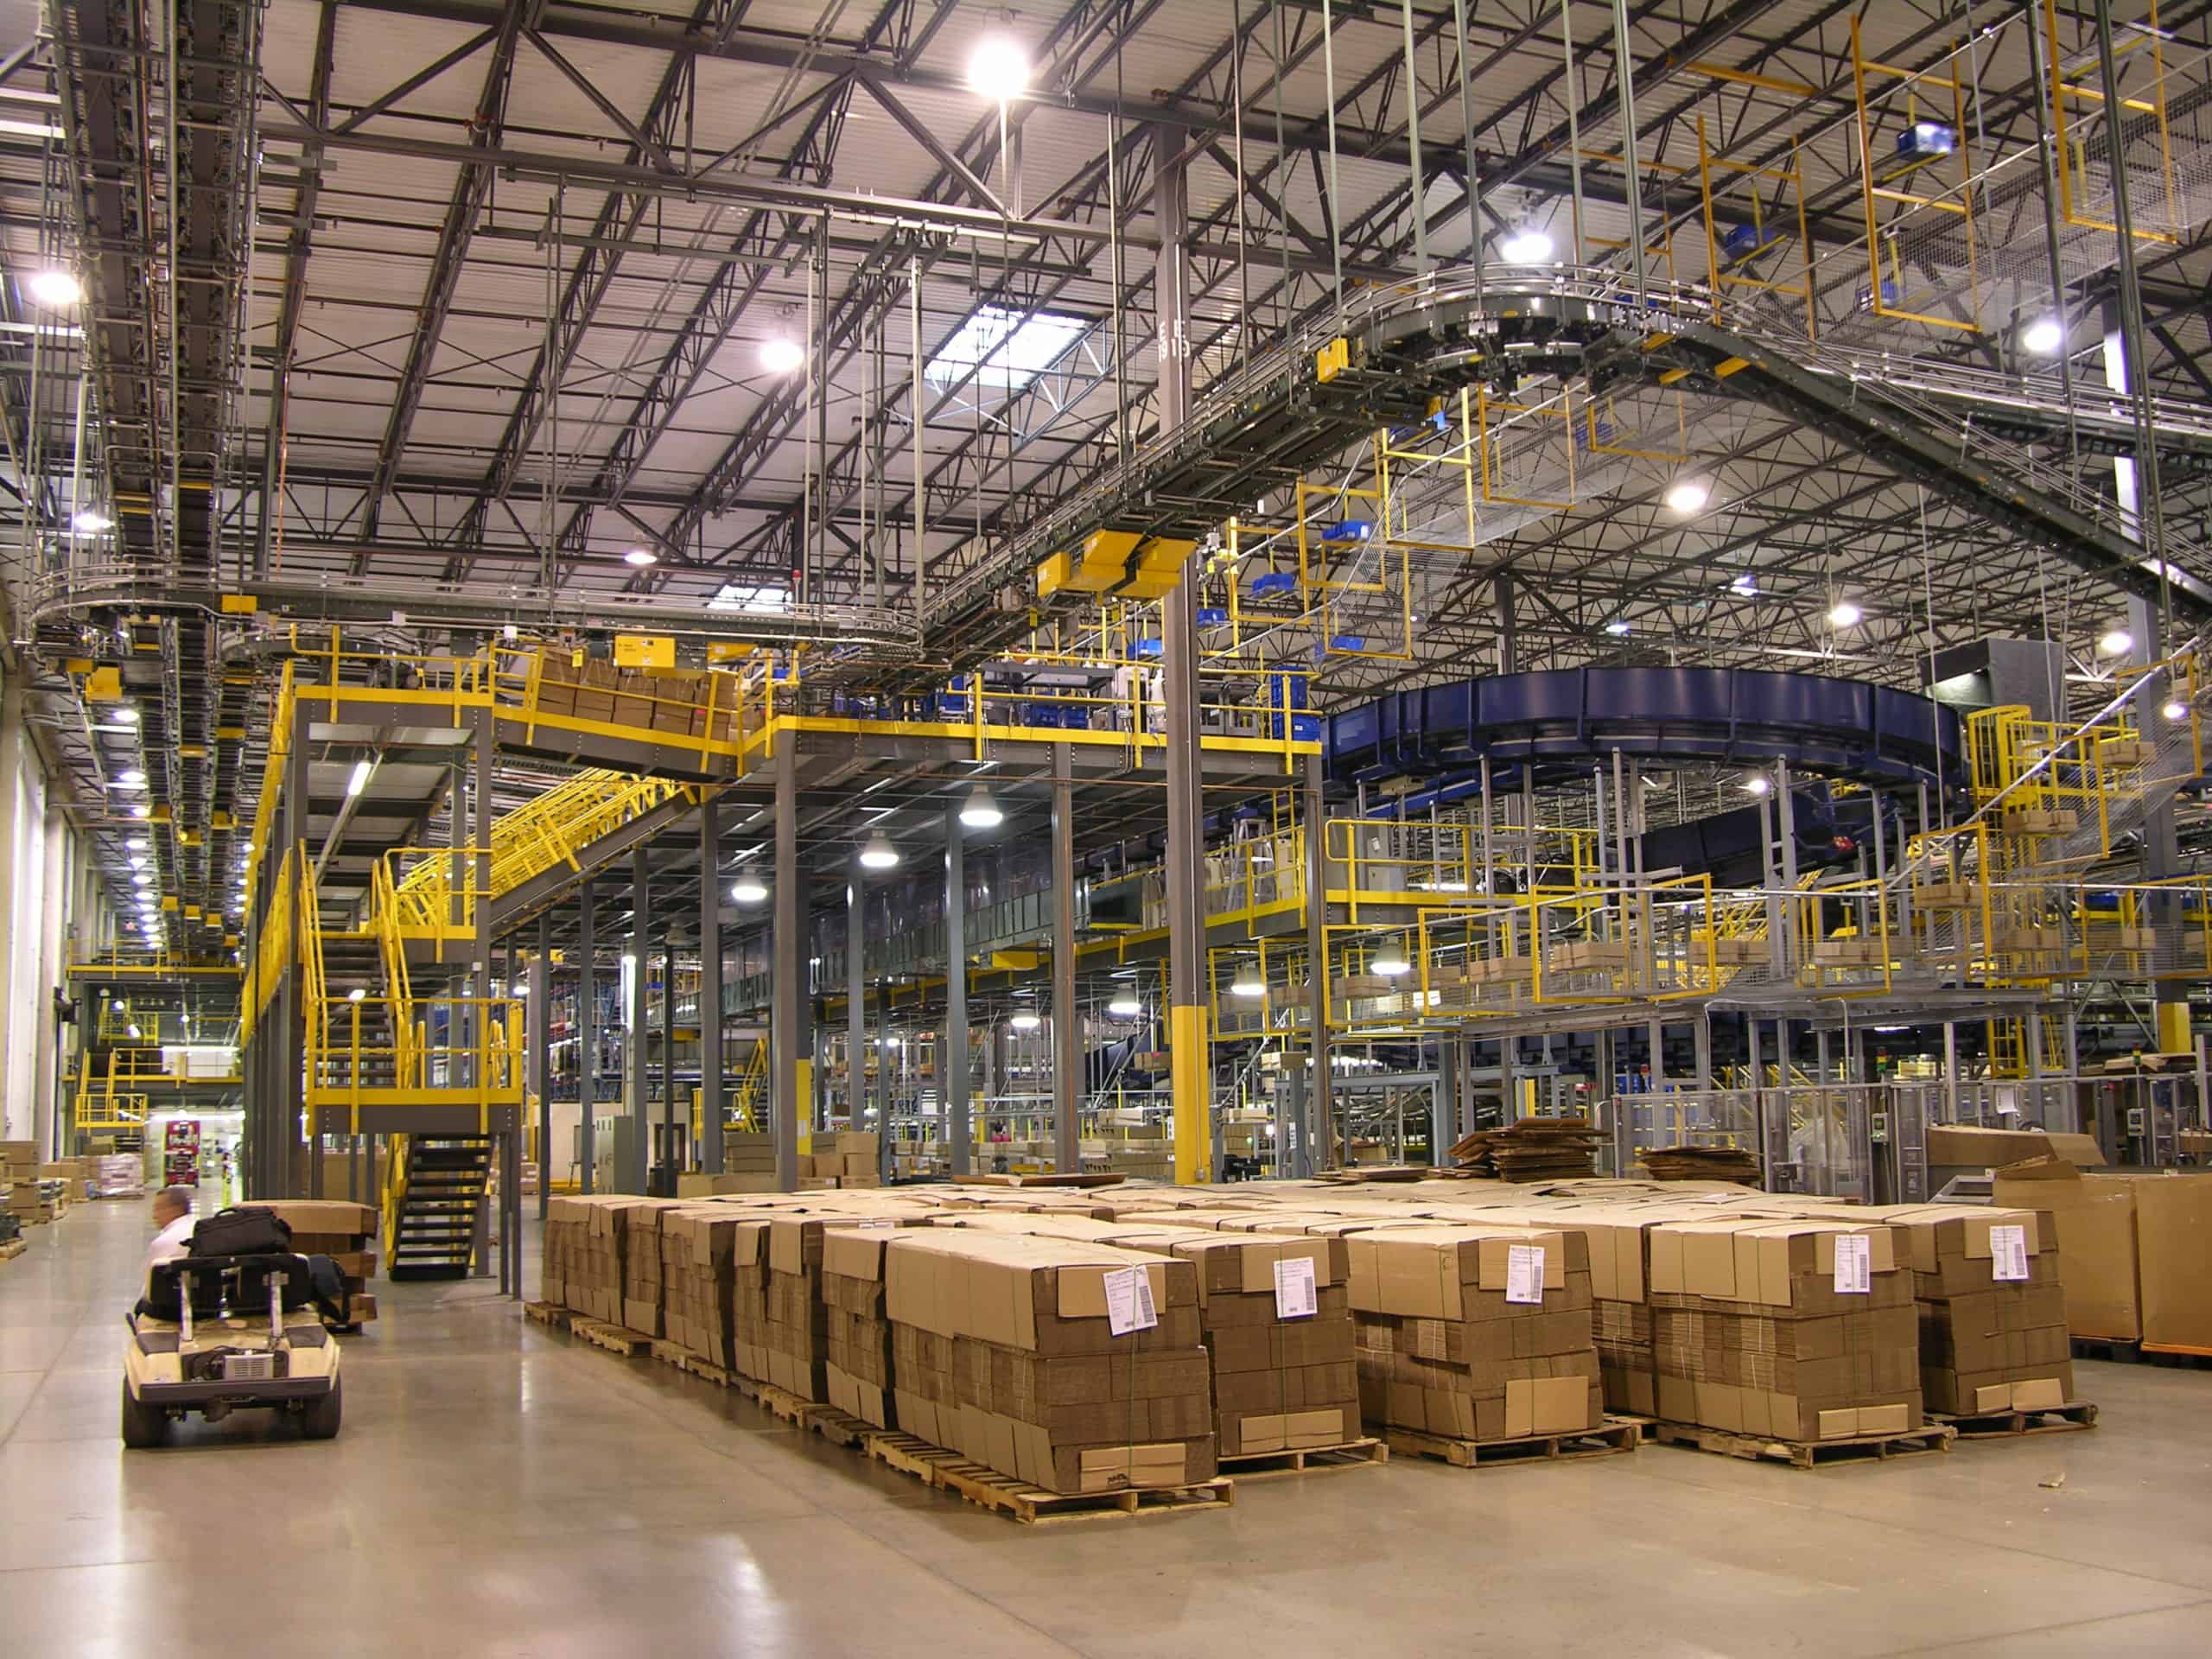
Century Conveyor is part of a five-company network covering controls, integration, robotics, fabrication, and ASRS. See who does what and why it matters.
Continue reading
Conveyor safety in a warehouse: guarding, e-stops, pull cords, crossovers, and lockout/tagout, tied to OSHA rules and ASME B20.1, with a daily checklist.
Continue reading
Conveyor belt tracking keeps a belt centered on its pulleys. Learn why warehouse belts wander, how technicians adjust them, and when to call for service.
Continue reading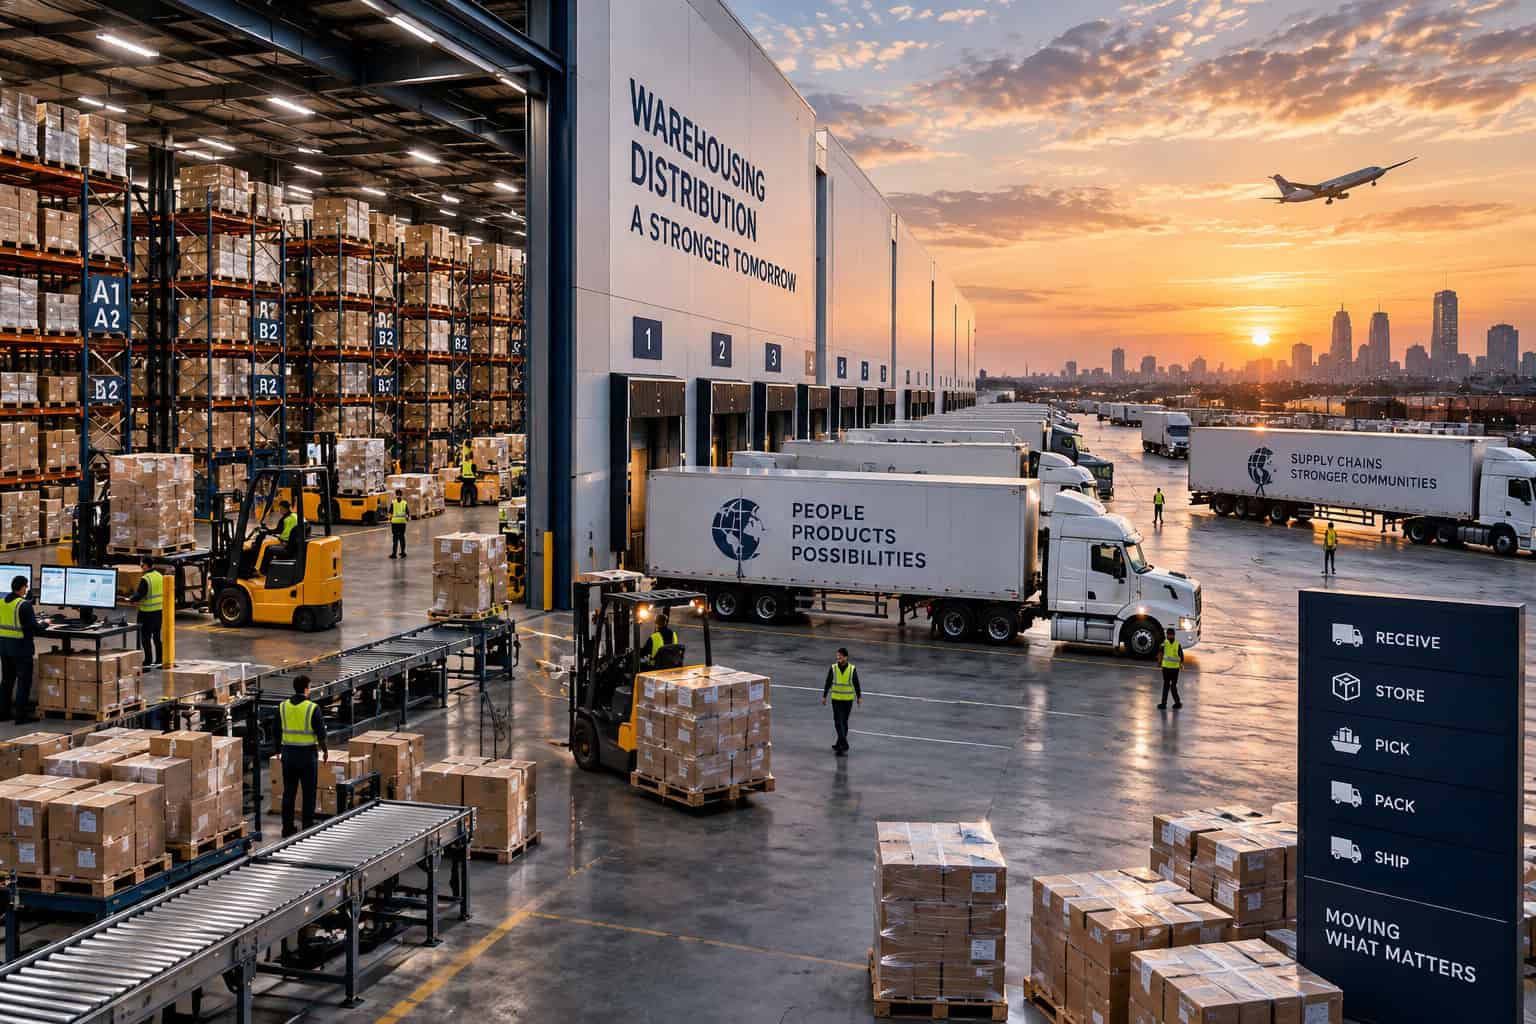
Warehousing and distribution operations play a critical role in getting products from storage locations to customers efficiently, accurately, and on time. As order volumes increase and fulfillment expectations continue to evolve, businesses need material handling systems that can keep pace with demand while controlling operating costs. Automation, conveyor technology, robotics, and warehouse control software can help distribution centers streamline workflows and improve productivity.
Century Conveyor Systems provides integrated material handling automation solutions for warehouses, distribution centers, and fulfillment facilities. From conveyor systems and automated sortation to robotic fulfillment, pallet handling, and warehouse control systems, the company helps businesses develop solutions tailored to their operational requirements.
Understanding how these technologies work together can help warehouse operators identify opportunities to improve performance, reduce manual handling, and prepare their facilities for future growth.
Below are frequently asked questions about warehousing and distribution and how Century Conveyor Systems can help businesses optimize their material handling operations.
Century Conveyor Systems offers integrated automation solutions designed to improve the movement, handling, sorting, and processing of products throughout warehouse and distribution environments. Rather than focusing on a single piece of equipment, the company approaches material handling as a connected system that supports the entire fulfillment process.
Its solutions include conveyor systems, sortation equipment, robotic fulfillment, robotic palletizing, controls and software, storage modules, and shipping-related equipment. These technologies can support products ranging from individual cartons and polybags to totes, drums, and full pallets.
For example, a warehousing and distribution center might use belt conveyors to move small packages, powered roller conveyors to transport cartons, and automated sortation equipment to direct shipments toward the correct destination. Robotic palletizing equipment can then help organize completed orders for outbound shipping. Warehouse control technology coordinates equipment and movement throughout the operation.
Century Conveyor Systems also provides project-related services, including system design, validation, installation, startup support, and parts and service. This integrated approach allows businesses to plan material handling improvements around their actual operational requirements.
The right solution depends on factors such as facility layout, product dimensions, order profiles, daily throughput, labor availability, and anticipated growth. By considering these factors together, businesses can develop a warehousing and distribution strategy that addresses current bottlenecks without overlooking long-term needs.
Conveyor systems help warehouses move products between operational areas with less dependence on manual transportation. Instead of requiring employees to carry cartons, push carts, or repeatedly move products between workstations, conveyors establish defined pathways that connect receiving, picking, packing, sortation, and shipping.
Century Conveyor Systems engineers conveyor solutions around the function of each section of a warehouse. Different products and workflows require different conveyor technologies, making equipment selection an important part of system design.
Belt conveyors, for example, provide stable movement for small packages, polybags, and irregularly sized cartons. Live roller conveyors are useful in applications that require powered movement, while gravity conveyors can support manual packing lines and other operations where products can move without a powered drive. Pallet conveyors are designed to accommodate heavier loads, with options selected according to pallet characteristics and handling requirements.
These technologies can improve warehousing and distribution efficiency in several ways. First, they reduce unnecessary travel between work areas. Second, they establish more consistent product flow, helping employees focus on value-added tasks. Third, they can support higher processing volumes by moving products continuously rather than relying entirely on individual handling.
Conveyors can also connect different stages of an automated workflow. When integrated with scanners, diverts, controls, and other material handling equipment, they help products reach the appropriate processing or shipping destination.
The goal is not simply to install more conveyor equipment. It is to design a layout that moves products through the facility efficiently, minimizes avoidable handling, and supports reliable throughput.
Yes. Warehouse automation can reduce the amount of repetitive manual work required to move, sort, and prepare products for shipment. Century Conveyor Systems designs and implements automated material handling systems intended to increase output while lowering labor costs.
Labor efficiency is particularly important in facilities where employees spend substantial time transporting products, manually sorting cartons, moving pallets, or transferring goods between departments. These activities are necessary, but they can consume time that employees could otherwise spend on inspection, exception handling, quality control, and other tasks requiring human judgment.
Automated conveyors create predictable transportation routes, while robotic mobile systems can move totes, cartons, carts, or pallets between designated locations. Automated palletizing equipment can further reduce the physical effort associated with stacking completed cases onto pallets.
Consider a distribution center where employees routinely move cartons from a packing area to several outbound staging lanes. A conveyor system with appropriately configured diverts could automate much of that transportation and routing. Employees could then focus on resolving exceptions, monitoring product quality, or managing outbound shipments.
However, labor savings depend on the facility’s starting conditions, system design, order volume, and implementation costs. Automation may change job responsibilities rather than eliminate every manual task. Businesses should evaluate labor productivity, throughput, equipment utilization, maintenance, and total operating costs when estimating potential returns.
Century Conveyor Systems’ integrated approach helps businesses assess how equipment and controls can work together to make warehouse processes more productive.
Robotic fulfillment helps automate the movement of goods within a warehouse, particularly when products must travel between storage, picking, packing, and shipping areas. Century Conveyor Systems offers solutions involving automated guided vehicles (AGVs) and autonomous mobile robots (AMRs), which can support different transportation requirements.
AGVs typically follow predefined routes using navigation technologies such as magnetic tape, QR codes, inductive wires, or laser-based guidance. They are suitable for operations that involve relatively consistent transportation paths, including moving pallets, cartons, or other loads between established locations.
AMRs use sensors and onboard navigation capabilities to move through a facility without relying on the same fixed route infrastructure. Their flexibility can make them useful in dynamic warehouse environments where transportation needs vary throughout the day.
One application is goods-to-person fulfillment. Instead of requiring employees to travel repeatedly to retrieve inventory, mobile robots can transport totes or other containers to picking or packing personnel. This approach can reduce unnecessary walking and help employees spend more time processing orders.
Robotic fulfillment can also support end-of-line operations, where finished products must be transferred from production or packing areas to another stage of the distribution process.
An important advantage is scalability. Depending on the application and system architecture, businesses may be able to introduce additional robots as demand increases. This can provide an alternative to making every transportation route permanently fixed in the facility.
Successful implementation still requires careful planning. Product weights, traffic patterns, charging requirements, safety procedures, floor conditions, and integration with existing equipment must all be considered. Century Conveyor Systems can help businesses determine where robotic transportation fits within a broader automation strategy.
Automated sortation systems direct products toward the correct destination based on the requirements of a distribution operation. In a busy warehouse, this may mean routing cartons to specific carrier lanes, shipping doors, customer orders, store destinations, or downstream processing areas.
Without an effective sortation process, employees may need to identify, lift, scan, and redirect individual packages manually. As volumes increase, these tasks can create congestion and increase the likelihood of misrouted shipments.
Century Conveyor Systems provides sortation conveyor solutions designed to support rapid product throughput. Its broader material handling capabilities include conveyor diverts, which direct cartons from one line to another without necessarily requiring a large, dedicated sortation system for every application.
The appropriate technology depends on the number of destinations, package characteristics, required processing speed, and available space. A straightforward operation may benefit from strategically placed conveyor diverts, while a high-volume distribution center may require a more advanced automated sortation configuration.
Sortation can improve performance by reducing manual transfers, establishing more consistent routing, and helping products reach the correct shipping area. When combined with appropriate scanning and control processes, it can also support more reliable order handling.
Accuracy is not determined by conveyor equipment alone. Product identification, order data, software configuration, exception procedures, and employee training remain important. Automated equipment must receive reliable information to route packages correctly.
For businesses experiencing shipping bottlenecks or frequent sorting errors, evaluating the complete path from packing to outbound staging can reveal opportunities to improve both speed and accuracy.
Yes. Warehouse automation does not always require replacing an entire facility or rebuilding every operational process. Many businesses can improve performance by modernizing specific areas, integrating new equipment with existing systems, or implementing upgrades in carefully planned stages.
Century Conveyor Systems offers retrofit and modernization capabilities alongside system design, mechanical installation, electrical installation, controls engineering, and project management. These services can help businesses evaluate how new material handling technology may fit within their current infrastructure.
For example, a warehouse may already have conveyor lines but experience recurring congestion near packing stations. An upgrade might involve changing conveyor configurations, introducing new diverts, improving controls, or automating a previously manual transfer point.
Another facility might need to expand outbound capacity without significantly disrupting daily shipping operations. Project phasing can help organize installation activities around operational priorities, available space, and acceptable downtime.
Integration requires more than determining whether a new conveyor physically fits. Engineers must also consider equipment interfaces, control logic, power requirements, traffic patterns, maintenance access, and the interaction between automated and manual processes.
Existing warehouse management systems and other operational software may also need to exchange information with new equipment. Proper planning helps ensure that automated workflows operate as intended and that employees understand how to respond to exceptions.
The most effective modernization strategy begins with identifying the specific operational problem. By targeting measurable bottlenecks instead of adding technology indiscriminately, businesses can make more informed investments in warehousing and distribution improvements.
Material handling equipment performs the physical work of transporting and processing products, but software and controls help coordinate how that equipment operates. Without appropriate control logic, conveyors, scanners, diverts, and robotic systems may not work together as an efficient, connected process.
Century Conveyor Systems offers controls and software capabilities that include programmable logic controllers (PLCs), control panel design and fabrication, warehouse management system (WMS) integration, and warehouse control systems (WCS).
A WMS generally supports warehouse-level inventory and order management functions, while a WCS coordinates and manages automated material handling activities. A PLC controls equipment behavior at the machine or process level. Although their responsibilities differ, these technologies can work together to connect business instructions with physical warehouse operations.
For example, an order may be released for fulfillment through a warehouse management process. Conveyors then transport cartons through the facility, scanners identify packages, and control logic directs each item toward the appropriate destination. If an exception occurs, the system may need to route the item to a designated handling area rather than allowing it to continue through the normal workflow.
Effective integration can improve visibility, coordination, and consistency. It can also help businesses identify operational constraints and better understand where delays occur.
Software selection and configuration should reflect the facility’s actual processes, existing technology, and future plans. Businesses should clarify system responsibilities, communication requirements, reporting needs, and exception-handling procedures before implementation.
When equipment and software are designed as parts of a coordinated system, distribution centers can establish more dependable workflows and make better use of their automation investments.
Product protection is an important consideration in warehousing and distribution because damage can result in returns, replacement costs, shipping delays, and dissatisfied customers. Material handling systems should be designed around the physical characteristics of the products being transported, including their dimensions, weight, packaging, and fragility.
Century Conveyor Systems offers several conveyor technologies that address different handling requirements. Belt conveyors provide a stable transportation surface for smaller parcels, polybags, and irregular cartons. Modular belt systems can offer advantages in specialized applications where traction, tight transfers, or easier belt maintenance are important.
Accumulation conveyor systems can also help control the spacing between products. Zero-pressure accumulation is designed to prevent products from touching, while minimum-pressure accumulation allows products to make light contact. These configurations can be useful when contact between packages presents a risk of damage.
The benefits extend beyond conveyor selection. Poorly planned transfers, abrupt changes in direction, congested workstations, and uncontrolled accumulation can all contribute to handling problems. A well-engineered layout accounts for how products enter, travel through, and exit each stage of the system.
Businesses should also evaluate package stability, transition points, sensor placement, conveyor speeds, and the behavior of products when lines temporarily stop. Fragile items may require different handling conditions from durable cartons or heavy palletized goods.
Preventing damage requires matching the equipment to the application rather than assuming one conveyor design is suitable for every product. With an appropriate combination of engineering, controls, and operating procedures, warehouses can reduce avoidable product contact and improve the consistency of their fulfillment processes.
Automated material handling equipment must be maintained to support reliable performance over time. Even a well-designed system can experience wear, component failures, sensor issues, or control problems if maintenance is neglected.
Century Conveyor Systems offers conveyor repair, preventative maintenance, replacement parts, equipment service, and related support capabilities. Its service offerings also include mechanical and electrical expertise for material handling systems.
Preventative maintenance helps identify developing problems before they cause significant operational disruption. Depending on the equipment, maintenance activities may include inspecting belts and rollers, checking motors and drives, evaluating sensors, examining mechanical components, and verifying that safety systems function properly.
Replacement parts are another important consideration. Facilities that depend on automated conveyors may experience substantial disruption when a critical component becomes unavailable. Maintaining appropriate spare parts and having a clear process for identifying equipment requirements can help streamline repairs.
Businesses should develop maintenance plans according to equipment specifications, operating hours, product loads, environmental conditions, and manufacturer recommendations. Maintenance records and recurring fault data can also reveal patterns that indicate the need for repairs or modernization.
Support requirements vary by location and service type. Century Conveyor Systems identifies its primary field service coverage in the New Jersey, Pennsylvania, and New York metropolitan area, while also offering replacement conveyor parts and equipment quotations for shipment to customer locations.
For distribution centers with demanding shipping schedules, maintenance should be treated as part of the overall automation strategy rather than an afterthought. Reliable equipment, accessible technical support, and well-planned servicing help protect the investment in warehouse infrastructure.
The decision to automate should begin with a clear understanding of current operational performance and the challenges a business wants to address. Automation can offer significant advantages, but the appropriate solution depends on the facility’s requirements, budget, order profile, and long-term strategy.
Businesses should first identify their most important constraints. These might include excessive employee travel, slow carton movement, limited shipping capacity, inconsistent order routing, repetitive pallet handling, or insufficient space for growing inventory volumes.
The next step is to establish a baseline using measurable operational indicators. Useful metrics include orders processed per hour, cartons handled per shift, labor hours per order, order accuracy, equipment downtime, product damage, and on-time shipping performance.
These measurements help determine whether the proposed system addresses a genuine business problem. For example, a conveyor upgrade may be valuable when transportation between packing and shipping is the primary bottleneck. Robotic fulfillment may be more appropriate when workers spend substantial time moving inventory containers. A sortation system may be the priority when outbound routing limits throughput.
The financial evaluation should consider more than the initial equipment price. Installation, software integration, facility modifications, maintenance, employee training, energy consumption, and future expansion can all influence the total cost of ownership. Expected benefits should be evaluated against these costs using realistic operating assumptions.
Century Conveyor Systems supports businesses through system design, validation, implementation, startup support, and ongoing parts and service. This provides a framework for assessing how a proposed solution fits within the facility’s wider operational goals.
A phased approach may be appropriate when a business wants to address its most urgent bottleneck before committing to a larger automation project. The key is to prioritize improvements that can be measured and aligned with long-term business objectives.
Efficient warehousing and distribution depend on more than moving products from one location to another. Businesses must coordinate transportation, order fulfillment, sortation, inventory movement, shipping preparation, software, and equipment maintenance to achieve consistent operational performance.
Century Conveyor Systems provides integrated material handling solutions that address these connected requirements. Conveyor systems can streamline product transportation, robotic fulfillment can reduce repetitive movement, automated sortation can improve routing, and controls and software can coordinate equipment throughout a facility. Maintenance and modernization services help businesses support system reliability as operational demands change.
The right combination of technologies depends on each facility’s products, workflow, available space, labor requirements, and future growth plans. A careful evaluation of these factors can help businesses identify practical opportunities to improve productivity, reduce unnecessary handling, and strengthen distribution performance.
Organizations considering their next warehousing and distribution improvement can contact Century Conveyor Systems to discuss their facility requirements and explore an automation solution designed around their operational goals.
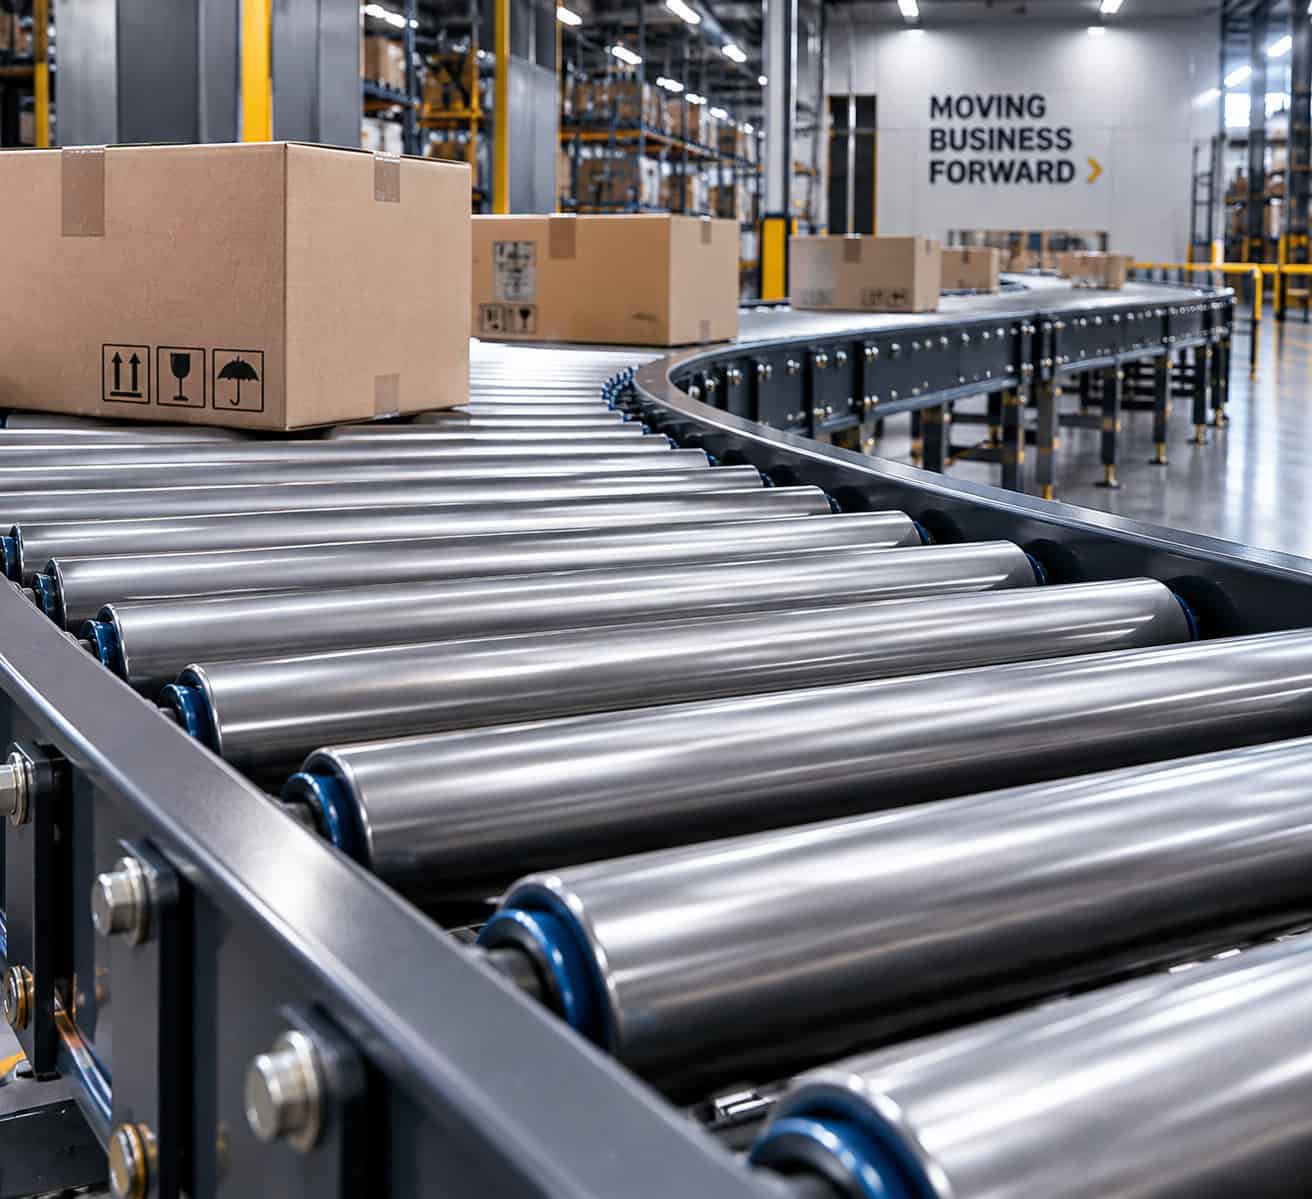
Conveyor rollers play an essential role in modern material handling, helping businesses move products efficiently, maintain consistent workflows, and manage the demands of high-volume operations. From distribution centers and warehouses to order fulfillment facilities, roller conveyor systems can simplify the movement of cartons, packages, totes, and other items throughout a facility. Selecting the right conveyor rollers, however, involves more than choosing components that turn freely. Businesses must consider product characteristics, conveyor layout, throughput requirements, integration with other equipment, and long-term operational needs.
Century Conveyor Systems provides material handling and order fulfillment solutions designed to help businesses improve the way products move through their operations. Understanding how conveyor rollers fit into a larger conveyor system can help facility managers, operations teams, and project planners make more informed decisions about equipment selection and system design.
The following frequently asked questions explore conveyor rollers, their role in material handling, and the considerations businesses should evaluate when planning a conveyor solution with Century Conveyor Systems.
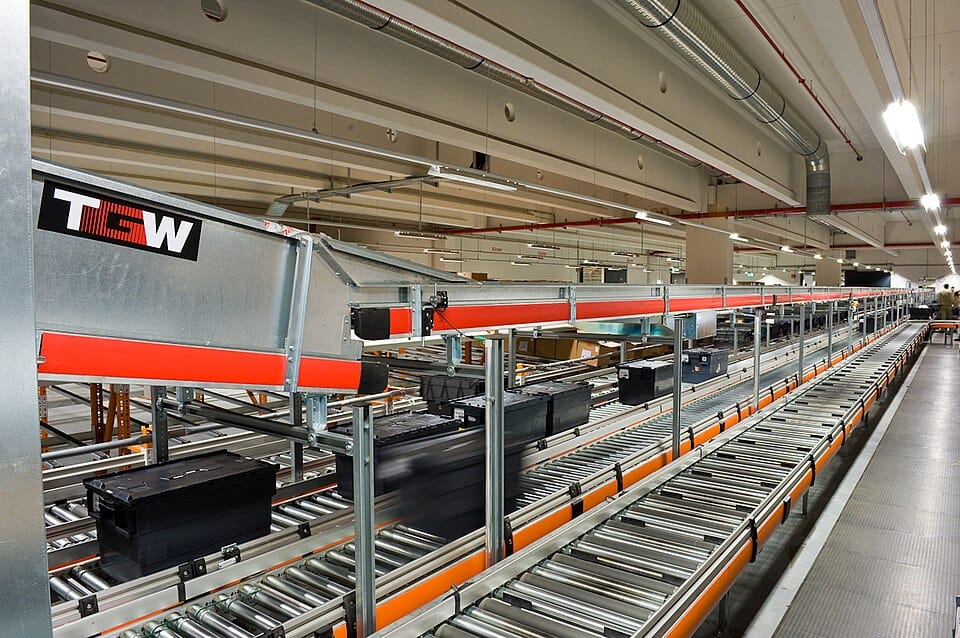
Conveyor rollers are cylindrical components that support and move products along a conveyor. As products travel across a roller conveyor, the rollers rotate beneath them, reducing the need for workers to carry or manually push items from one location to another. Depending on the conveyor design, movement may occur through gravity, manual pushing, or a powered drive mechanism.
Although an individual roller is a relatively simple component, its contribution to a material handling operation can be substantial. Rollers help establish a predictable path for products, making it easier to connect receiving, storage, picking, packing, sorting, and shipping activities within a facility.
For example, a distribution center may need to move cartons from an order picking area to a packing station and then onward to shipping. A properly designed conveyor system can provide a continuous route between these work areas, reducing unnecessary handling and helping employees focus on tasks that require human judgment or intervention.
Conveyor rollers are also important because their performance affects the behavior of the entire conveyor line. Roller spacing, load capacity, surface condition, alignment, and drive configuration all influence how smoothly products travel. If the rollers are unsuitable for the products being conveyed, items may hesitate, skew, accumulate improperly, or require additional manual assistance.
For businesses considering Century Conveyor Systems, the key is to evaluate conveyor rollers as part of a complete material handling strategy rather than as isolated parts. The right solution should support the products being moved, the distances they must travel, and the workflow the facility needs to maintain.
Order fulfillment involves coordinating multiple activities, often under strict expectations for accuracy and speed. Products must be picked, consolidated, packed, and routed toward the correct shipping destination. Conveyor rollers can help connect these activities by creating organized pathways between workstations and reducing the amount of manual product transportation required.
In an order fulfillment environment, roller conveyors may be used to move cartons away from picking locations, deliver totes to packing areas, transport completed orders toward sorting equipment, or direct packages to shipping zones. The specific application depends on the facility’s layout, the products being handled, and the design of the overall system.
One of the primary advantages is improved workflow continuity. Without an effective material handling arrangement, employees may spend considerable time walking products between stations, navigating crowded aisles, or waiting for work to arrive. Conveyor systems can help establish more consistent product movement, allowing different parts of the operation to function as a coordinated process.
Roller conveyors can also support more organized workspaces. Defined product routes help separate transportation from activities such as scanning, packing, and quality checks. When combined with suitable controls, accumulation zones, and other material handling equipment, conveyors can help manage the flow of orders during busy periods.
Century Conveyor Systems’ order fulfillment solutions provide a relevant starting point for businesses evaluating how conveyor equipment can contribute to a broader operational design. Rather than selecting rollers based solely on their physical specifications, companies should consider where products enter the system, how they move between processes, and where they need to exit.
A successful design aligns the conveyor arrangement with the order fulfillment process. This means considering peak demand, package variety, workstation placement, and the possibility of future changes. Conveyor rollers are most valuable when they support the complete journey of an order, not just one isolated movement.
Choosing conveyor rollers requires an understanding of the products being transported and the environment in which the conveyor will operate. A roller that works well for one application may be unsuitable for another, even when both systems appear similar.
Product weight and load distribution are important starting points. Businesses should determine the weight of individual items, the maximum expected load, and whether products will travel separately or in groups. The conveyor structure, rollers, supports, and drive components must be appropriate for the loads the system will experience. It is also important to account for uneven weight distribution, since a package may place more pressure on some rollers than others.
Product dimensions and base characteristics influence roller spacing and product stability. Cartons, totes, rigid containers, and other items may have different lengths, widths, and bottom surfaces. Roller spacing must provide adequate support as products travel along the conveyor. Items with small bases or irregular undersides may require a different arrangement from large, rigid cartons.
Movement requirements help determine whether a gravity or powered roller conveyor is appropriate. Gravity conveyors use a suitable incline and gravity to move products, while powered conveyors use a drive system to provide movement. The right choice depends on the available space, the distance products must travel, the required rate of movement, and how precisely product flow must be controlled.
Operating conditions also matter. Dust, moisture, temperature variation, cleaning procedures, and exposure to chemicals can influence material selection and maintenance needs. Facilities should communicate relevant environmental conditions before choosing conveyor components.
Finally, businesses should consider integration. Conveyor rollers must work with the conveyor frame, transitions, curves, transfers, sensors, controls, and other equipment in the planned system. Evaluating these factors together helps prevent mismatches that could affect reliability or require costly modifications.
When planning a solution with Century Conveyor Systems, a thorough application assessment can help identify the equipment configuration that best supports the facility’s operating requirements. The objective is to select conveyor rollers that are suitable for the actual workload, not simply those that meet a single specification.
Gravity and powered roller conveyors both use rollers to support products, but they differ in how products move and how much control an operation has over that movement.
Gravity roller conveyors rely on gravity, generally using a slight decline, or on manual force to move products along the conveyor. They can be useful for straightforward transportation between work areas where the layout and product characteristics permit consistent movement. Because they do not require a powered drive along every conveying section, gravity systems may offer a relatively simple solution for appropriate applications.
However, gravity conveyors depend on conditions such as conveyor slope, product weight, roller resistance, and the ability to control product speed. An excessive incline may cause products to move too quickly, while an insufficient incline may leave them stationary. Stopping, spacing, and releasing products may also require additional design considerations.
Powered roller conveyors use a motorized drive arrangement to move products. Depending on the system, powered sections can provide more consistent movement and support controlled transfers between operational areas. They may be useful in facilities where products need to travel across level surfaces, where movement must be coordinated with other equipment, or where the workflow requires more deliberate control over product flow.
Powered systems can also be designed to support accumulation, allowing products to wait temporarily in designated zones. This can help coordinate processes when downstream stations are busy, although the specific capability depends on the conveyor design and controls.
The right option depends on the application rather than a universal preference for one technology. Businesses should consider the required throughput, product characteristics, facility layout, available labor, control requirements, and total operating costs.
For Century Conveyor Systems projects, determining whether gravity or powered rollers are appropriate should be part of the broader system planning process. A conveyor that moves products adequately under normal conditions must also handle the expected fluctuations in demand without creating unnecessary bottlenecks.Writing
Yes. Conveyor rollers can be incorporated into systems that handle a wide range of products, but the conveyor configuration must match the items being transported. Cartons, rigid totes, polybags, drums, and pallets each present different handling challenges, so businesses should not assume that one roller arrangement will perform equally well for every product type.
Rigid cartons generally provide a reasonably stable base for roller conveyance, provided their dimensions and weight are compatible with the conveyor. Totes and containers may also travel effectively on rollers, particularly when their bases provide sufficient contact with the conveying surface. Larger and heavier loads, such as pallets, require equipment specifically engineered for the relevant load capacity and handling method.
Small parcels and flexible packages can be more challenging. Polybags, soft packages, and cartons with irregular dimensions may not remain stable on conventional roller conveyors. Their undersides may catch between rollers, or they may fail to maintain consistent contact with the conveying surface. In these applications, a belt-over conveyor can provide a more continuous supporting surface and improve product stability.
Century Conveyor Systems identifies live roller and gravity conveyors as options for applications such as packing lines, divert lines, extendable conveyors, and end-of-line operations. Its order fulfillment solutions also include belted conveyors for small polybags, parcels, and irregular carton sizes. These distinctions are important because they show why selecting material handling equipment should begin with the products themselves rather than with a predetermined conveyor type.
Businesses should assess the full range of items that will travel through the system, including unusually small, large, heavy, light, or fragile products. Seasonal merchandise changes and new packaging formats should also be considered. A conveyor system designed around only the most common carton size may encounter problems when product dimensions vary.
The goal is to create a conveying arrangement that maintains stability, protects products, and supports consistent movement across the expected range of operating conditions. If a facility handles multiple product categories, combining roller conveyors with belts, diverts, or other equipment may offer a more effective solution than relying on rollers alone.
One of the main reasons businesses invest in conveyor rollers is to reduce the time and effort required to move products through a facility. In operations where employees regularly transport cartons between picking, packing, and shipping stations, manual movement can consume valuable labor hours without directly advancing order processing.
A properly designed roller conveyor helps establish a repeatable path between work areas. Instead of carrying or pushing products over long distances, employees can place items onto the conveyor and allow the system to transport them toward the next stage. This can reduce unnecessary walking, limit repetitive material handling, and make workstation responsibilities easier to organize.
The benefits extend beyond transportation. When workstations are connected by an appropriately designed conveyor layout, teams can coordinate product movement more effectively. For example, completed packages can travel toward a shipping area while employees remain focused on packing and verification. Divert sections can direct cartons toward different destinations, while suitable accumulation arrangements can help coordinate upstream and downstream processes.
These improvements are particularly relevant to high-volume fulfillment operations, where small inefficiencies can accumulate across thousands of orders. If employees repeatedly walk across a warehouse to transfer packages, the combined time spent on these movements may reduce the time available for picking, packing, and other productive activities.
Century Conveyor Systems describes its material handling approach as a turnkey process that includes system design, validation, implementation, installation, startup support, and ongoing parts and service. This broader approach matters because conveyor efficiency depends on how equipment fits into the operation, not simply on the presence of rollers.
For instance, installing a conveyor between two poorly positioned workstations may shorten one movement but create congestion elsewhere. Likewise, a system with insufficient capacity can cause products to accumulate at bottlenecks. Effective planning considers the entire workflow, including where products enter, how they are processed, and how quickly they must reach their destinations.
Businesses should evaluate performance using practical measures such as throughput, labor hours per order, product damage rates, waiting time, and order accuracy. These measurements help determine whether the conveyor installation is delivering meaningful operational improvements.
Conveyor rollers can serve as important components within larger automated material handling systems. Although rollers primarily support product movement, the conveyor sections around them can be integrated with equipment that directs packages, controls spacing, and coordinates movement between different destinations.
In a distribution center, for example, packages may arrive from picking or packing stations and need to be routed to different shipping lanes. Conveyor lines can carry products toward divert mechanisms that send cartons to their designated destinations. Depending on the system, these mechanisms may use roller-ball diverts, skate wheels, push-trays, swinging arms, or other transfer technologies.
The distinction between transportation and sorting is important. Rollers help move products along a path, but the overall system must also determine where each product should go and when it should move. Sensors, programmable logic controllers, control panels, and warehouse control software can help coordinate these processes.
Accumulation is another important consideration. When a downstream workstation cannot accept additional packages, an appropriately designed accumulation conveyor can hold products temporarily until space becomes available. Century Conveyor Systems describes zero-pressure and minimum-pressure accumulation options for managing product spacing and helping reduce contact-related damage. The appropriate configuration depends on the products, operating conditions, and desired flow characteristics.
Integration becomes especially valuable when a facility needs to coordinate multiple processes. A conveyor line might connect packing stations to automated sortation equipment, which then directs orders toward shipping lanes. In a more advanced operation, conveyor systems may also interface with robotic fulfillment equipment or automated mobile robots.
However, more automation is not automatically better. Businesses should identify the actual operational problem before investing in additional equipment. A simple roller conveyor may be sufficient for straightforward transportation, while a high-volume distribution center may benefit from integrated controls and automated sorting.
Century Conveyor Systems offers a range of material handling solutions, including conveyor systems, sortation equipment, controls and software, and robotic fulfillment. Considering these capabilities together can help businesses plan an arrangement in which conveyor rollers serve a clear purpose within the wider automation strategy.
Regular maintenance helps preserve conveyor performance, identify developing problems, and reduce the risk of unexpected downtime. Even a well-designed conveyor system experiences wear as rollers, bearings, drive components, and supporting structures operate under repeated loads.
A maintenance program should begin with routine inspections. Operators and maintenance personnel should look for rollers that fail to rotate freely, unusual noises, visible damage, misalignment, loose components, and signs of excessive wear. Changes in product movement can also indicate that a component needs attention. For example, cartons that repeatedly stop at the same point may indicate a damaged roller, an obstruction, or an alignment issue.
Cleaning is another consideration. Dust, packaging debris, labels, and other materials can interfere with roller rotation or accumulate around moving parts. The appropriate cleaning procedure depends on the operating environment and the equipment manufacturer’s recommendations. Maintenance teams should avoid introducing cleaning agents or methods that could damage components.
Powered roller conveyors require additional attention to the drive system and associated controls. Depending on the design, inspections may include motors, belts, chains, sensors, electrical connections, and safety devices. Maintenance work should follow established lockout and safety procedures, with equipment isolated before personnel access hazardous moving parts.
Preventive maintenance is generally more effective than waiting for a component to fail. Scheduled inspections can help identify deterioration before it interrupts production, while maintenance records make it easier to recognize recurring issues and plan replacement activities.
Century Conveyor Systems provides conveyor preventative maintenance, repair services, and replacement parts as part of its broader service offering. Businesses evaluating conveyor rollers should consider how maintenance responsibilities will be handled after installation, including access to appropriate parts and qualified technical support.
A useful maintenance strategy should reflect actual operating conditions. A lightly used conveyor may require a different inspection frequency from a system running multiple shifts every day. Load levels, environmental conditions, operating hours, and the consequences of downtime should all influence the maintenance plan.
The objective is to keep the conveyor system safe, reliable, and suitable for the workload while avoiding unnecessary maintenance interruptions.
Replacing conveyor rollers or upgrading an existing conveyor system may become necessary when equipment no longer meets operational requirements. However, replacement decisions should be based on the condition and performance of the system rather than age alone.
One warning sign is recurring mechanical trouble. Rollers that repeatedly seize, develop excessive noise, or fail to support consistent product movement may indicate wear or damage. If repairs become frequent, maintenance costs rise, or spare parts are increasingly difficult to obtain, businesses should evaluate whether continued repairs remain practical.
Changes in operational demand can also justify an upgrade. A warehouse that originally handled a limited number of product types may eventually need to accommodate a larger range of package sizes, higher order volumes, or different shipping processes. Existing rollers and conveyor sections may no longer provide the necessary capacity, stability, or control.
Layout changes are another consideration. Expanding a packing area, adding a shipping lane, introducing automated sorting, or reorganizing storage can change the way products need to move through a facility. In these situations, the best solution may involve modifying the conveyor layout rather than replacing every component.
Businesses should also investigate whether problems attributed to the rollers actually originate elsewhere. Incorrect alignment, unsuitable spacing, worn drive components, inadequate controls, or an inappropriate conveyor design can create similar symptoms. Replacing individual rollers without correcting the underlying issue may provide only temporary relief.
Century Conveyor Systems offers retrofit and modernization solutions alongside conveyor repair, parts, and broader system integration services. This makes a system-level assessment a sensible starting point when an existing installation no longer supports the operation effectively.
Before approving an upgrade, businesses should document current problems, estimate the cost of continued maintenance, assess the consequences of downtime, and define the performance improvements they expect. They should also consider whether the proposed changes will accommodate future requirements.
The most effective upgrade is not necessarily the largest one. Replacing worn components may be sufficient in a well-designed system, while a facility facing fundamental throughput or layout limitations may need a more comprehensive redesign.
Selecting conveyor rollers is only one part of creating a dependable material handling operation. Businesses also need to consider system design, equipment integration, installation, maintenance, and how the conveyor will support their long-term operational goals.
Century Conveyor Systems focuses on material handling automation for warehouses, distribution centers, and fulfillment facilities. Its capabilities span conveyor systems, sortation, robotic fulfillment, controls and software, storage solutions, and conveyor service and parts. This range is relevant to businesses that need to evaluate rollers within a complete workflow rather than purchase components without considering their role in the wider operation.
A system-oriented approach can help businesses identify the most appropriate combination of equipment. Some applications may require gravity rollers for straightforward product transfers. Others may benefit from powered live roller conveyors, belt-over sections for irregular packages, accumulation equipment for managing product spacing, or specialized pallet handling solutions for heavier loads.
The right recommendation depends on the facility’s specific requirements. Relevant information includes product dimensions, load weights, expected throughput, available floor space, operating schedules, existing equipment, and future expansion plans. Providing these details helps establish a realistic starting point for system planning.
Support after installation is equally important. Conveyor systems need appropriate maintenance, replacement parts, and technical assistance to remain productive over time. Century Conveyor Systems lists preventative maintenance, conveyor repair, parts, and project support among its services, allowing businesses to consider both initial implementation and ongoing equipment care.
Companies should approach the selection process with clear performance objectives. Rather than asking only which conveyor rollers to purchase, they should determine what the system needs to accomplish: reduce manual handling, improve package flow, accommodate new product types, increase throughput, reduce damage, or connect previously separate operations.
For businesses planning an order fulfillment improvement project, Century Conveyor Systems’ order fulfillment solutions provide a useful starting point for exploring conveyor and automation options. Its main website also provides an overview of its material handling capabilities and service offerings.
Conveyor rollers can make a meaningful difference in the way products move through warehouses, distribution centers, and order fulfillment facilities. Their effectiveness depends on selecting suitable components, matching the conveyor configuration to the products being handled, and integrating the equipment into a well-planned material handling process.
Businesses should evaluate load requirements, package dimensions, movement methods, maintenance needs, and opportunities for automation before committing to a particular solution. They should also recognize that roller conveyors may work best alongside belts, divert equipment, accumulation sections, and other technologies when product characteristics or workflow requirements demand additional capabilities.
Century Conveyor Systems offers a broader material handling perspective that can help businesses assess these decisions in the context of their operational goals. By focusing on the complete product journey—from receiving and processing to packing, sorting, and shipping—companies can make more informed decisions about conveyor rollers and the systems that support them.
Ultimately, the right conveyor solution should deliver more than movement. It should help create a safer, more organized, and more productive operation that can adapt to changing business demands.

An MDR conveyor uses 24V motorized rollers to drive each zone. Learn how zone cards work and how MDR compares with line shaft and live roller conveyor.
Continue readingRobotic palletizing explained: how a cell works, cobot vs. industrial arm vs. gantry, mixed-SKU pallets, what drives the cost, and where it fits your line.
Continue reading