Sorting Conveyors FAQ 101: Understanding Century Conveyor Systems’ Amazing Conveyor System Integration

sorting conveyors

When warehouses and distribution centers need to move, route, and process products more efficiently, sorting conveyors can become a critical part of the material handling strategy. But selecting a conveyor is only one piece of the automation puzzle. The larger challenge is integrating conveyors with controls, software, sortation equipment, order fulfillment processes, and the physical layout of a facility.

Century Conveyor Systems approaches this challenge as a full-service system integrator. The company describes its work as turnkey material handling automation for warehouses, distribution centers, and fulfillment facilities, covering everything from system design and validation through installation, startup support, and ongoing parts and service.

The following FAQ explains how Century Conveyor Systems’ conveyor system integration approach can apply to sorting conveyors and broader order fulfillment operations.

sorting conveyors

What are sorting conveyors, and why are they important in an automated warehouse?

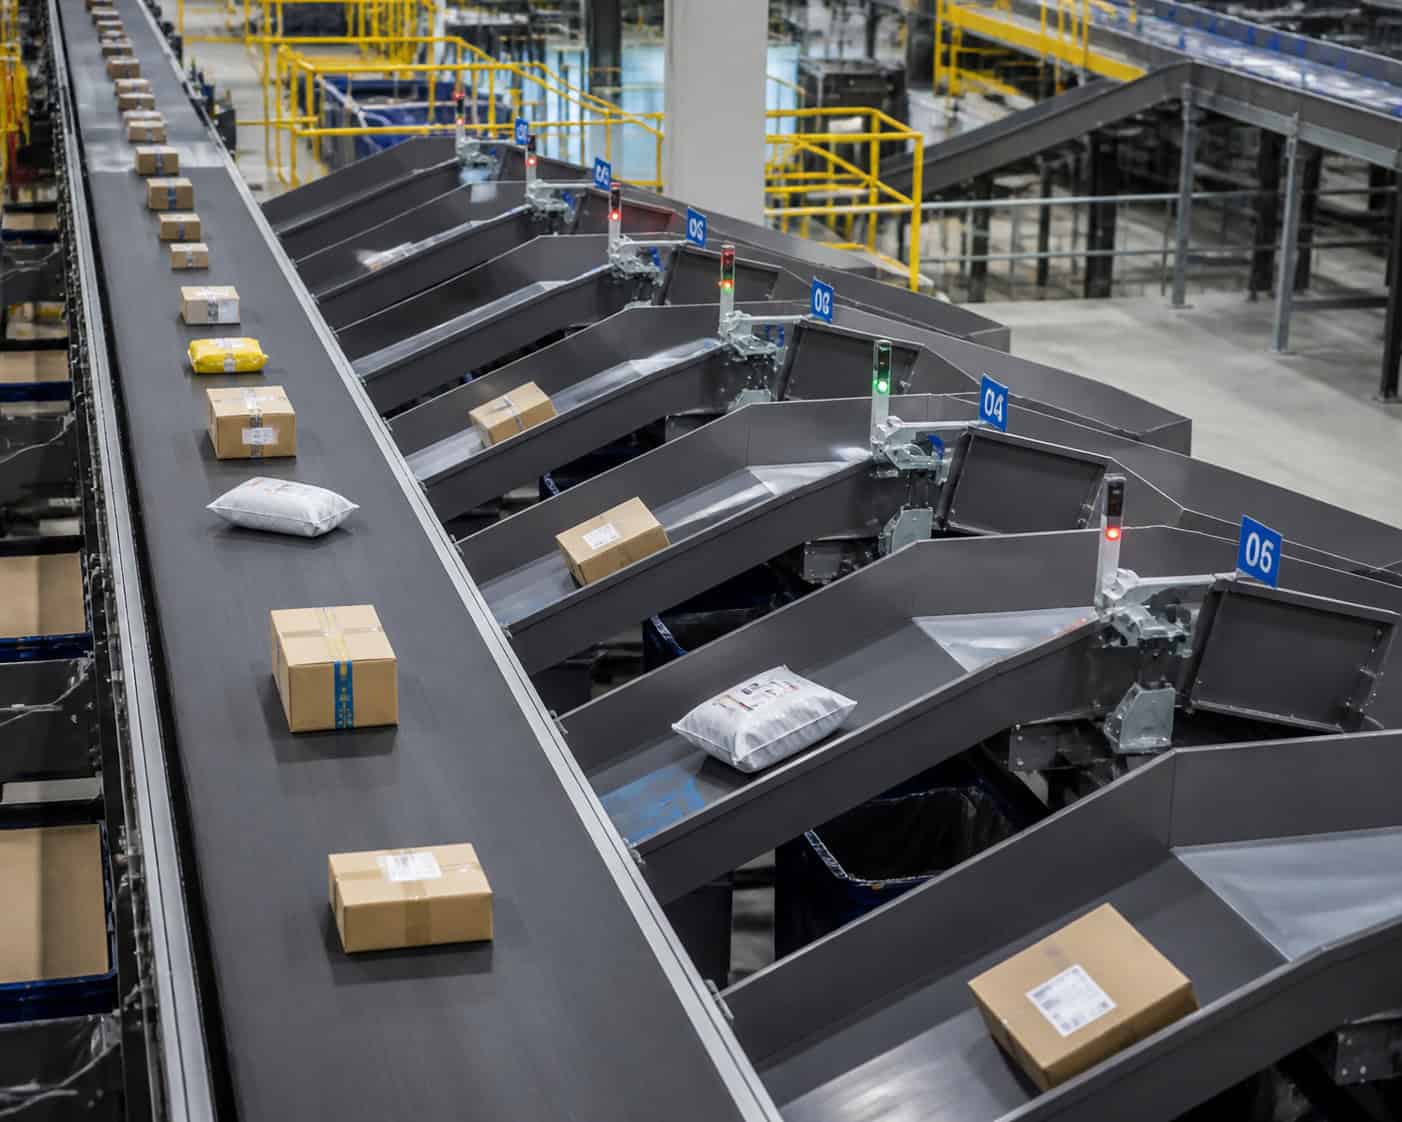
Sorting conveyors are material handling systems designed to route products, cartons, totes, or other items toward specific destinations within a facility. Rather than simply moving a product from point A to point B, a sorting conveyor system helps determine where an item should go and then directs it to the appropriate lane, workstation, packing area, shipping destination, or other process.

That distinction matters because modern fulfillment operations often have many destinations operating simultaneously. A conveyor system may need to move products from receiving or picking areas toward packing, then separate orders according to shipping requirements, customer destinations, carrier routes, or other operational criteria.

Century identifies sortation conveyors as one of its core solutions, with equipment including shoe, belt, tray, and Bombay distribution systems. The company positions these systems as rapid-throughput sortation equipment within a larger portfolio of material handling automation.

The value of sorting conveyors therefore goes beyond the conveyor hardware itself. A well-integrated system can connect transportation and sortation processes so that products keep moving through the facility with fewer unnecessary manual touches.

For businesses evaluating sorting conveyors, the key question should not simply be, “Which conveyor should we purchase?” A better question is, “How should the conveyor system work with the rest of our operation?”

How does Century Conveyor Systems approach conveyor system integration?

Century’s approach is broader than supplying individual conveyor components. The company describes itself as a full-service integrator, with system engineers responsible for designing, validating, and implementing turnkey systems. Its stated process encompasses system design, validation, final installation, startup support, and lifetime parts and service.

This integrated approach can be especially important for sorting conveyors because sortation typically sits within a network of other equipment and software. The conveyor must physically transport products, but controls and software also have to coordinate how products move through the system.

Century’s listed capabilities include concepts and design, controls engineering, control panel design and fabrication, electrical and mechanical installation, project management, project phasing, human-machine interfaces, and preventative maintenance.

That range of capabilities creates a more unified approach to automation. Instead of treating mechanical equipment, electrical controls, software, and installation as isolated projects, system integration brings those elements together around the facility’s operational goals.

For a warehouse considering sorting conveyors, this can mean evaluating the entire material flow before determining how the sortation equipment should be configured.

Why should sorting conveyors be planned around the entire order fulfillment process?

A conveyor can move a package efficiently and still fail to improve an operation if it does not fit the overall fulfillment process.

Century describes order fulfillment as the sequence of activities beginning when a fulfillment center receives an order and continuing until the item reaches the shipping dock for loading. Its stated goal is to optimize performance at each operational touchpoint, reduce errors that can contribute to returns or damaged products, and process items faster with fewer manual interactions.

This systems-level perspective is particularly relevant to sorting conveyors.

Consider a fulfillment operation in which products are picked manually, transported by conveyor, sorted into different destinations, packed, labeled, and ultimately sent to shipping. Improving only one segment may create a bottleneck somewhere else. A faster sorter could overwhelm downstream packing stations. More accumulation could require different controls. A new conveyor route could interfere with pedestrian traffic or existing equipment.

System integration addresses these relationships before equipment is installed.

Century offers multiple conveyor technologies that can serve different portions of an order fulfillment system. Its portfolio includes live roller and gravity conveyors, belted conveyors, modular belt conveyors, conveyor diverts, zero- and minimum-pressure accumulation conveyors, extendable conveyors, spiral conveyors, and pallet conveyors.

The important point is that sorting conveyors do not necessarily operate alone. Their effectiveness depends on how well the entire material flow is designed.

How can Century integrate different conveyor technologies into one system?

Different products and operational steps require different forms of conveyance. A small polybag may need a different handling approach than a large carton or pallet, and an accumulation zone has different requirements from a high-speed sortation area.

Century notes that live roller and gravity conveyors can be used for packing lines, divert lines, extendable applications, and end-of-line operations. Belted conveyors can provide stable handling for small polybags, parcels, and irregular cartons, while also supporting inclines, declines, and gapping. Modular belt conveyors provide a different belt construction that can be easier to clean, modify, or maintain for certain applications.

Conveyor diverts provide another integration point. According to Century, diverts can move products from a single conveyor line to other lines without requiring a large sortation system in every application. Different divert mechanisms can be selected depending on the product and required movement.

This illustrates why conveyor integration should begin with material characteristics and workflow rather than with a particular piece of equipment.

A successful design may combine several conveyor types, each performing a specific job. Sorting conveyors can handle routing, while accumulation equipment manages spacing, belt conveyors stabilize certain products, and gravity or live roller sections support packing or end-of-line processes.

The result is a system designed around the operation rather than a collection of disconnected conveyor components.

Can sorting conveyors work with robotics and other warehouse automation?

Yes. Sorting conveyors can be one component of a broader automated fulfillment environment that also includes robotics.

Century offers robotic fulfillment solutions involving automated guided vehicles (AGVs) and autonomous mobile robots (AMRs). The company describes AGVs as suitable for transporting pallets, cartons, and non-conveyable products along static routes, while AMRs can navigate more freely through a facility and are suited to applications such as goods-to-person fulfillment.

This creates opportunities for hybrid automation.

For example, a facility could use conveyors for predictable, high-volume product movement while using mobile robots for flexible transportation between areas that are difficult or inefficient to connect with fixed conveyor. The appropriate balance depends on the facility, product mix, throughput requirements, and operational objectives.

Century also states that its robotic fulfillment solutions can be scalable and flexible, with systems capable of being added later and customized for specific handling requirements.

The broader lesson is that sorting conveyors do not have to represent the entirety of a warehouse automation strategy. They can be integrated into a larger system in which fixed conveyors, sortation equipment, controls, and robotics each handle the tasks they are best suited to perform.

How do controls and software fit into a sorting conveyor system?

The mechanical conveyor is only part of an automated material handling system. Controls and software determine how equipment operates together and how products are directed through the facility.

Century lists controls and software among its primary solutions, including control panel fabrication, programmable logic controls (PLC), Warehouse Management Systems (WMS), and Warehouse Control Systems (WCS).

This layer of integration is especially important for sorting conveyors because sortation decisions need to correspond with the operational information associated with each product or order.

A conveyor can physically send an item toward several possible destinations, but the system needs a reliable method for determining the correct destination and coordinating equipment at the appropriate time. Controls can manage conveyor operation and equipment interactions, while warehouse software can provide information needed to support the overall fulfillment process.

For that reason, specifying sorting conveyors without considering controls and software can produce an incomplete automation plan.

Century’s system integration model combines engineering disciplines so the mechanical equipment, electrical systems, controls, and operational objectives can be considered together.

What makes conveyor system integration valuable for long-term performance?

A conveyor project should not end when the equipment is installed. Warehouses change, equipment requires maintenance, and production requirements can evolve.

Century lists conveyor preventative maintenance, repair services, replacement parts, mechanical and electrical installation, and ongoing service among its capabilities. The company also states that it has more than 40 years of conveyor experience and an established service department.

This long-term perspective is valuable when evaluating sorting conveyors because reliability directly affects the operation’s ability to keep products moving.

Century also notes that well-maintained conveyor systems can last more than 20 years and that additional solutions can be added to conveyor lines to increase automation.

That makes maintainability and future expansion important considerations during the initial design.

A system designed only for today’s throughput may eventually become a constraint as order volumes, product types, or fulfillment requirements change. A system designed with scalability in mind can provide more flexibility for future modifications.

The objective, therefore, is not simply to install sorting conveyors that work today. It is to develop an automation platform that can continue supporting the facility as its requirements evolve.

What should a company consider before contacting Century about sorting conveyors?

Companies should begin by documenting the operational problem they want automation to solve rather than selecting equipment first.

Useful information can include current and projected throughput, product dimensions and weights, order profiles, destinations, peak volumes, existing conveyor equipment, available floor space, staffing requirements, current bottlenecks, and desired future capabilities.

It is also useful to identify where errors, manual handling, product damage, or delays occur. Century specifically emphasizes improving output performance, reducing errors that can cause returns or breakage, and processing items faster with less manual interaction in its order fulfillment approach.

From there, a system integrator can evaluate whether sorting conveyors are appropriate and how they should interact with other technologies.

Century encourages prospective customers to provide project details when beginning an automation optimization project, after which an automation expert can respond with next steps.

For organizations exploring conveyor automation, this approach can help shift the conversation from purchasing equipment to engineering a complete solution.

Where can I learn more about Century Conveyor Systems’ conveyor integration services?

The best starting point is Century Conveyor Systems’ official website, where the company outlines its conveyor, sortation, robotic fulfillment, controls and software, storage, print-and-apply, service, and other material handling capabilities.

For a closer look at order fulfillment applications, visit Century’s Conveyor and Order Fulfillment Systems page. The page covers conveyor types, diverts, accumulation, pallet handling, robotic fulfillment, AGVs, and AMRs.

Ultimately, sorting conveyors are most effective when they are treated as part of a complete material handling strategy. Century Conveyor Systems’ conveyor system integration approach brings conveyor equipment together with engineering, controls, installation, project management, and ongoing service. For warehouses and distribution centers seeking higher throughput and more coordinated automation, that systems-level approach can be more valuable than choosing a conveyor in isolation.
AGV and AMR vs. Conveyor Systems: Drive Efficiency With The Best Solution for your Warehouse.

agv and amr vs conveyor comparison blog post header image
agv and amr vs conveyor system comparison blog post header image

Automatic Guided Vehicles (AGV) and Autonomous Mobile Robots (AMR) have existed for years now, offering robotic material handling operations for a multitude of warehouse operations. The industry is well aware of its pros and cons, and supply chain executives are content with placing them within their arsenal of automated warehouse solutions.

The much harder decision when automating is understanding which solution will provide the most benefit, as opposed to if it will at all. In the case of AGVs and AMRs, conveyor systems are tried and true forms of automation that continue to provide exceptional output and return-on-investment. While both solutions differ in engineering and functionality, both exist for the same goal- reliable, stable, and quick movement of items. How do AGVs/AMRs stack up against traditional conveyor systems? Where does one solution shine, while another does better in a different application?

Century has experience integrating both and understands where and how these systems outperform one over the other. We wanted to share some of our insights so you can evaluate what works best for your warehouse.


newsletter sign up element

AGV and AMR

AGVs and AMRs are often grouped together, mostly because the operations they perform overlap with each other. The single main difference between the two is its form of sensing and moving throughout the environment. AGVs move by using a sensor that follows a set path (typically a form of sticker or tape on the ground-hence the word “guided” in its name). AMRs move by sensing objects around them, and learning an optimal path (hence the word “autonomous” in its name).

This characteristic defines what operations are typically assigned to an AGV or an AMR. Essentially, AGVs work best at moving cartons and pallets across the facility with little to no variation in its traveling path. AMRs shine in picking operations, where it would not have a set path.

AGV


Effective in moving, tugging, and towing cartons or pallets from a single location to another.

  • Carts
  • Tuggers
  • Lift-Truck
  • Pallet Jack
  • Unit Load

AMR


Assistance in multi-variable operations that require diversion in movement paths.

  • Picking
  • Sortation
  • Inventory Control
  • Sanitization

AGVs and AMRs have seen expanded use over the course of the past year, and most new warehouses are built with the notion that automation will be implemented at some point. According to Research and Markets, United States, Germany, U.K., China and Japan are going to lead the market with an annual demand of more than 200,000 mobile robots (AGV & AMR) by 2026.

To put the cost-effectiveness of an AGV and AMR into perspective, Annual costs for a forklift operator can run up to $50,000. If a forklift has to be operated around the clock, then at least 3-4 drivers are needed. Adding the invest costs of $10,000 for a forklift truck to the personnel costs, the annual costs for one forklift come to over $200,000 (ResearchAndMarkets.com). Depending on the output of the warehouse, operating AGVs and AMRs can save thousands over traditional manually operated lift trucks.

Automated robotic solutions continue to improve as newer technologies are created and adapted. Artificial intelligence (AI), machine vision, voice-to-robotic-pick, and warehouse data-driven learned actions continue to provide added functionality and benefit to AGVs and AMRs (primarily the latter). This makes AGVs and AMRs a forward-facing implementation, as abilities are added to their repertoire of functionality through the advancement of warehouse technologies and software capabilities.

Conveyor

Conveyor systems are the typical solution of any automated operation, offering a continuously moving assembly line to quickly complete the processing and distribution of a package. Conveyors use belts or rollers to move cartons or pallets, powered by motors. Each warehouse that employs conveyors has a specially engineered layout, consisting of a variety of conveyor sections, depending on function.

Conveyor Section Types

  • Infeeding
  • Straight
  • Curved
  • Incline
  • Decline
  • Divert
  • Merge
  • Switch
  • Outfeeding

Conveyors produce the best results when implemented in fast-moving post-production operations such as order fulfillment, product distribution, sortation, and crossdocking. Conveyors are highly customizable, with the number of systems that can be added to the conveyor line spanning from carton forming to in-trailer loading, and everything in-between. Conveyors have proved the test of time as being the main system of reliable and quick movement in a warehouse. There’s a reason they’re still in use for over 100 years. The output rate is unmatched and its simplicity in design help it to easily integrate with other cutting-edge automation solutions.

The Most Important Factor: Your Warehouse

If you were to ask us what system we would use, we would ask “what’s your warehouse like?”. This is the number one question you should ask yourself as you’re exploring solutions. The effectiveness and benefit of these solutions are only relevant if integrated correctly in your distribution center, warehouse or facility.

To simply it even further- think on your answer to this question. Can your operations continue effectively if you install a “bolted-down” conveyor system. If the answer is a definite “NO”, then you’ll most likely benefit more from the use of AGVs and AMRs. A fully engineered conveyor system is not mobile, and if your warehouse has limited space, or needs open lanes for lift trucks to travel in, a conveyor system may not be ideal. That’s not to say it’s impossible to engineer, but an AGV or AMR would be a more realistic solution.

With that in mind, here’s our comparison between AGVs/AMRs and conveyor systems.

The Comparison

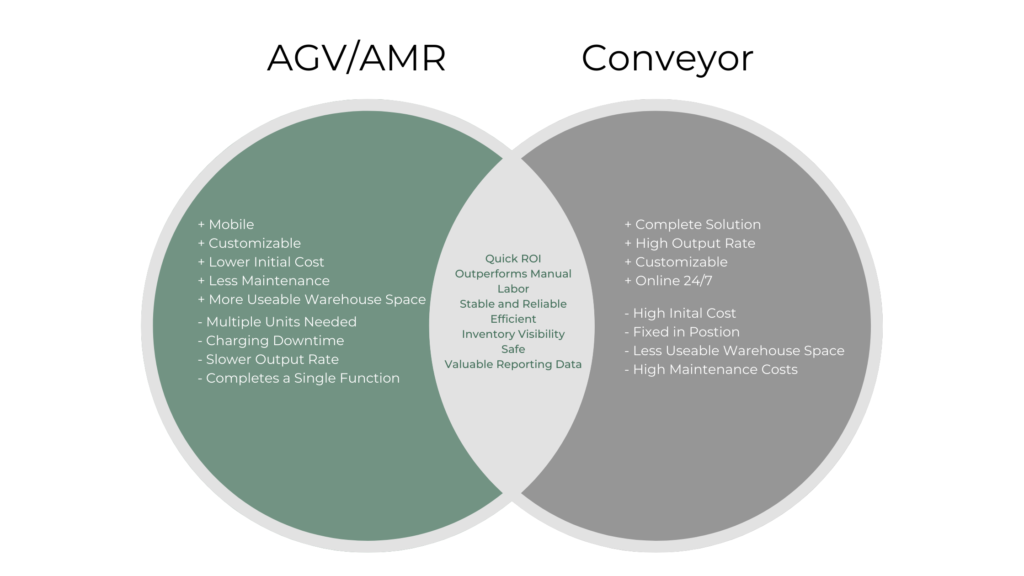
AGVs AMRs Vs Conveyor

Key Takeaway

Both systems will complete the task of transporting product across a warehouse, it’s that your operations and facility space will determine which one will work better.

AGVs/AMRs are ideal for warehouses that have:

  • Limited space and cannot install a conveyor system.
  • Extensive pick operations
  • Forklifts transporting the majority of items
  • A healthy output rate (5,000 to 20,000 cartons shipped per day)

Conveyor systems are ideal for warehouses that have:

  • Flexible space arrangements
  • A variety of package types
  • Extensive sortation operations
  • A high-output rate (20,000+ cartons shipped per day)

Both AGVs/AMRs and conveyors can benefit in more ways than one, and in many cases, are both implemented in a facility to maximize distribution operations.


century conveyor boilerplate element

Ahead of the Trend: The Rise of eCommerce in the Wine and Spirits Industry

rise of ecommerce in wine and spirits industry blog header image
rise of ecommerce in the wine and spirits industry blog header image

Online sales directly to the consumer in the wine and spirits industry used to be a tiny niche, compared to typical distribution methods, but the newest trend, fueled by COVID, is anything but.

In 2020, bars and restaurants shut their doors, leading consumers to make the decision to shop online. U.S. E-commerce sales of alcohol increased more than 80% in value during the pandemic (IWSR). A year later, the sales have plateaued, but are still 15% to 20% higher than pre-pandemic levels. Consumers turned to online shopping because of an external factor, and a surprising number have stuck around after that factor has been eased.

Online liquor stores have seen increases in sales, spurring investor interest. Last February, Uber purchased Drizly for $1.1 billion (Barrons). Consumer interest is certain to increase in eCommerce purchasing as users adopt the buying behavior, and experience the benefits over traditional liquor store visits. Along with Drizly, a few other online liquor stores run in the races, including:

Uptown Spirits

ReserveBar

Thrive Market

Wine.com

Bright Cellars

Nestor Liquor

Minibar

Flaviar

Wine.com

How does this affect the wine and spirits industry? Supply chains will have to accommodate for order fulfillment, that is having the necessary material handling solutions in place to ensure an order gets packed, labeled, and sorted to its end destination. This is quite different from what is typically processed in a wine and liquor distribution operation.

Cartons (usually packed within 6 bottles) are sent to be palletized or loaded in a truck, which makes deliveries to liquor stores, bars, and restaurants. With an online order, each package is customized and can contain a variety of items (kitting).

Wine and liquor warehouses will have to store individual items, accurately pick and pack them, apply a shipping label, and send them to the customer’s doorstep safely and within a few days’ time.

Integrating order fulfillment is a carefully planned and engineered project, but the long-term growth and profits will dwarf the initial investment once implemented fully.

Order fulfillment is one of Century’s specialties. We’ve had experience in the past engineering systems specifically for eCommerce operations, and we’d like to pass along our recommendations on the solutions that are used.

1. Storage and Pick Modules

Managing a fully stocked wine and spirits warehouse can get complicated when a large variety of products are offered. This creates a need for both short-term and long-term pallet storage. Automation in the form of an ASRS (automatic storage and retrieval system) can rapidly retrieve pallets that need to be distributed or store long-term inventory in the most optimal spot within a racking system.

An ASRS uses a crane attached to a horizontal and vertical track, scaling the racking structure, and using extendable forks to handle pallets. The operator terminal provides information on what product is stored where, and the ASRS operates when a retrieve or store command is inputted.

2. Conveyor System

A tried-and-true conveyor system will be the most accurate, simple, and efficient solution for a wine and spirits warehouse. Conveyors are dynamic in the sense that there are hundreds of additional solutions that can be integrated in the layout. Being highly customizable, each conveyor system is engineered according to the layout of the wine and spirits operation.

In the wine and spirits industry, the key to stable operations is ensuring cartons avoid damage. A zero-pressure accumulation conveyor (like this conveyor, manufactured by Hytrol) does not allow cartons to touch, by properly maintaining space between each and stopping the rollers when the accumulation zone is full. This is especially important when fulfilling specific customer orders that may include unevenly sized items.

3. Pack Tables

In order fulfillment, stations are positioned at infeeding operations so that orders can be packaged and sent to a label application. A worker or autonomous robot picks the products and brings it to a pack table. The worker checks to ensure that the order is correct in places in any invoicing documents, and places the items in the package with void-fill.

Pack tables are simple to integrate, and sit aside a main conveyor, so that workers can simply push orders from their tables onto the conveying surface.

4. Print and Apply Stations

Affixing identifiable tags on packages is crucial to ensuring their deliverability. Scanners and sensors across the line depend on a readable tag for it to make it to its destination. Print and apply systems do exactly that. However, there are multiple systems depending on the identification process use and where the box must be marked. Applications can roll-on, wipe over, corner wrap, air blow, and stamp labels.

The direction the box must be scanned also plays a role in a solution selection, but it will outpace manual operations regardless.

5. Sortation

Sortation systems separate products for induction into individual lanes typically associated with an outbound destination. Various types of sortation and conveyor systems are often connected to comprise a fully functioning material handling solution.

The type of sortation integrates highly depends on what product is being moved. For a fragile wine and spirits operation, care must be taken in selecting a stable method of diverting the packages. Sliding Shoe and Narrow Belt sorters are best suited for safely, yet quickly, sending items to where they need to be.

narrow belt sortation
Narrow belt utilizes thin belts so that rising directional skate wheels activate when a package is to be diverted down a destination lane.

sliding shoe conveyor sortation
Sliding shoe uses segmented plastic slats that gently divert cartons to an outfeeding conveyor.

6. Warehouse Management System

The ability to have complete visibility of your warehouse inventory at all times is paramount to operating effectively. A warehouse management system (or WMS) stores vital information such as alcohol percentage, storage location, best-by dates for rotation, and a multitude of SKU data for ordering. A WMS can even offer a best shipping rate selector and presents data with correct state alcohol regulations applied.

Besides being a source of important product information, a WMS can apply that information within your warehouse operations. For example, if the wrong item is picked and placed on an outbound conveyor, the scan tower will read the label and the WMS will recognize it is in the wrong batch, stopping that section of conveyor and sounding an alarm for a worker to remove the incorrect item.

7. Reverse Logistics

Returns are a constant area of disconnect in operations when it comes to order fulfillment. There needs to be a planned intake process to return the items to storage and re-fulfill the order with the correct products.

When returns enter back into a warehouse, they’re put in a separate staging area. Depending on the condition of the item, or whatever the nature of the return is, it may be returned to inventory, sent to another distributor who sells discount items or discarded.

Once a return item has been rescanned in the system, the customer’s order will either be marked as fulfilled (so they can receive their money back) or another order will be placed (in the event they were sent the wrong item, but they still need the correct item sent to them).


Century Systems has extensive experience in integrating warehouse automation systems in the wine and spirits material handling industry. View the video below on a system we engineered and integrated with Fedway Associates.

7 Conveyance Solutions for Robust Handling of Various Product Types

ARB Solutions 2

Conveyor systems are versatile machines, working in tandem with a variety of material handling solutions, ensuring increase output and productivity. Besides the additions of machines in conjunction with a conveyance solution, there exists extended automation for the conveyor system itself.

Belting plays a critical role in how the product moves throughout the system, but typically, most operations use either a roller conveyor or a flat belt. What many do not realize is that belting can be upgraded to automatically position cartons in a way that simplifies various induction steps in the line.

ARB (Activated Roller Belt) technology revolutionizes the way a conveyor system functions by offering automatic aligning and positioning, precise gapping, high-speed sortation and diversion, uniform operator station package distribution, and more.

ARB equipment performs a variety of different functions on the product by utilizing free-spinning rollers that are embedded in plastic belt modules. The rollers can bi-directionally manipulate products in a variety of different angles and trajectories. The rollers can be bi-directional or omnidirectional depending on the usage of that specific belt space. The rollers reorientate themselves rapidly depending on the destination of the package.

ARB equipment can provide substantial throughput benefits while providing a quick return on investment by eliminating time-consuming manual labor and being flexible enough of a solution to apply to a variety of operations.

  • Sortation
  • Depalletizing
  • Singulators
  • Merges
  • Switching
  • Zone Picking
  • Infeeding and Outfeeding

1. Sortation Systems

DARB S4500 Sorting Belt

90-degree sortation

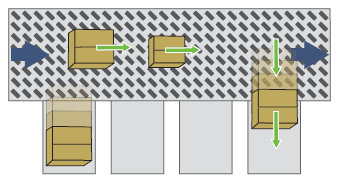
Bi-directional right-angle sortation that activates the belt rollers when the carton reaches its divert destination. This form of sortation is high speed, with rates up to 250 packages a minute, in a compact footprint. If your facility distributes a variety of packages, this sortation method can accommodate polybags, crates, top-heavy items, and more, along with typical flat-bottomed cartons.

ARB Sorter S7000

Bulk sortation

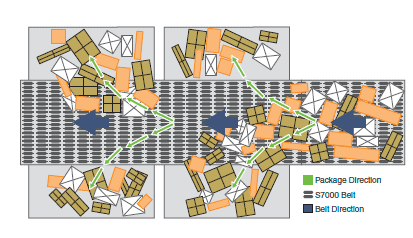
In facilities where a continuous flow of a mix of bulk packages is present, ARB equipment can be employed to sort an even volume of packages for downstream processing (operator stations, for example). Due to the bulk nature of the continuous induction, sortation rates can achieve up to 360 packages per minute, automatically avoiding jams.

2. Depalletizing Systems

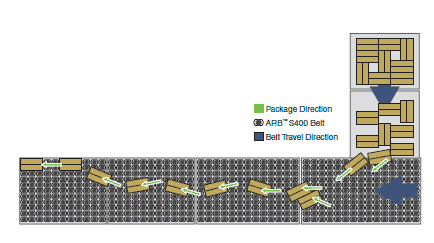
ARB Pallet Layer Descrambling S400

Depalletizing can be a laborious operation if done manually. With ARB equipment in use, omnidirectional track rollers can descramble up to 6 pallet layers per minute and place them in a uniform line, ideal for scanning or picking. By alternating packages left and right on the ARB conveyor, and using the side railing as a guide, packages line up neatly for downstream applications.

3. Singulators

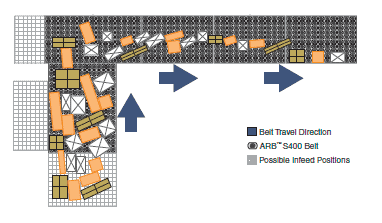
ARB Singulating Belt

Singulating, in this context, means to place the items in a single, congruent line. Depending on induction rates, this could be a continuous line, or broken up into segments (for example, one segment having four packages). ARB equipment moves the undistributed packages from left to right to acquire a straight line, using the railing of the support to gently align the items. This eliminates the need for manual clearing of side-by-sides, recirculation due to miss-sorts, and enables workers to place items on without concern for positioning.

4. Merges

Polybag ARB Merging

Polybag merging

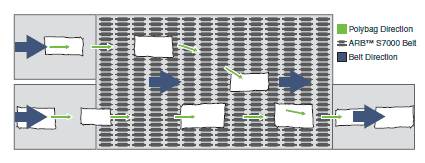
In a polybag-focused operation, reliable merging from multiple infeeds is paramount to downstream processes. ARB conveyor solutions merges infeed conveyors with a high-speed directional belt, while maintaining gapping, and alignment, for later scanning and sortation operations. All of this is completed in a relatively small footprint, as an ARB conveyor is designed to quickly merge the lanes.

5. Switching

Polybag Switching and Aligning

Polybag destination switching

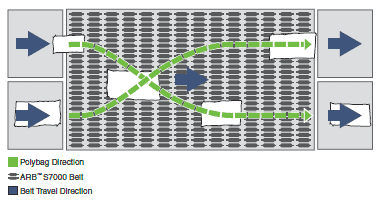
If lanes are not merging, but instead, crossing polybags over each other to their reach their destination lane, an ARB conveyor solution can achieve this efficiently. Much like the merging ARB conveyor, omnidirectional rollers quickly switch polybags into their respective destination outfeeds, while maintaining proper gapping and alignment.

6. Zone Picking

Zone picking

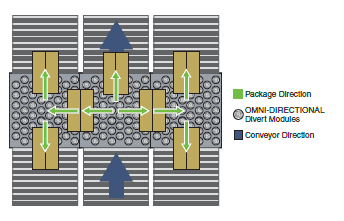
Pick and pass order fulfillment zones can also benefit from ARB equipment inclusion. Manual picking stations can be added to a central conveyor merge, utilizing an omnidirectional sorter to easily pick packages from the main line to be processed, and then re-introduced back to that same conveyor. Order fulfillment can be completed at rates greater than 25 packages per minute, and only needs one 24-volt motor to drive the rollers.

7. Infeeding and Outfeeding

Infeeding and Outfeeding ARB

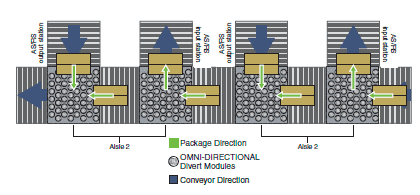
Used in conjunction with an automatic storage and retrieval system (AS/RS), this ARB conveyor combines both infeeding and outfeeding operations. Packages can both be sent to storage, while simultaneously accepting packages coming from storage. This is achieved by utilizing omnidirectional sorters in conjunction with right angle diverters, with alternating flow directions that activate depending on the carton’s destination. Sortation can achieve excess of 30 packages per minute, while infeed/outfeed rates to an AS/RS can reach 1,800 cases or totes per hour.

Intralox equipment has been successfully implemented by retail, grocery, manufacturing, and direct-to-consumer e-commerce distribution centers. The technology brings value in many applications ranging from high-speed 90-degree sorting to AS/RS infeeding and outfeeding. From increased throughput to flexible package handling and efficiency, Intralox’s conveyance technologies pick up where traditional technologies end.


Century is a longtime partner and integrator of Intralox, utilizing its innovative ARB equipment technologies throughout a wide range of clients. Together, a truly efficient system can be designed, engineered, and installed to increase output, accuracy, and ROI.

Post-COVID Parcel Customer Expectations

parcel industry customer expectations blog post header

How automation solutions fulfill today’s parcel shipping demands

post covid parcel expectations automation solutions

Parcel delivery expectations have increased exponentially, exacerbated by the effects on consumers of the pandemic, and the movement of large E-commerce players offering 1-day or even same-day shipping. Consumers expect quick shipping in comparison to a decade ago when a speedy delivery was a premium option.

In a recent report by McKinsey & Co., online product categories have experienced a 15% to 40% increase in user growth during 2020. That increase of users means higher expectations for faster shipping speeds, and in turn, carriers and shippers will be expected to offer and fulfill such services.

To accommodate the demand, automation has been utilized to rapidly speed up processing and sortation operations. Forgoing manual labor opens the door to quick shipment offerings, a tantalizing benefit to any prospective client. Automated solutions typically depend on the conveyor and divert systems, which need to be versatile enough to handle small parcels like letters and polybags, to larger carton packages. Belt conveyors are used, versus roller, as smaller items could get stuck in between rollers if the weight is undistributed across incorrectly. Where automation differs, is in its sortation method:

Tilt-tray

Tilt-tray sortation uses order consolidation chutes to sort items in a batch-pick environment. Cartons are scanned before being inducted onto a tilt-tray carousel, where it will sit on a moving platform until it reaches its destination chute.  The tray will tilt either left or right depending on where it’s being sorted and slide down a chute onto a conveyor to be loaded.

Tilt-tray applications are effective for high-speed sortation.

Cross-belt

Functioning similar to the tilt-tray, cross-belt sortation differs by using bi-directional belts to divert items into destination chutes. Packages are inducted onto the cross-belt conveyor carousel and sorted accordingly. Each belt section can hold one package, but multiple belt sections can be combined and used in tandem to divert larger items.

Narrow-belt

A series of narrow belts, each with its own take-up, span the length of the conveyor. High friction divert wheels rise between the belts, diverting product to its destination.

Narrow belts are typically used for larger, heavier packages that need heavy-duty forms of sortation. Smaller packages would not be ideal for this application, as they would fall in-between the belting segments.

Shoe Sorter

High-speed sorter utilizing aluminum slats that have plastic shoes that slide across them to divert cartons either left or right (bi-directional) to required sort destinations.

The advantage this provides over the similar functions of the tilt-tray is that the shoe is incorporated as part of the central induction conveyor. This eliminates the need for a separate sortation application, like the aforementioned tilt-tray carousel.

Split-tray Sorter

Sometimes also referred to as a bomb-bay sorter, dual split tray sorters have the ability to sort two smaller items within the same tray, at higher throughput speeds.

Split-tray sections have a bottom platform that opens to drop items gently into chutes, totes, or cartons below. This method is space-saving, as the item discharge area drops below vs being conveyed.

Swivel Wheel Sorter

Swivel wheel sorters utilize a platform of omni-directional rollers to divert items quickly. When a product reaches the divert, the wheels orientate to direct the item to its destination. This sortation method works best for systems that have a conveyor junction, rather than a gradual merge or curve.

Push-tray Sorter

A high-speed sorter with tray segments utilizing a positive divert to gently push items or polybags off the tray and slide them into a sortation chute.

Depending on the dimensions of the parcel processed, each conveyor sortation method varies slightly, and one solution may work better than another one. It’s a function of careful engineering and planning to discover which one would work best. Regardless, any conveyor sorter will far exceed manual labor.

Parcel Customer Expectation

pullquote graphic parcel industy automation

Mainly attributed to the increase in e-commerce usage, the courier, express, and parcel (CEP) market is expected to exhibit a CAGR of over 6% from 2021-2026 (source). To adjust to this substantial demand increase, automation and technology are taking center stage to provide future solutions. Parcel distributors have their work cut out for them, as operations need to accommodate for the increase, as well as deliver to customers within 1-2 days.

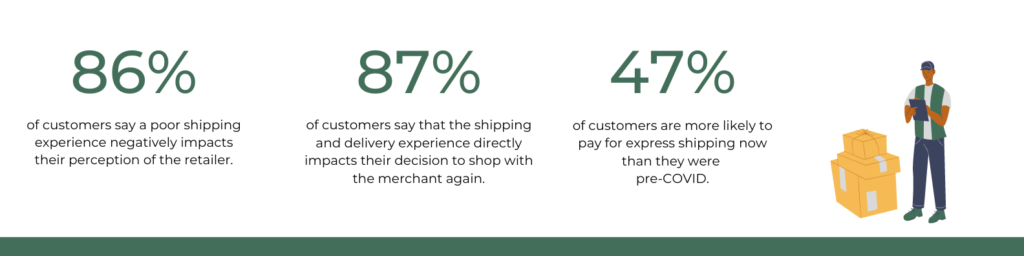
ShipStation’s report “Last Touch, Lasting Impact” highlighted insightful statistics in how consumers view various topics concerning shipping. A few pertaining to parcel shipping expectations include:

  • 86% say a poor shipping experience negatively impacts their perception of the retailer.
  • 87% say that shipping and delivery experience directly impacts their decision to shop with the merchant again.
  • 47% of customers are more likely to pay for express shipping now than they were pre-COVID.
parcel industry customer shipping expectation stats

Clients strive to uphold the best delivery experience for their customers, and that expectation extends to their parcel handling partner. Recurring slow shipping speeds and errors in sortation can spur negative consumer sentiment or increase returns, something clients work very hard to avoid.

The parcel industry is a constantly evolving sector, as automation technology continues to provide solutions for quick handling and delivery of packages. The post-COVID explosion of online shopping has led many forward-thinking parcel shippers to evaluate their current operations and develop an integration plan.


Century Systems understands how critical effective parcel operations are to maintain customer delivery satisfaction. Our primary focus is to engineer an automated solution that provides a profitable output and is curated specifically to your warehouse layout.