WMS Systems 101: Frequently Asked Questions About Century Conveyor Systemsโ€™ Warehouse Management Solutions

wms systems

WMS systems are under increasing pressure to fulfill orders faster, improve inventory accuracy, reduce labor costs, and keep operations running smoothly. As order volumes grow and customer expectations rise, businesses need more than traditional material handling equipment to remain competitive. They need intelligent technology that connects warehouse processes, coordinates equipment, and supports efficient order fulfillment.

This is where WMS systems play an important role. Warehouse Management Systems help businesses manage and coordinate essential warehouse activities, while integrating with automation technologies that can improve productivity and operational visibility.

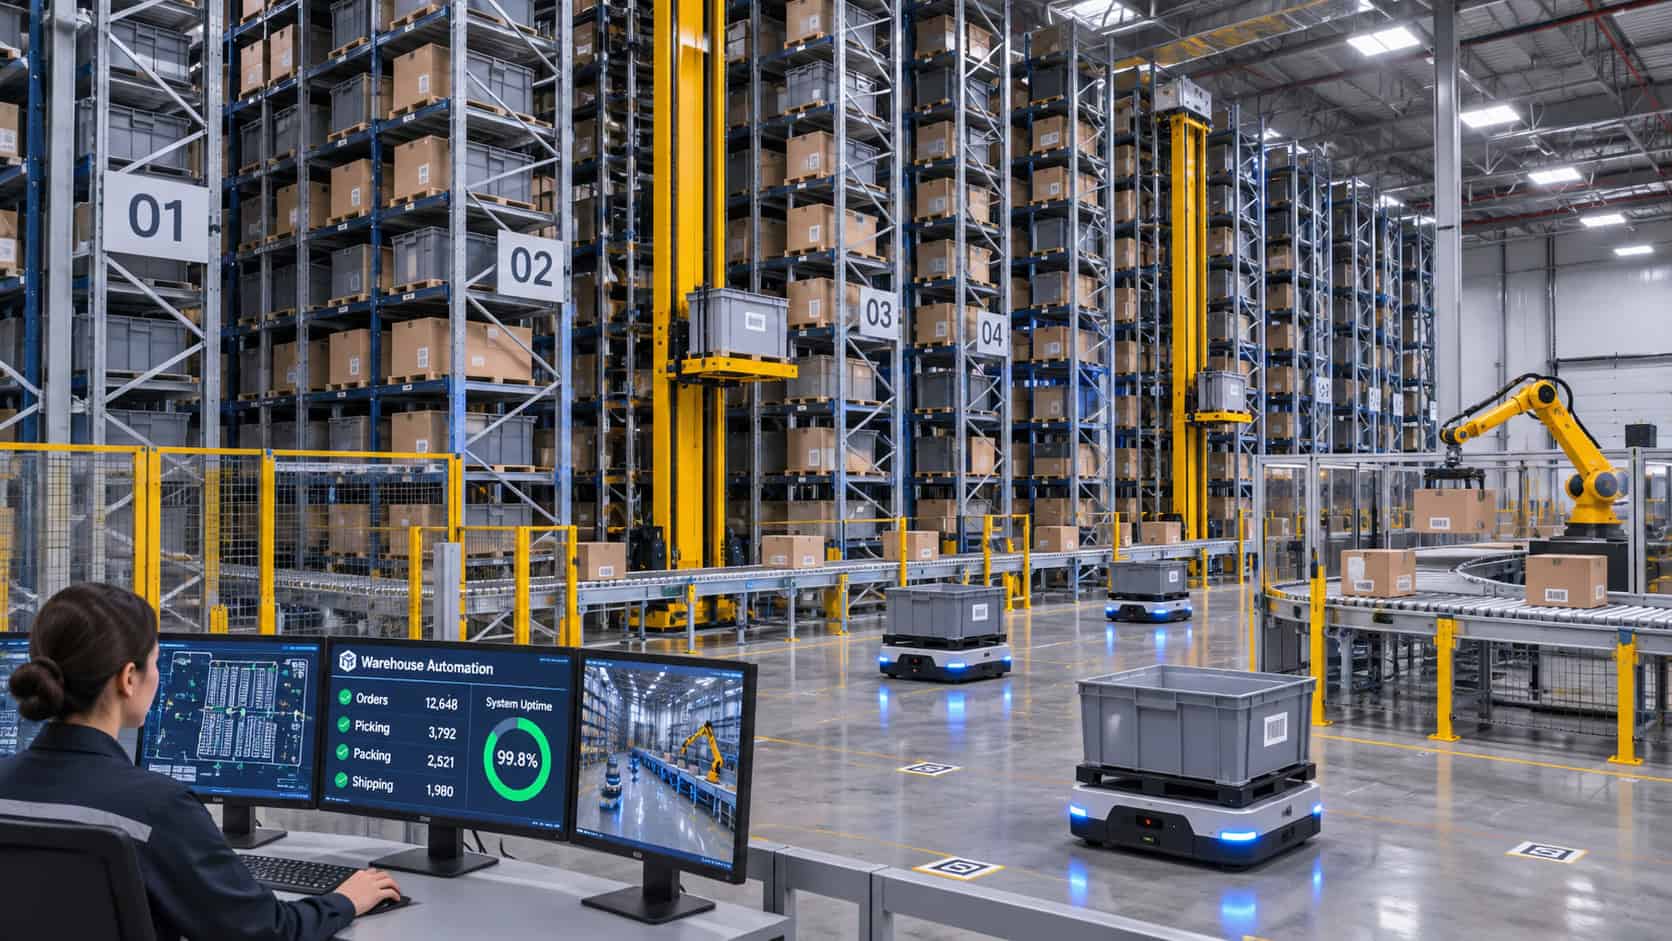
Century Conveyor Systems provides comprehensive warehouse automation and material handling solutions, including Warehouse Management Systems (WMS), Warehouse Control Systems (WCS), conveyor systems, robotic fulfillment, sortation equipment, and customized storage solutions. By bringing these technologies together, Century helps warehouses and distribution centers develop more efficient, scalable operations.

Below, we answer some frequently asked questions about WMS systems, Century Conveyor Systems’ capabilities, and how warehouse automation can help businesses improve their fulfillment processes.

wms systems

Frequently Asked Questions About WMS Systems

1. What are WMS systems, and why are they important for warehouse operations?

WMS systems, or Warehouse Management Systems, are software solutions designed to help businesses manage and coordinate warehouse activities. They provide an organized approach to overseeing inventory, managing warehouse workflows, and supporting the movement of products through a facility.

A warehouse involves numerous interconnected processes, including receiving, storage, inventory management, picking, packing, and shipping. Without an effective management system, coordinating these activities can become increasingly complicated as order volumes increase.

WMS systems help businesses organize these processes and establish more consistent workflows. They can support inventory visibility, improve the coordination of warehouse activities, and help managers make more informed operational decisions.

Their importance becomes even more apparent in facilities that use automated material handling equipment. When warehouse operations involve conveyors, sortation equipment, robotic systems, and automated storage solutions, effective software coordination becomes essential.

Century Conveyor Systems offers WMS and WCS solutions as part of its broader controls and software capabilities. Rather than treating warehouse software as an isolated investment, Century approaches automation as an integrated system designed around the facility’s operational requirements.

2. How does Century Conveyor Systems help businesses implement WMS systems?

Century Conveyor Systems takes a comprehensive approach to warehouse automation, providing more than individual pieces of material handling equipment. The company works with shipping warehouses, distribution centers, and fulfillment facilities to design, validate, and implement turnkey automation systems.

Its capabilities include controls engineering, software solutions, mechanical engineering, system design, installation, project management, and ongoing support.

When considering WMS systems, businesses should evaluate how software will interact with their existing warehouse infrastructure and future automation plans. A solution must account for the facility’s workflows, equipment requirements, operational capacity, and fulfillment objectives.

Century’s system integration approach helps businesses consider these requirements together. Its engineers work to develop solutions that increase output while reducing labor costs through the deployment of automation.

This integrated approach is particularly valuable for companies that want to modernize multiple areas of their warehouse rather than investing in disconnected technologies that may not work effectively together.

3. What is the difference between a WMS and a Warehouse Control System (WCS)?

Although Warehouse Management Systems and Warehouse Control Systems are closely related, they serve different purposes within an automated warehouse.

A WMS primarily focuses on managing warehouse operations and inventory-related activities. It helps organize the broader processes involved in storing, tracking, picking, and shipping products.

A WCS focuses more directly on coordinating automated material handling equipment and controlling how products move through an automated facility.

For example, a warehouse might use a WMS to support inventory and order management while relying on a WCS to coordinate conveyor movement, sortation processes, and other automated equipment.

Both technologies can contribute to a more efficient operation, but they address different layers of warehouse management and automation.

Century Conveyor Systems offers both WMS and WCS capabilities within its controls and software solutions. This gives businesses the opportunity to consider how warehouse management software and equipment-level controls can work together as part of a larger automation strategy.

Understanding this distinction is important when planning a new warehouse or upgrading an existing facility. Businesses should consider both their operational management requirements and the level of control needed for their automated equipment.

4. Can WMS systems improve order fulfillment efficiency?

Yes. Improving order fulfillment efficiency is one of the most important reasons businesses invest in warehouse management technology and automation.

Order fulfillment involves every step between receiving an order and preparing the products for shipment. This includes locating inventory, retrieving products, transporting items, picking orders, packing packages, sorting shipments, and delivering completed orders to the shipping dock.

When these processes rely heavily on manual labor, bottlenecks and inconsistencies can develop. Employees may spend excessive time walking between picking locations, moving products, or manually sorting packages.

WMS systems can help organize warehouse workflows, while integrated automation can reduce unnecessary manual handling and improve the movement of products throughout the facility.

Century Conveyor Systems specializes in engineering order fulfillment solutions designed to improve output performance, reduce errors that contribute to returns or damaged products, and process items faster with fewer manual interactions.

Its solutions include:

  • Conveyor systems that automate the movement of cartons and pallets.
  • Robotic fulfillment systems that transport products throughout the warehouse.
  • Sortation equipment that directs packages to the appropriate destinations.
  • Goods-to-person solutions that bring inventory closer to fulfillment personnel.
  • Picking and storage systems designed to support efficient inventory access.

Combining effective warehouse management with these technologies can help businesses develop a more streamlined fulfillment operation.

5. How do WMS systems work with conveyor automation?

Conveyor systems are an important component of many automated warehouses. They provide a continuous method of transporting cartons, packages, and pallets between different operational areas.

However, conveyors do more than simply move products from one location to another. In an automated warehouse, they can support coordinated workflows involving picking, packing, sorting, accumulation, and shipping.

WMS and WCS technologies can contribute to the coordination of these activities, depending on the system architecture and integration requirements.

Century Conveyor Systems designs conveyor solutions around the specific layout and operational needs of each facility. Available equipment includes live roller conveyors, gravity conveyors, belted conveyors, modular belt conveyors, conveyor diverts, pallet conveyors, and extendable conveyors.

Each conveyor type serves a different purpose.

For example, belted conveyors provide stable transportation for small polybags, parcels, and irregularly shaped cartons. Conveyor diverts help direct packages toward different operational lines, while pallet conveyors provide reliable movement for heavier loads.

Accumulation conveyors can also help prevent products from making contact with one another, reducing the potential for damage during transportation.

By integrating the right conveyor equipment with appropriate warehouse management and control technologies, businesses can establish a more coordinated material handling environment.

6. Can WMS systems support robotic warehouse automation?

Yes. WMS systems can form part of a broader technology environment that supports robotic warehouse automation. The specific level of integration depends on the software, robotic equipment, and control architecture selected for the facility.

Robotic automation can reduce the amount of manual transportation required in a warehouse while helping businesses move products more efficiently between operational areas.

Century Conveyor Systems offers robotic order fulfillment solutions that include Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs).

AGVs typically follow established navigation routes using technologies such as magnetic tape, QR code stickers, inductive wires, and laser grids. They are particularly useful for transporting pallets, cartons, and other items along predefined routes.

AMRs offer greater flexibility because they navigate their surroundings using sensors and programming rather than relying on fixed physical guidance paths. They can transport totes, cartons, and carts throughout a distribution facility.

Both technologies can support goods-to-person operations and other warehouse workflows.

For businesses considering robotic automation, the important question is how robots will fit into the existing warehouse environment. Software, equipment controls, transportation routes, and employee workflows must all be considered to ensure the technology contributes to the facility’s overall efficiency.

7. Are WMS systems suitable for businesses with growing fulfillment demands?

WMS systems can be valuable for businesses experiencing growth because increasing order volumes often create additional demands on warehouse space, labor, inventory management, and fulfillment processes.

A warehouse that operates efficiently at a lower volume may struggle when order activity increases. Manual processes can become harder to coordinate, employees may spend more time transporting products, and existing material handling equipment may become a bottleneck.

Businesses should therefore consider scalability when evaluating WMS systems and warehouse automation investments.

Century Conveyor Systems offers several automation solutions that can accommodate changing operational requirements.

Its robotic fulfillment solutions, for example, offer flexibility and scalability. Additional robotic systems can be implemented as needed, allowing businesses to expand their automation capabilities over time. Unlike some traditional automation equipment, mobile robots are not permanently fixed to one location.

Conveyor systems can also be designed with different sections and equipment types to accommodate specific warehouse functions.

The goal is to develop an automation strategy that addresses current operational challenges while allowing room for future growth.

Businesses should consider projected order volumes, available warehouse space, product characteristics, and expected changes in fulfillment requirements before selecting a system.

8. How can WMS systems help reduce warehouse labor costs?

Labor is one of the major expenses associated with warehouse operations. Employees are responsible for receiving products, managing inventory, picking orders, packing shipments, transporting goods, and completing numerous other tasks.

When warehouse workflows are inefficient, employees may spend significant portions of their shifts performing repetitive activities that could be supported by automation.

WMS systems help organize warehouse activities, while automated material handling technologies can reduce the physical work required to move products throughout a facility.

For example, conveyor systems can transport cartons between workstations without requiring employees to manually carry or move every package. Robotic systems can transport totes and pallets, while sortation equipment can automate the distribution of packages to designated destinations.

Century Conveyor Systems focuses on designing and implementing automation solutions that increase warehouse output while lowering labor costs.

However, reducing labor costs does not necessarily mean eliminating employees. Instead, automation can allow warehouse personnel to spend less time on repetitive transportation tasks and more time on activities that require human oversight, decision-making, and attention to detail.

For businesses facing labor shortages or increasing fulfillment demands, this can be an important operational advantage.

9. Can WMS systems be integrated into an existing warehouse?

Yes, businesses do not necessarily need to construct an entirely new warehouse to benefit from improved warehouse management and automation.

Many facilities already have conveyors, storage systems, picking stations, and other material handling equipment. However, these systems may have been installed at different times and may not operate as efficiently together as they could.

Modernization and retrofit projects can help businesses improve existing infrastructure while reducing the need for a complete facility redesign.

Century Conveyor Systems offers retrofit and modernization capabilities alongside system design, controls engineering, mechanical engineering, and installation services.

When evaluating an existing warehouse, businesses should examine which processes are creating bottlenecks and determine whether new software, equipment controls, or material handling solutions could improve performance.

For some facilities, improvements may involve updating controls or integrating additional automation equipment. Others may benefit from new conveyor sections, robotic transportation, improved storage configurations, or redesigned picking and packing areas.

The best approach depends on the condition of the existing infrastructure and the facility’s long-term operational goals.

10. What should businesses consider when choosing WMS systems?

Selecting the right WMS system requires more than comparing software features. Businesses should evaluate how the technology will support their specific warehouse operations and whether it can accommodate their future requirements.

Several important factors deserve consideration.

Warehouse size and layout: The physical configuration of a facility affects how inventory is stored, how products move, and where automation equipment can be installed.

Order volume and fulfillment requirements: Businesses handling high order volumes or complex fulfillment processes may require more extensive coordination between software and automated equipment.

Existing technology: Companies should evaluate their current warehouse software, conveyors, controls, storage systems, and other equipment before selecting additional technology.

Integration capabilities: A WMS should fit into the broader technology environment, including any WCS, conveyor controls, robotic systems, and other operational platforms.

Scalability: Businesses should consider whether their investment can accommodate increased order volumes, additional equipment, and changing fulfillment requirements.

Long-term support: Implementation is only one part of an automation project. Maintenance, replacement parts, troubleshooting, and ongoing technical assistance are also important considerations.

Century Conveyor Systems provides a range of services covering system design, controls engineering, project management, installation, startup support, and lifetime parts and service.

Considering these factors together can help businesses select an approach that delivers lasting operational value.

11. Why should businesses choose Century Conveyor Systems for warehouse automation?

Choosing a warehouse automation partner is an important decision because the success of an automation project depends on more than the equipment itself. Businesses need a partner capable of understanding their operational requirements and developing solutions that work together.

Century Conveyor Systems is a full-service material handling automation integrator serving shipping warehouses, distribution centers, and fulfillment facilities.

Its capabilities extend across several important areas of warehouse automation, including:

  • Warehouse Management Systems and Warehouse Control Systems.
  • Conveyor systems and pallet handling equipment.
  • Robotic order fulfillment and mobile robots.
  • Automated sortation systems.
  • Robotic palletizing and depalletizing.
  • Picking modules and storage systems.
  • Programmable logic controls and control panel fabrication.
  • Mechanical engineering and electrical installation.
  • Preventative maintenance, conveyor repair, and replacement parts.

Century manages projects from system design and validation through installation and startup support. This comprehensive approach helps businesses address the different technical and operational requirements involved in warehouse automation.

Rather than purchasing individual technologies without considering how they interact, companies can work toward a more unified material handling solution.

For organizations looking to improve productivity, increase fulfillment capacity, and modernize warehouse operations, this level of system integration can make a meaningful difference.

Final Thoughts: Are WMS Systems the Right Investment for Your Warehouse?

WMS systems play an important role in helping businesses organize warehouse operations, manage inventory, and support efficient order fulfillment. When combined with warehouse control technology and automated material handling equipment, they can contribute to a more productive and coordinated distribution environment.

However, the most effective warehouse automation strategy depends on the individual facility. Factors such as order volume, warehouse layout, existing infrastructure, labor requirements, and future growth expectations should all influence the decision-making process.

Century Conveyor Systems offers a comprehensive range of warehouse automation capabilities, including WMS, WCS, conveyor systems, robotic fulfillment, and sortation solutions. Its engineering and integration services help businesses develop automation strategies designed around their specific operational needs.

Whether you are planning a new distribution facility, upgrading an existing warehouse, or exploring ways to improve order fulfillment, investing in the right combination of warehouse management and automation technology can help position your operation for long-term success.

Ready to explore WMS systems and warehouse automation for your facility? Contact Century Conveyor Systems to discuss your operational requirements and start planning a customized automation solution.
Customized Storage Solutions 101: Frequently Asked Questions About Century Conveyor Systems

customized storage solutions

Warehouses and distribution centers face an ongoing challenge: finding the right customized storage solutions. As inventory grows and customer expectations change, traditional storage arrangements may no longer provide the flexibility or performance businesses need. This is where customized storage solutions become an important investment.

Century Conveyor Systems helps businesses address these challenges through engineered material handling and warehouse automation systems. From shelving and pallet racking to mezzanines, picking modules, and automated storage and retrieval systems, Century offers solutions designed to support the specific requirements of modern warehouse environments.

Rather than relying on a one-size-fits-all approach, customized storage solutions consider the products being handled, available floor space, inventory movement, employee workflows, and long-term operational goals.

Below are some frequently asked questions about Century Conveyor Systems’ customized storage solutions and how they can help businesses create more efficient, productive warehouse environments.

customized storage solutions

1. What Are Customized Storage Solutions, and Why Are They Important for Warehouse Operations?

Customized storage solutions are warehouse storage systems designed around the specific needs, inventory requirements, and operational processes of an individual facility. Instead of selecting standard shelving or racking based solely on available dimensions, businesses can implement storage configurations that accommodate their products, workflow, and space limitations.

For example, a distribution center handling large palletized products will have different storage requirements than an e-commerce fulfillment facility managing thousands of smaller individual items. A standard storage arrangement may not provide the accessibility, organization, or picking efficiency needed by both operations.

Century Conveyor Systems offers storage-related solutions that include shelving and racking, ergonomic picking and packing systems, automated storage and retrieval systems, mezzanines, platforms, and warehouse structures.

These options help businesses address several important operational considerations:

  • Available warehouse space: Storage configurations can be planned around the facility’s dimensions, ceiling height, existing equipment, and available floor space.
  • Inventory characteristics: Storage systems can accommodate different product dimensions, weights, quantities, and handling requirements.
  • Workflow efficiency: Storage arrangements can reduce unnecessary movement between inventory locations, picking stations, and packing areas.
  • Operational accessibility: Employees can access inventory through storage configurations that support the facility’s picking and replenishment processes.
  • Future requirements: Businesses can consider anticipated inventory growth and operational changes when planning their storage infrastructure.

The importance of customization comes down to making the storage environment work for the business rather than forcing the business to work around an inefficient storage arrangement.

With an appropriately engineered solution, companies can improve how inventory is organized, accessed, and moved throughout their facilities.

2. How Can Customized Storage Solutions Maximize Available Warehouse Space?

Warehouse space is a valuable operational resource. When storage systems are poorly configured, businesses can lose significant amounts of usable space to inefficient aisles, inaccessible inventory, disorganized shelving, and unnecessary floor-level storage.

Customized storage solutions help address these problems by considering how a facility’s horizontal and vertical space can be used more effectively.

Century Conveyor Systems provides storage modules that include shelving, racking, mezzanines, platforms, and warehouse structures. These options give businesses different ways to organize inventory while making better use of their existing buildings.

For instance, mezzanines can introduce additional usable levels within a warehouse, allowing companies to take advantage of vertical space. Rather than immediately expanding their building footprint, businesses may be able to accommodate additional storage or operational areas within their existing facility.

Shelving and racking systems also help organize inventory according to product characteristics and accessibility requirements. Different configurations can support palletized goods, smaller individual items, and products that need to be accessed frequently.

A customized approach also considers the relationship between storage and movement. Increasing storage density without considering picking access, replenishment, and material handling can create congestion and slow down daily operations.

The objective is not simply to fit more products into a warehouse. It is to create a storage environment that balances capacity with accessibility and productivity.

By evaluating how inventory enters, occupies, and leaves the facility, Century can help businesses develop storage configurations that make more effective use of their available space.

3. What Types of Storage Systems Does Century Conveyor Systems Offer?

Different warehouse operations require different storage arrangements. The right system depends on factors such as inventory size, product weight, storage volume, picking frequency, available space, and the degree of automation required.

Century Conveyor Systems offers several storage-related technologies and infrastructure options to help businesses meet these varying requirements.

Shelving and racking systems

Shelving and racking provide structured locations for storing inventory. They can help businesses organize products, establish consistent inventory locations, and improve access to stored materials.

These systems are particularly useful for warehouses that handle a variety of products and need clearly defined storage areas.

Ergonomic picking and packing solutions

Picking and packing operations depend heavily on how inventory is presented to employees. Storage configurations that support ergonomic workflows can help reduce unnecessary reaching, walking, and handling.

When storage and packing stations are properly coordinated, employees can retrieve products and prepare orders more efficiently.

Automated storage and retrieval systems

Automated storage and retrieval systems (AS/RS) use automated equipment and controls to store and retrieve inventory. These systems can help businesses reduce certain manual handling requirements and create more structured inventory movement.

They are particularly relevant for facilities seeking greater automation and improved control over storage and retrieval processes.

Mezzanines and platforms

Mezzanines and platforms provide additional usable levels within a facility. They can support storage areas, picking operations, and other warehouse functions, depending on the facility’s engineering and layout requirements.

Warehouse structures

Warehouse structures help establish the physical infrastructure needed to support storage and material handling operations.

The advantage of having multiple options is that businesses can select storage technologies based on their actual operational requirements rather than purchasing equipment that may not fit their processes.

4. How Do Customized Storage Solutions Improve Order Fulfillment?

Order fulfillment involves much more than retrieving an item from a shelf. It includes the entire process of receiving an order, locating inventory, picking products, transporting them through the facility, packing them, and preparing them for shipment.

Every unnecessary movement, delay, or handling error can affect the speed and accuracy of this process.

Century Conveyor Systems approaches order fulfillment as an integrated material handling operation. Its conveyor and robotic fulfillment solutions are engineered to optimize operational touchpoints, improve output performance, reduce errors that can lead to returns or product damage, and process items faster with fewer manual interactions.

Customized storage solutions contribute to this process by improving the relationship between inventory locations and order processing areas.

For example, consider an e-commerce distribution center that handles hundreds or thousands of orders daily. If frequently requested products are stored far away from picking and packing stations, employees may spend considerable time traveling throughout the warehouse.

A better-organized storage configuration can help position inventory according to operational priorities and picking requirements.

Storage systems can also work alongside conveyor equipment to create a more connected fulfillment process. Once an item is retrieved, conveyors can transport it to another processing area without requiring employees to manually carry products throughout the facility.

Century offers different conveyor technologies for these applications, including:

  • Live roller and gravity conveyors for applications such as packing lines and manual induction.
  • Belted conveyors for stable transportation of small parcels, polybags, and irregular carton sizes.
  • Modular belt conveyors for specialized product handling and applications requiring easier belt maintenance.
  • Conveyor diverts for directing cartons toward different processing destinations.
  • Zero-pressure and minimum-pressure accumulation conveyors for managing product spacing and reducing contact between items.
  • Extendable conveyors for loading and unloading operations.

Robotic fulfillment technologies, including automated guided vehicles (AGVs) and autonomous mobile robots (AMRs), can further support material movement.

When storage, picking, conveying, and automation are considered together, businesses can create a more coordinated fulfillment environment that supports faster and more accurate order processing.

5. Can Customized Storage Solutions Be Integrated With Existing Warehouse Automation?

Yes. One of the most important considerations when planning a warehouse storage project is ensuring that the new equipment works effectively with the facility’s existing infrastructure.

Businesses may already have conveyors, warehouse management software, picking stations, robotic equipment, or other material handling systems in place. Replacing everything simply to improve storage capacity may be unnecessary and expensive.

A customized approach considers how new storage infrastructure can complement the equipment and processes already operating within the facility.

Century Conveyor Systems provides material handling integration services that extend beyond storage equipment. Its capabilities include conveyor systems, robotic fulfillment, controls and software, programmable logic controls (PLC), warehouse management systems (WMS), and warehouse control systems (WCS).

This broader range of capabilities is important because storage does not operate independently from the rest of a warehouse.

For example, a business introducing additional picking modules may need to consider how retrieved products will move to packing stations. A facility installing automated storage equipment may also need to coordinate inventory movements with its existing controls and warehouse software.

Similarly, adding a mezzanine or elevated picking area may require consideration of how products will move between different facility levels.

By evaluating the complete material handling environment, businesses can avoid creating isolated storage improvements that introduce new operational bottlenecks elsewhere.

Century’s system integration capabilities allow storage projects to be considered as part of a larger warehouse automation strategy.

6. How Do Customized Storage Solutions Support Business Growth and Changing Inventory Demands?

Warehouse requirements rarely remain the same forever. Businesses experience seasonal demand, introduce new products, expand distribution networks, and adjust inventory strategies to accommodate changing customer expectations.

A storage system that works well today may become less effective as product volumes and operational requirements increase.

Customized storage solutions help businesses account for these changes by considering long-term requirements during the initial planning process.

For example, a growing distribution center may eventually need additional storage locations, more picking capacity, or increased transportation capacity between warehouse departments.

If these requirements are considered early, businesses can make more informed decisions about the storage infrastructure they install.

Century’s broader automation portfolio also includes scalable robotic fulfillment options. Its AGV and AMR solutions can support warehouse transportation requirements, with additional systems implemented as operational needs develop.

AMRs are particularly flexible because they navigate through a facility without requiring fixed tracks. They can transport totes, cartons, and carts and can support goods-to-person applications in which inventory is brought to employees at fulfillment stations.

AGVs, meanwhile, can be configured for more defined transportation routes and can handle pallets, cartons, and other products depending on their attachments and applications.

Although storage equipment and mobile robotics serve different functions, combining them can help businesses develop a more adaptable material handling environment.

The key is to plan storage capacity, inventory accessibility, and transportation requirements together. This creates a stronger foundation for accommodating future growth without unnecessarily disrupting current operations.

7. Why Is Professional Engineering Important When Designing Customized Storage Solutions?

Choosing warehouse storage equipment based on dimensions and price alone can overlook important operational considerations.

A storage configuration must account for the facility’s physical characteristics, the products being handled, employee workflows, material movement, equipment compatibility, and safety requirements.

Professional engineering helps bring these considerations together before installation begins.

Century Conveyor Systems is a full-service material handling systems integrator. Its project capabilities include system design, validation, implementation, installation, and startup support.

This turnkey approach is valuable because warehouse projects often involve multiple interconnected systems and disciplines.

For example, installing a new storage structure may require coordination with conveyors, electrical equipment, controls, and other warehouse infrastructure. Without appropriate planning, individual components may not work together as intended.

Century also provides mechanical engineering, controls engineering, electrical installation, mechanical installation, project management, and project phasing services.

These capabilities support a more organized project process, from initial planning through implementation.

Engineering also helps businesses evaluate the practical limitations of their facilities. Ceiling clearances, floor conditions, aisle dimensions, product weights, access requirements, and existing equipment all influence which storage configurations are appropriate.

Rather than selecting a system simply because it offers additional storage capacity, businesses should consider whether it will improve the overall performance of their operations.

Professional system design helps establish that connection between equipment selection and measurable warehouse objectives.

8. What Should Businesses Consider Before Investing in Customized Storage Solutions?

Before implementing a new storage system, businesses should evaluate their current warehouse operations and identify the problems they want to solve.

A successful storage project begins with understanding the facility’s existing limitations and defining what an improved operation should accomplish.

Several considerations can help guide this process.

Inventory characteristics: Businesses should understand the dimensions, weights, quantities, and handling requirements of the products they store. These characteristics influence the types of shelving, racking, and automated equipment that may be appropriate.

Available space: Facility dimensions, ceiling height, floor space, existing structures, and aisle requirements all affect storage design.

Picking and replenishment workflows: Storage locations should support the way inventory is retrieved, replenished, and transported throughout the facility.

Order volume: Businesses should consider current order volumes as well as anticipated changes in demand. This helps determine whether manual storage arrangements, automated systems, or a combination of technologies may be appropriate.

Existing equipment: Current conveyors, software, controls, and material handling systems should be evaluated to identify integration opportunities.

Long-term maintenance: Storage and automation equipment should be considered in terms of ongoing maintenance, replacement parts, and service requirements.

Future expansion: Companies should determine whether the proposed system can accommodate additional inventory, equipment, or operational capacity in the future.

Having a clear understanding of these factors makes it easier to establish project priorities and communicate requirements to a systems integrator.

Century Conveyor Systems encourages businesses to provide project details when beginning the planning process so an automation expert can respond with appropriate next steps.

The more clearly a company defines its operational challenges, the easier it becomes to develop a solution aligned with its objectives.

9. Does Century Conveyor Systems Provide Support Beyond Customized Storage Solutions Installation?

Yes. A warehouse automation investment should be viewed as a long-term operational asset rather than a one-time equipment purchase.

Even a well-designed system requires ongoing attention to maintain performance, address mechanical issues, and replace components when necessary.

Century Conveyor Systems offers services that extend beyond initial system design and installation. Its capabilities include conveyor preventative maintenance, repair services, replacement parts, mechanical installation, controls engineering, and project support.

The company also highlights lifetime parts and service as part of its turnkey integration approach.

This ongoing support is important for businesses that rely on their material handling systems to keep daily warehouse operations moving.

For example, a conveyor breakdown can interrupt the movement of products between storage, picking, packing, and shipping areas. Having access to experienced service technicians and replacement equipment can help businesses address maintenance requirements and minimize operational disruption.

Century also offers conveyor service and parts capabilities, including preventative maintenance and equipment quotations.

Its website notes more than 40 years of conveyor experience and a service department with technicians serving the New Jersey, Pennsylvania, and New York metropolitan area.

By considering service and maintenance during the initial planning process, businesses can make more informed decisions about the long-term requirements of their storage and automation investments.

10. How Can Businesses Get Started With Customized Storage Solutions From Century Conveyor Systems?

The first step is to identify the specific warehouse challenges that a customized storage system should address.

Some businesses may need to increase storage capacity because inventory is growing. Others may want to improve picking efficiency, reduce manual material handling, integrate automation, or make better use of available vertical space.

Once these objectives are established, businesses can begin evaluating potential storage configurations and how they fit into the wider material handling operation.

Century Conveyor Systems works with businesses to engineer automation solutions for warehouses, distribution centers, and fulfillment facilities.

Its approach encompasses system design, validation, implementation, installation, startup support, and ongoing parts and service.

Companies interested in customized storage solutions can begin by sharing details about their facility and operational requirements.

Useful information to prepare includes:

  • Current warehouse dimensions and layout.
  • Types of products and inventory being stored.
  • Existing shelving, racking, and material handling equipment.
  • Current picking, packing, and replenishment processes.
  • Average and peak order volumes.
  • Current operational bottlenecks.
  • Anticipated storage and fulfillment requirements.
  • Long-term business growth objectives.

These details help establish a starting point for evaluating the right combination of storage infrastructure and automation technologies.

Businesses can visit Century Conveyor Systems online at www.centuryconveyor.com or contact its team to discuss an upcoming warehouse optimization project.

Final Thoughts: Why Choose Customized Storage Solutions for Your Warehouse?

An efficient warehouse requires more than sufficient storage capacity. It needs an organized environment in which inventory can be stored, accessed, retrieved, and transported without creating unnecessary delays or operational complications.

Customized storage solutions give businesses the opportunity to address these requirements through systems designed around their facilities and workflows.

Century Conveyor Systems offers a combination of shelving and racking, ergonomic picking and packing solutions, automated storage and retrieval systems, mezzanines, platforms, and warehouse structures. Its broader material handling capabilities also include conveyors, robotic fulfillment, controls engineering, and warehouse automation integration.

This combination allows businesses to approach storage as part of a complete operational strategy rather than an isolated equipment purchase.

Whether a company wants to maximize available space, improve order fulfillment, accommodate inventory growth, or introduce more automation, the right storage configuration can make a meaningful difference in warehouse productivity.

With its turnkey engineering, integration, installation, and support capabilities, Century Conveyor Systems helps businesses take a more comprehensive approach to warehouse efficiency and customized storage solutions.

Customized Storage Solutions 101: Frequently Asked Questions About Century Conveyor Systems

customized storage solutions

Warehouses and distribution centers face an ongoing challenge: finding the right customized storage solutions. As inventory grows and customer expectations change, traditional storage arrangements may no longer provide the flexibility or performance businesses need. This is where customized storage solutions become an important investment.

Century Conveyor Systems helps businesses address these challenges through engineered material handling and warehouse automation systems. From shelving and pallet racking to mezzanines, picking modules, and automated storage and retrieval systems, Century offers solutions designed to support the specific requirements of modern warehouse environments.

Rather than relying on a one-size-fits-all approach, customized storage solutions consider the products being handled, available floor space, inventory movement, employee workflows, and long-term operational goals.

Below are some frequently asked questions about Century Conveyor Systems’ customized storage solutions and how they can help businesses create more efficient, productive warehouse environments.

customized storage solutions

1. What Are Customized Storage Solutions, and Why Are They Important for Warehouse Operations?

Customized storage solutions are warehouse storage systems designed around the specific needs, inventory requirements, and operational processes of an individual facility. Instead of selecting standard shelving or racking based solely on available dimensions, businesses can implement storage configurations that accommodate their products, workflow, and space limitations.

For example, a distribution center handling large palletized products will have different storage requirements than an e-commerce fulfillment facility managing thousands of smaller individual items. A standard storage arrangement may not provide the accessibility, organization, or picking efficiency needed by both operations.

Century Conveyor Systems offers storage-related solutions that include shelving and racking, ergonomic picking and packing systems, automated storage and retrieval systems, mezzanines, platforms, and warehouse structures.

These options help businesses address several important operational considerations:

  • Available warehouse space: Storage configurations can be planned around the facility’s dimensions, ceiling height, existing equipment, and available floor space.
  • Inventory characteristics: Storage systems can accommodate different product dimensions, weights, quantities, and handling requirements.
  • Workflow efficiency: Storage arrangements can reduce unnecessary movement between inventory locations, picking stations, and packing areas.
  • Operational accessibility: Employees can access inventory through storage configurations that support the facility’s picking and replenishment processes.
  • Future requirements: Businesses can consider anticipated inventory growth and operational changes when planning their storage infrastructure.

The importance of customization comes down to making the storage environment work for the business rather than forcing the business to work around an inefficient storage arrangement.

With an appropriately engineered solution, companies can improve how inventory is organized, accessed, and moved throughout their facilities.

2. How Can Customized Storage Solutions Maximize Available Warehouse Space?

Warehouse space is a valuable operational resource. When storage systems are poorly configured, businesses can lose significant amounts of usable space to inefficient aisles, inaccessible inventory, disorganized shelving, and unnecessary floor-level storage.

Customized storage solutions help address these problems by considering how a facility’s horizontal and vertical space can be used more effectively.

Century Conveyor Systems provides storage modules that include shelving, racking, mezzanines, platforms, and warehouse structures. These options give businesses different ways to organize inventory while making better use of their existing buildings.

For instance, mezzanines can introduce additional usable levels within a warehouse, allowing companies to take advantage of vertical space. Rather than immediately expanding their building footprint, businesses may be able to accommodate additional storage or operational areas within their existing facility.

Shelving and racking systems also help organize inventory according to product characteristics and accessibility requirements. Different configurations can support palletized goods, smaller individual items, and products that need to be accessed frequently.

A customized approach also considers the relationship between storage and movement. Increasing storage density without considering picking access, replenishment, and material handling can create congestion and slow down daily operations.

The objective is not simply to fit more products into a warehouse. It is to create a storage environment that balances capacity with accessibility and productivity.

By evaluating how inventory enters, occupies, and leaves the facility, Century can help businesses develop storage configurations that make more effective use of their available space.

3. What Types of Storage Systems Does Century Conveyor Systems Offer?

Different warehouse operations require different storage arrangements. The right system depends on factors such as inventory size, product weight, storage volume, picking frequency, available space, and the degree of automation required.

Century Conveyor Systems offers several storage-related technologies and infrastructure options to help businesses meet these varying requirements.

Shelving and racking systems

Shelving and racking provide structured locations for storing inventory. They can help businesses organize products, establish consistent inventory locations, and improve access to stored materials.

These systems are particularly useful for warehouses that handle a variety of products and need clearly defined storage areas.

Ergonomic picking and packing solutions

Picking and packing operations depend heavily on how inventory is presented to employees. Storage configurations that support ergonomic workflows can help reduce unnecessary reaching, walking, and handling.

When storage and packing stations are properly coordinated, employees can retrieve products and prepare orders more efficiently.

Automated storage and retrieval systems

Automated storage and retrieval systems (AS/RS) use automated equipment and controls to store and retrieve inventory. These systems can help businesses reduce certain manual handling requirements and create more structured inventory movement.

They are particularly relevant for facilities seeking greater automation and improved control over storage and retrieval processes.

Mezzanines and platforms

Mezzanines and platforms provide additional usable levels within a facility. They can support storage areas, picking operations, and other warehouse functions, depending on the facility’s engineering and layout requirements.

Warehouse structures

Warehouse structures help establish the physical infrastructure needed to support storage and material handling operations.

The advantage of having multiple options is that businesses can select storage technologies based on their actual operational requirements rather than purchasing equipment that may not fit their processes.

4. How Do Customized Storage Solutions Improve Order Fulfillment?

Order fulfillment involves much more than retrieving an item from a shelf. It includes the entire process of receiving an order, locating inventory, picking products, transporting them through the facility, packing them, and preparing them for shipment.

Every unnecessary movement, delay, or handling error can affect the speed and accuracy of this process.

Century Conveyor Systems approaches order fulfillment as an integrated material handling operation. Its conveyor and robotic fulfillment solutions are engineered to optimize operational touchpoints, improve output performance, reduce errors that can lead to returns or product damage, and process items faster with fewer manual interactions.

Customized storage solutions contribute to this process by improving the relationship between inventory locations and order processing areas.

For example, consider an e-commerce distribution center that handles hundreds or thousands of orders daily. If frequently requested products are stored far away from picking and packing stations, employees may spend considerable time traveling throughout the warehouse.

A better-organized storage configuration can help position inventory according to operational priorities and picking requirements.

Storage systems can also work alongside conveyor equipment to create a more connected fulfillment process. Once an item is retrieved, conveyors can transport it to another processing area without requiring employees to manually carry products throughout the facility.

Century offers different conveyor technologies for these applications, including:

  • Live roller and gravity conveyors for applications such as packing lines and manual induction.
  • Belted conveyors for stable transportation of small parcels, polybags, and irregular carton sizes.
  • Modular belt conveyors for specialized product handling and applications requiring easier belt maintenance.
  • Conveyor diverts for directing cartons toward different processing destinations.
  • Zero-pressure and minimum-pressure accumulation conveyors for managing product spacing and reducing contact between items.
  • Extendable conveyors for loading and unloading operations.

Robotic fulfillment technologies, including automated guided vehicles (AGVs) and autonomous mobile robots (AMRs), can further support material movement.

When storage, picking, conveying, and automation are considered together, businesses can create a more coordinated fulfillment environment that supports faster and more accurate order processing.

5. Can Customized Storage Solutions Be Integrated With Existing Warehouse Automation?

Yes. One of the most important considerations when planning a warehouse storage project is ensuring that the new equipment works effectively with the facility’s existing infrastructure.

Businesses may already have conveyors, warehouse management software, picking stations, robotic equipment, or other material handling systems in place. Replacing everything simply to improve storage capacity may be unnecessary and expensive.

A customized approach considers how new storage infrastructure can complement the equipment and processes already operating within the facility.

Century Conveyor Systems provides material handling integration services that extend beyond storage equipment. Its capabilities include conveyor systems, robotic fulfillment, controls and software, programmable logic controls (PLC), warehouse management systems (WMS), and warehouse control systems (WCS).

This broader range of capabilities is important because storage does not operate independently from the rest of a warehouse.

For example, a business introducing additional picking modules may need to consider how retrieved products will move to packing stations. A facility installing automated storage equipment may also need to coordinate inventory movements with its existing controls and warehouse software.

Similarly, adding a mezzanine or elevated picking area may require consideration of how products will move between different facility levels.

By evaluating the complete material handling environment, businesses can avoid creating isolated storage improvements that introduce new operational bottlenecks elsewhere.

Century’s system integration capabilities allow storage projects to be considered as part of a larger warehouse automation strategy.

6. How Do Customized Storage Solutions Support Business Growth and Changing Inventory Demands?

Warehouse requirements rarely remain the same forever. Businesses experience seasonal demand, introduce new products, expand distribution networks, and adjust inventory strategies to accommodate changing customer expectations.

A storage system that works well today may become less effective as product volumes and operational requirements increase.

Customized storage solutions help businesses account for these changes by considering long-term requirements during the initial planning process.

For example, a growing distribution center may eventually need additional storage locations, more picking capacity, or increased transportation capacity between warehouse departments.

If these requirements are considered early, businesses can make more informed decisions about the storage infrastructure they install.

Century’s broader automation portfolio also includes scalable robotic fulfillment options. Its AGV and AMR solutions can support warehouse transportation requirements, with additional systems implemented as operational needs develop.

AMRs are particularly flexible because they navigate through a facility without requiring fixed tracks. They can transport totes, cartons, and carts and can support goods-to-person applications in which inventory is brought to employees at fulfillment stations.

AGVs, meanwhile, can be configured for more defined transportation routes and can handle pallets, cartons, and other products depending on their attachments and applications.

Although storage equipment and mobile robotics serve different functions, combining them can help businesses develop a more adaptable material handling environment.

The key is to plan storage capacity, inventory accessibility, and transportation requirements together. This creates a stronger foundation for accommodating future growth without unnecessarily disrupting current operations.

7. Why Is Professional Engineering Important When Designing Customized Storage Solutions?

Choosing warehouse storage equipment based on dimensions and price alone can overlook important operational considerations.

A storage configuration must account for the facility’s physical characteristics, the products being handled, employee workflows, material movement, equipment compatibility, and safety requirements.

Professional engineering helps bring these considerations together before installation begins.

Century Conveyor Systems is a full-service material handling systems integrator. Its project capabilities include system design, validation, implementation, installation, and startup support.

This turnkey approach is valuable because warehouse projects often involve multiple interconnected systems and disciplines.

For example, installing a new storage structure may require coordination with conveyors, electrical equipment, controls, and other warehouse infrastructure. Without appropriate planning, individual components may not work together as intended.

Century also provides mechanical engineering, controls engineering, electrical installation, mechanical installation, project management, and project phasing services.

These capabilities support a more organized project process, from initial planning through implementation.

Engineering also helps businesses evaluate the practical limitations of their facilities. Ceiling clearances, floor conditions, aisle dimensions, product weights, access requirements, and existing equipment all influence which storage configurations are appropriate.

Rather than selecting a system simply because it offers additional storage capacity, businesses should consider whether it will improve the overall performance of their operations.

Professional system design helps establish that connection between equipment selection and measurable warehouse objectives.

8. What Should Businesses Consider Before Investing in Customized Storage Solutions?

Before implementing a new storage system, businesses should evaluate their current warehouse operations and identify the problems they want to solve.

A successful storage project begins with understanding the facility’s existing limitations and defining what an improved operation should accomplish.

Several considerations can help guide this process.

Inventory characteristics: Businesses should understand the dimensions, weights, quantities, and handling requirements of the products they store. These characteristics influence the types of shelving, racking, and automated equipment that may be appropriate.

Available space: Facility dimensions, ceiling height, floor space, existing structures, and aisle requirements all affect storage design.

Picking and replenishment workflows: Storage locations should support the way inventory is retrieved, replenished, and transported throughout the facility.

Order volume: Businesses should consider current order volumes as well as anticipated changes in demand. This helps determine whether manual storage arrangements, automated systems, or a combination of technologies may be appropriate.

Existing equipment: Current conveyors, software, controls, and material handling systems should be evaluated to identify integration opportunities.

Long-term maintenance: Storage and automation equipment should be considered in terms of ongoing maintenance, replacement parts, and service requirements.

Future expansion: Companies should determine whether the proposed system can accommodate additional inventory, equipment, or operational capacity in the future.

Having a clear understanding of these factors makes it easier to establish project priorities and communicate requirements to a systems integrator.

Century Conveyor Systems encourages businesses to provide project details when beginning the planning process so an automation expert can respond with appropriate next steps.

The more clearly a company defines its operational challenges, the easier it becomes to develop a solution aligned with its objectives.

9. Does Century Conveyor Systems Provide Support Beyond Customized Storage Solutions Installation?

Yes. A warehouse automation investment should be viewed as a long-term operational asset rather than a one-time equipment purchase.

Even a well-designed system requires ongoing attention to maintain performance, address mechanical issues, and replace components when necessary.

Century Conveyor Systems offers services that extend beyond initial system design and installation. Its capabilities include conveyor preventative maintenance, repair services, replacement parts, mechanical installation, controls engineering, and project support.

The company also highlights lifetime parts and service as part of its turnkey integration approach.

This ongoing support is important for businesses that rely on their material handling systems to keep daily warehouse operations moving.

For example, a conveyor breakdown can interrupt the movement of products between storage, picking, packing, and shipping areas. Having access to experienced service technicians and replacement equipment can help businesses address maintenance requirements and minimize operational disruption.

Century also offers conveyor service and parts capabilities, including preventative maintenance and equipment quotations.

Its website notes more than 40 years of conveyor experience and a service department with technicians serving the New Jersey, Pennsylvania, and New York metropolitan area.

By considering service and maintenance during the initial planning process, businesses can make more informed decisions about the long-term requirements of their storage and automation investments.

10. How Can Businesses Get Started With Customized Storage Solutions From Century Conveyor Systems?

The first step is to identify the specific warehouse challenges that a customized storage system should address.

Some businesses may need to increase storage capacity because inventory is growing. Others may want to improve picking efficiency, reduce manual material handling, integrate automation, or make better use of available vertical space.

Once these objectives are established, businesses can begin evaluating potential storage configurations and how they fit into the wider material handling operation.

Century Conveyor Systems works with businesses to engineer automation solutions for warehouses, distribution centers, and fulfillment facilities.

Its approach encompasses system design, validation, implementation, installation, startup support, and ongoing parts and service.

Companies interested in customized storage solutions can begin by sharing details about their facility and operational requirements.

Useful information to prepare includes:

  • Current warehouse dimensions and layout.
  • Types of products and inventory being stored.
  • Existing shelving, racking, and material handling equipment.
  • Current picking, packing, and replenishment processes.
  • Average and peak order volumes.
  • Current operational bottlenecks.
  • Anticipated storage and fulfillment requirements.
  • Long-term business growth objectives.

These details help establish a starting point for evaluating the right combination of storage infrastructure and automation technologies.

Businesses can visit Century Conveyor Systems online at www.centuryconveyor.com or contact its team to discuss an upcoming warehouse optimization project.

Final Thoughts: Why Choose Customized Storage Solutions for Your Warehouse?

An efficient warehouse requires more than sufficient storage capacity. It needs an organized environment in which inventory can be stored, accessed, retrieved, and transported without creating unnecessary delays or operational complications.

Customized storage solutions give businesses the opportunity to address these requirements through systems designed around their facilities and workflows.

Century Conveyor Systems offers a combination of shelving and racking, ergonomic picking and packing solutions, automated storage and retrieval systems, mezzanines, platforms, and warehouse structures. Its broader material handling capabilities also include conveyors, robotic fulfillment, controls engineering, and warehouse automation integration.

This combination allows businesses to approach storage as part of a complete operational strategy rather than an isolated equipment purchase.

Whether a company wants to maximize available space, improve order fulfillment, accommodate inventory growth, or introduce more automation, the right storage configuration can make a meaningful difference in warehouse productivity.

With its turnkey engineering, integration, installation, and support capabilities, Century Conveyor Systems helps businesses take a more comprehensive approach to warehouse efficiency and customized storage solutions.

Warehouse Fulfillment 101: Frequently Asked Questions About Century Conveyor Systems’s Amazing Services

warehouse fulfillment

Warehouse fulfillment is a critical part of modern supply chain operations. As customer expectations for faster deliveries, accurate orders, and reliable shipping continue to grow, warehouses and distribution centers must find ways to improve productivity without continually increasing labor costs. Efficient warehouse fulfillment requires more than simply picking products and preparing packages. It involves coordinating inventory movement, order processing, sorting, packing, and shipping through a well-designed material handling system.

Century Conveyor Systems helps businesses improve warehouse fulfillment through engineered conveyor systems, robotic automation, material handling equipment, and integrated warehouse technologies. By designing solutions around the specific needs of each facility, Century helps warehouses increase throughput, reduce unnecessary manual handling, and create more efficient fulfillment operations.

Below are some frequently asked questions about Century Conveyor Systems and its approach to warehouse fulfillment.

warehouse fulfillment

1. What Is Warehouse Fulfillment, and How Does Century Conveyor Systems Improve the Process?

Warehouse fulfillment refers to the complete process of receiving, processing, picking, packing, sorting, and preparing customer orders for shipment. It begins when an order enters the fulfillment operation and continues until the products reach the shipping area, where they are loaded for delivery.

Every step must work together to ensure orders are processed accurately and efficiently. When a warehouse relies heavily on manual transportation, repetitive handling, or disconnected processes, bottlenecks can develop. These inefficiencies can slow down order processing, increase labor requirements, and create opportunities for shipping errors.

Century Conveyor Systems addresses these challenges by engineering automated material handling solutions that connect different stages of warehouse fulfillment. Its solutions include conveyor systems, robotic fulfillment equipment, sortation systems, warehouse controls, and storage modules.

Rather than treating each piece of equipment as an isolated improvement, Century approaches warehouse automation as an integrated operation. Its engineers design, validate, and implement systems that support the movement of products throughout the facility.

This approach helps businesses improve productivity at multiple points in the fulfillment process. Products can move between workstations with fewer manual transfers, orders can be directed toward the appropriate processing areas, and warehouse employees can focus on tasks that require more direct involvement.

The ultimate objective is to create a warehouse fulfillment operation that processes more orders while minimizing unnecessary labor, handling, and operational delays.

2. Why Are Conveyor Systems Important for Warehouse Fulfillment?

Conveyor systems are one of the most important components of an automated warehouse fulfillment operation because they provide a consistent way to transport products throughout a facility.

Without an effective transportation system, employees may need to move cartons, totes, and pallets manually between picking, packing, sorting, and shipping areas. This can consume valuable labor hours and create unnecessary travel throughout the warehouse.

Century Conveyor Systems engineers conveyor solutions designed to match the layout, product characteristics, and processing requirements of individual facilities.

Depending on the application, a conveyor system can transport small parcels, irregular cartons, heavy products, or full pallets. Different conveyor sections can also perform specific functions, including accumulation, product transfers, diverting, and elevation changes.

One important advantage of conveyor automation is its ability to create a continuous flow of products. Instead of relying on employees to transport every item between workstations, conveyors move products along predetermined routes.

Century offers several conveyor technologies for different warehouse fulfillment applications, including:

  • Live roller conveyors: Powered roller conveyors that move cartons through packing lines, divert areas, and end-of-line operations.
  • Gravity conveyors: Non-powered conveyors that use gravity to move products, making them useful for staging and manual handling applications.
  • Belt conveyors: Provide stable transportation for small parcels, polybags, and irregularly sized cartons.
  • Modular belt conveyors: Feature removable belt sections that can simplify cleaning, maintenance, and modifications.
  • Pallet conveyors: Provide durable transportation for pallets and heavier loads.
  • Extendable conveyors: Extend directly into trailers to help move packages toward loading associates.

Selecting the appropriate conveyor technology allows businesses to create a transportation system that supports their specific fulfillment requirements.

3. How Can Warehouse Automation Reduce Labor Costs?

Labor is one of the most significant operational expenses for many warehouses and distribution centers. As fulfillment volumes increase, businesses often need additional employees to transport products, move materials, sort packages, and complete repetitive handling tasks.

However, adding more employees does not necessarily solve the underlying inefficiencies in a warehouse. If workers spend a considerable amount of time walking between stations or moving products manually, productivity can remain limited.

Warehouse automation helps address this problem by reducing the amount of repetitive manual work required to process orders.

Century Conveyor Systems focuses on designing systems that allow products to move efficiently between different stages of the fulfillment process. Conveyor equipment can automate transportation, while robotic systems can assist with moving cartons, totes, and pallets.

For example, an automated conveyor network can transport packages from packing stations to sorting equipment without requiring employees to manually move each carton. Similarly, automated mobile robots can retrieve products or transport materials between designated areas.

These improvements allow employees to spend more time on activities that require decision-making, quality control, and direct supervision.

The goal is not necessarily to eliminate employees from warehouse operations. Instead, it is to make better use of available labor by reducing repetitive transportation and handling responsibilities.

For facilities experiencing labor shortages, rising labor expenses, or increasing order volumes, this can be an important component of a long-term warehouse fulfillment strategy.

4. What Role Do Robotics Play in Century Conveyor Systems’ Warehouse Fulfillment Solutions?

Robotics provide another layer of automation that can improve warehouse fulfillment by handling transportation activities that would otherwise require manual equipment or employee involvement.

Century Conveyor Systems offers robotic fulfillment solutions using two primary technologies: Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs).

Although both technologies transport materials throughout a facility, they operate differently and serve different applications.

Automated Guided Vehicles (AGVs) follow established navigation paths using technologies such as magnetic tape, QR codes, inductive wires, and laser grids. They are particularly useful for predictable transportation requirements involving pallets, cartons, and other materials.

AGVs can also be equipped with carts or conveyor attachments to accommodate different types of products. They are often integrated with conveyor systems to support transportation between automated and manual processing areas.

Autonomous Mobile Robots (AMRs) offer greater navigation flexibility. Rather than following a fixed physical route, AMRs use sensors and programming to navigate throughout a facility.

This flexibility makes them particularly useful for goods-to-person operations. An AMR can retrieve a tote or container and transport it to a packing line or fulfillment employee, reducing the need for workers to travel throughout the warehouse searching for inventory.

Robotic automation also provides scalability. Businesses can introduce additional robots as fulfillment requirements change rather than committing to a completely fixed transportation infrastructure.

For warehouses seeking greater flexibility, robotics can complement conveyor automation and create a more adaptable fulfillment environment.

5. How Does Century Conveyor Systems Help Improve Order Accuracy and Reduce Product Damage?

Order accuracy and product condition are essential parts of warehouse fulfillment. Shipping the wrong product, sending an incomplete order, or damaging merchandise during transportation can lead to returns, additional expenses, and dissatisfied customers.

Many fulfillment problems originate from inefficient material handling processes. Products may be transferred between workstations multiple times, handled unnecessarily, or transported through poorly designed accumulation areas.

Century Conveyor Systems addresses these challenges through equipment designed to improve product movement and reduce unnecessary handling.

For example, conveyor diverts can automatically direct cartons toward their appropriate destinations. This reduces the need for employees to manually reposition every package as it moves through the facility.

Accumulation conveyors can also help protect products during transportation. Century offers zero-pressure and minimum-pressure accumulation solutions that use sensors and controlled spacing to manage how products move along a conveyor.

Zero-pressure accumulation prevents products from touching one another, while minimum-pressure accumulation allows products to make light contact. These technologies are particularly useful when handling fragile merchandise or products that could be damaged by excessive contact.

Belt conveyors provide another advantage by offering stable transportation for smaller parcels, polybags, and irregularly shaped cartons.

By combining appropriate conveyor equipment, automated routing, and controlled product movement, warehouses can create fulfillment processes that reduce avoidable handling errors and product damage.

6. Can Century Conveyor Systems Design a Warehouse Fulfillment System Around an Existing Facility?

Yes. Warehouse automation should reflect the physical characteristics and operational requirements of the facility where it will be installed.

Every warehouse has different constraints, including available floor space, ceiling height, product dimensions, shipping volumes, existing equipment, and employee workflows. A standardized system may not address these requirements effectively.

Century Conveyor Systems provides system design and engineering services to develop material handling solutions around individual warehouse operations.

Its approach includes evaluating the facility, determining the appropriate equipment, validating system designs, and managing implementation.

For example, a warehouse with limited floor space may benefit from vertical transportation solutions such as spiral conveyors. These systems move products between different facility levels using a compact spiral configuration.

A facility with extensive pallet transportation requirements may need a combination of pallet gravity conveyors, chain-driven live roller conveyors, and pallet drag chain systems.

Meanwhile, a fulfillment center handling smaller parcels may benefit from belt conveyors, roller conveyors, and automated sortation equipment.

The important consideration is how the equipment works together. A successful warehouse fulfillment system should support the movement of products from one operational stage to the next without creating unnecessary congestion or inefficient work patterns.

By engineering solutions around existing facility requirements, Century helps businesses pursue automation without assuming that every warehouse needs the same equipment configuration.

7. What Is the Difference Between Conveyor Automation and Robotic Fulfillment?

Conveyor automation and robotic fulfillment both improve warehouse productivity, but they solve different material handling challenges.

Conveyor systems typically move products along established transportation paths. They are particularly effective when products need to travel between predictable locations, such as packing stations, sorting equipment, accumulation areas, and shipping docks.

Robotic fulfillment equipment provides more flexible transportation capabilities. AGVs and AMRs can move products, totes, and pallets through warehouse environments without requiring every transportation route to be built into a fixed conveyor network.

The main difference is how products are transported.

Conveyors provide continuous movement along an engineered pathway, while mobile robots offer point-to-point transportation and greater flexibility when navigating changing warehouse environments.

Neither technology is automatically the better choice for every application.

A high-volume distribution center may benefit from conveyors because they can continuously transport large quantities of products through established processing areas. Another facility may benefit more from AMRs because its inventory movement requirements involve multiple destinations and changing transportation needs.

In many cases, combining both technologies produces the most effective result.

Century Conveyor Systems offers conveyor and robotic fulfillment solutions that can work together as part of a broader warehouse automation strategy.

8. How Does Century Conveyor Systems Support Different Types of Products and Order Volumes?

Warehouses rarely handle only one type of product. Depending on the industry, a fulfillment operation may process small polybags, standard cartons, irregular packages, drums, oversized products, or heavy pallets.

Each product category creates different material handling requirements.

Small packages may require stable belt transportation, while heavier products may need roller conveyors or specialized pallet handling equipment. Fragile items may require controlled accumulation to prevent products from colliding during transportation.

Century Conveyor Systems offers different equipment configurations to accommodate these varying requirements.

For example, modular belt conveyors are useful for applications that require specialized belt characteristics, easy cleaning, or simplified maintenance. Live roller conveyors provide powered transportation for cartons, while gravity conveyors can support staging and manual processing areas.

For larger loads, pallet conveyors provide stable transportation based on the weight and characteristics of the materials being handled.

System flexibility also matters when order volumes fluctuate. A warehouse may experience significant seasonal demand, promotional surges, or long-term business growth.

An appropriately engineered warehouse fulfillment system should account for these changes. Businesses can benefit from selecting equipment that supports current operations while allowing opportunities for future expansion.

Century’s robotic fulfillment solutions also offer scalability, allowing additional mobile robots to be introduced as operational requirements increase.

9. Does Century Conveyor Systems Provide Warehouse Controls and Software Integration?

Yes. Warehouse automation requires more than physical equipment. Controls and software help coordinate the movement of products and ensure that different components of an automated system operate together.

Century Conveyor Systems provides controls and software solutions that include control panel fabrication, Programmable Logic Controls (PLC), Warehouse Management Systems (WMS), and Warehouse Control Systems (WCS).

These technologies support the coordination of warehouse equipment and operational processes.

Programmable Logic Controls help manage equipment behavior, including conveyor movement, sensors, product transfers, and automated sequences.

Warehouse Management Systems support broader warehouse activities, including inventory management and order processing.

Warehouse Control Systems help coordinate automated material handling equipment and direct product movement throughout the facility.

Integrating the appropriate controls and software is important because disconnected systems can create operational inefficiencies. Equipment may function independently while failing to support the overall movement of products through the warehouse.

A properly designed automation solution considers both the mechanical equipment and the controls responsible for coordinating its operation.

For businesses investing in warehouse fulfillment automation, this integrated approach can help establish a more consistent and manageable operation.

10. How Does Preventative Maintenance Affect Warehouse Fulfillment Performance?

Even a well-designed warehouse automation system requires regular maintenance to maintain reliable performance.

Conveyor breakdowns, worn components, electrical problems, and equipment malfunctions can interrupt product movement and create bottlenecks throughout a fulfillment operation.

Because conveyor systems often connect multiple warehouse processes, a problem in one section can affect several downstream operations.

Preventative maintenance helps reduce the likelihood of unexpected equipment failures by identifying potential problems before they develop into major disruptions.

Century Conveyor Systems offers conveyor preventative maintenance, repair services, replacement parts, and ongoing support.

Its service capabilities include mechanical and electrical installation, conveyor repairs, and maintenance programs designed to support material handling equipment.

Century also provides 24/7 support services and parts assistance for conveyor systems.

The company highlights more than 40 years of conveyor experience and maintains a service department with technicians serving the New Jersey, Pennsylvania, and New York metropolitan area.

Maintenance should be considered during the initial planning of a warehouse fulfillment project rather than treated as an afterthought. Equipment accessibility, replacement components, and service requirements can all influence the long-term performance of an automated system.

A proactive maintenance strategy helps businesses protect their automation investment and maintain consistent warehouse operations.

11. Can Century Conveyor Systems Help a Warehouse Expand Its Automation Capabilities Over Time?

Yes. Warehouse automation does not always need to happen as one large installation.

Many businesses prefer to introduce automation in phases, particularly when they need to maintain existing operations during implementation or manage capital expenditures carefully.

Century Conveyor Systems offers project management, system design, project phasing, and installation services that support warehouse automation projects.

A phased approach allows businesses to prioritize the areas experiencing the greatest operational challenges.

For example, a distribution center might begin by automating transportation between packing stations and shipping areas. Once that system is operating effectively, the business may introduce additional sortation equipment or robotic transportation.

Another facility may prioritize pallet movement before investing in smaller-package fulfillment automation.

The advantage of this approach is that businesses can address immediate operational needs while planning for future improvements.

However, future expansion should be considered during the initial system design. Equipment placement, available floor space, control architecture, and transportation pathways can all affect how easily additional automation can be introduced.

Century’s scalable conveyor and robotic fulfillment solutions provide opportunities for businesses to develop their automation capabilities as their operational needs evolve.

12. Why Choose Century Conveyor Systems for Warehouse Fulfillment Automation?

Choosing an automation partner is an important decision because warehouse fulfillment equipment affects productivity, labor requirements, shipping performance, and long-term operating costs.

Century Conveyor Systems positions itself as a full-service material handling automation integrator for warehouses, distribution centers, and fulfillment facilities.

One of its main advantages is its ability to support multiple aspects of an automation project through a single provider.

Rather than focusing exclusively on conveyor installation, Century offers a broader range of capabilities, including:

  • System engineering: Designing material handling solutions around warehouse layouts, product characteristics, and operational requirements.
  • Conveyor automation: Providing belt, roller, pallet, extendable, and specialized conveyor systems.
  • Robotic fulfillment: Integrating AGVs and AMRs for automated transportation and goods-to-person applications.
  • Sortation solutions: Helping warehouses direct packages toward appropriate processing and shipping destinations.
  • Controls engineering: Providing PLC systems, control panels, and warehouse software integration.
  • Storage solutions: Offering shelving, racking, picking modules, mezzanines, and automated storage solutions.
  • Project management: Coordinating project design, validation, installation, and implementation.
  • Maintenance and service: Supporting conveyor equipment through repairs, preventative maintenance, and replacement parts.

This range of capabilities allows Century to consider the entire warehouse fulfillment process when developing an automation strategy.

The company also emphasizes a turnkey project approach, managing activities from system design and validation through installation and start-up support.

For businesses looking to improve fulfillment performance, working with an integrator that understands both individual equipment and the larger material handling system can make a meaningful difference.

Final Thoughts: Improving Warehouse Fulfillment With Century Conveyor Systems

Warehouse fulfillment is becoming increasingly demanding as businesses work to process orders faster, manage labor expenses, and maintain reliable shipping operations. Improving performance requires more than adding individual pieces of equipment. It requires an integrated approach to material handling, transportation, automation, and warehouse controls.

Century Conveyor Systems provides engineered warehouse fulfillment solutions that combine conveyor technology, robotic automation, sortation equipment, controls, and ongoing service capabilities.

Whether a facility needs to automate carton transportation, improve pallet handling, introduce goods-to-person robotics, or modernize an existing conveyor system, the right automation strategy starts with understanding the specific challenges within the operation.

By designing systems around individual warehouse requirements and considering opportunities for future expansion, Century helps businesses build more efficient material handling operations.

For organizations evaluating their next warehouse fulfillment project, Century Conveyor Systems offers an opportunity to work with an experienced automation integrator focused on improving warehouse performance from design through implementation and ongoing support.

Warehousing Services 101: Frequently Asked Questions About Century Conveyor Systems’s Amazing Services

warehousing services

Warehousing services play an essential role in helping businesses store, move, process, and distribute products efficiently. As order volumes increase and customer expectations for fast delivery continue to rise, warehouses and distribution centers must find ways to improve productivity without unnecessarily increasing labor costs or operational complexity. Material handling automation, conveyor systems, robotic fulfillment, and integrated warehouse controls can all contribute to a more streamlined operation.

Century Conveyor Systems provides engineered material handling automation solutions for warehouses, distribution centers, and fulfillment facilities. Its capabilities include conveyor systems, robotic fulfillment, sortation equipment, storage modules, warehouse controls, and ongoing conveyor maintenance and service. Rather than treating warehouse equipment as isolated components, Century focuses on designing and implementing integrated systems that support the movement of goods throughout a facility.

The following frequently asked questions explain how Century Conveyor Systems approaches warehousing services, what its solutions can accomplish, and how businesses can determine which warehouse automation capabilities best fit their operational needs.

warehousing services

1. What are warehousing services, and how does Century Conveyor Systems support warehouse operations?

Warehousing services encompass the processes, equipment, and operational capabilities required to receive, store, handle, process, and distribute inventory. Depending on the facility, these activities may include unloading incoming shipments, transporting products between workstations, storing pallets or cartons, picking orders, packing packages, sorting shipments, and preparing goods for dispatch.

However, effective warehousing involves more than having sufficient storage space. The way products move through a building can influence productivity, labor requirements, order accuracy, and the facility’s ability to meet shipping deadlines. Bottlenecks in one area can affect every subsequent step, making it important to evaluate the warehouse as a connected operation.

Century Conveyor Systems supports these requirements through material handling automation and system integration. Its engineers design, validate, and implement turnkey systems intended to improve warehouse output and reduce labor costs through automation. The company also manages project activities ranging from initial system design to implementation, installation, startup support, and ongoing parts and service.

Its capabilities cover several essential warehouse functions:

  • Conveyor transportation: Belt, roller, and pallet conveyor systems move products through designated processing and distribution routes.
  • Order fulfillment: Integrated material handling solutions help coordinate the movement of items from order processing through packing and shipping.
  • Sortation and distribution: Automated equipment directs packages toward the appropriate destinations or shipping lanes.
  • Robotic material handling: Automated guided vehicles and autonomous mobile robots transport goods through suitable warehouse environments.
  • Storage and picking infrastructure: Shelving, racking, mezzanines, platforms, and other storage modules support organized inventory handling.
  • Warehouse controls and software: Programmable logic controllers and warehouse control solutions help coordinate equipment and material movement.
  • Maintenance and replacement parts: Preventative maintenance, repairs, and parts support help businesses maintain their conveyor equipment.

These capabilities allow businesses to explore improvements across multiple stages of warehouse operations. The appropriate combination depends on existing infrastructure, product characteristics, order volume, available floor space, and long-term growth plans.

2. How can Century Conveyor Systems’ warehousing services improve order fulfillment efficiency?

Order fulfillment is one of the most important areas to evaluate when improving warehouse performance. It involves the activities that take place after an order is received and before the shipment reaches the shipping dock. Depending on the business, this process may include retrieving inventory, picking individual items or complete cases, consolidating products, packing orders, sorting packages, and moving shipments to their appropriate destinations.

When these activities rely heavily on manual transportation, employees may spend substantial time moving products between workstations rather than performing tasks that require direct attention. Congested aisles, poorly coordinated handoffs, and inefficient packing or shipping arrangements can further slow the process.

Century Conveyor Systems engineers order fulfillment solutions designed to improve throughput, reduce errors that can contribute to returns or product damage, and process items faster with fewer manual interactions.

Conveyor automation is one way to achieve these objectives. A carefully designed conveyor network can establish consistent transportation routes between picking, packing, accumulation, sortation, and shipping areas. Instead of repeatedly moving cartons by hand, employees can focus on picking accuracy, inspection, packing quality, and exception handling.

The specific conveyor technology matters, too. Live roller and gravity conveyors can support packing lines, manual induction points, and end-of-line operations. Belt conveyors can provide stable movement for smaller packages, polybags, and irregularly sized cartons. Divert mechanisms can route packages from a primary line to different destinations, while accumulation conveyors can regulate spacing between products.

Robotic solutions offer another option. Automated guided vehicles (AGVs) can transport pallets, cartons, and other loads along established routes. Autonomous mobile robots (AMRs) can navigate more flexibly through a facility, including in applications where mobile robots bring totes or products to order fulfillment personnel.

By connecting these technologies appropriately, a warehouse can reduce unnecessary handling, improve the consistency of product movement, and make better use of its available workforce.

The goal is not simply to move more packages. It is to create a coordinated fulfillment process that supports reliable shipping performance while accommodating the actual requirements of the business.

3. What types of warehouse conveyor systems are available through Century Conveyor Systems’ warehousing services?

Different products and operational environments require different transportation methods. A conveyor that works well for standard shipping cartons may not be suitable for small polybags, fragile merchandise, heavy pallets, or oversized loads. Choosing the right configuration requires considering product dimensions, weight, stability, throughput requirements, and the layout of the facility.

Century Conveyor Systems offers several conveyor technologies that address different material handling applications.

Live roller and gravity conveyors are useful for packing lines, manual induction areas, divert points, and end-of-line operations. Powered live roller conveyors use motors to move products, while gravity conveyors rely on gravity to advance items along an appropriately configured path. These systems can support operations that require practical integration between manual workstations and automated transportation.

Belt conveyors provide a continuous conveying surface that can improve stability when handling smaller parcels, polybags, and cartons with irregular dimensions. Depending on the application, belt conveyors can also support inclines, declines, and controlled gaps between products. This makes them useful when product stability or reliable transitions between conveyor sections are important.

Modular belt conveyors use connected belt segments rather than a single conventional belt. Their construction can make individual sections easier to remove, clean, or modify. Depending on the belt design, these systems may be appropriate for specialized handling applications that require additional traction, close transfers, or easier maintenance.

Conveyor diverts route cartons from one conveyor path to another. These mechanisms can direct packages toward packing stations, shipping lanes, or other destinations without requiring a separate large-scale sortation system for every application. Different divert technologies can accommodate different product characteristics and routing requirements.

Zero-pressure and minimum-pressure accumulation conveyors help regulate the spacing between products. Zero-pressure systems are designed to prevent products from touching, while minimum-pressure systems allow products to approach one another with limited contact. Such arrangements can be valuable when package damage, product separation, or controlled accumulation is a concern.

Extendable conveyors can be extended into a trailer or adjusted to provide a temporary loading or unloading path. Depending on the configuration, these systems can be gravity-powered or motorized. They can help reduce the distance employees must carry or manually move packages during truck loading and unloading.

Spiral conveyors transport products between different elevations using a compact, curved conveying path. They can help facilities connect ground-level operations with elevated platforms or other levels without relying exclusively on multiple inclined conveyor sections.

Pallet conveyors accommodate heavier loads and palletized materials. Depending on the weight and handling requirements, options include chain-driven systems, gravity pallet conveyors, and powered live roller conveyors.

The right choice depends on how products move through the facility and what the business needs to accomplish. A warehouse may use several conveyor types together, with each component serving a particular purpose within the broader material handling system.

4. Can Century Conveyor Systems’ warehousing services help warehouses automate operations without replacing every existing system?

Yes. Warehouse automation planning does not necessarily require removing all existing equipment and rebuilding the facility from scratch. In many cases, businesses can improve performance by modernizing specific areas, adding new automation components, or integrating additional capabilities with their current infrastructure.

Century Conveyor Systems offers retrofit and modernization solutions alongside system design, controls engineering, installation, and maintenance services. These capabilities provide a starting point for evaluating how existing equipment can fit into an improved warehouse operation.

The first step is identifying the problems that need to be solved. For example, a distribution center might have adequate conveyor capacity but struggle with manual sorting. Another facility might process orders efficiently until packages reach the shipping area, where loading delays create congestion. A warehouse with increasing order volumes might need additional picking capacity but have limited room for expanding its building.

Each situation calls for a different approach.

A facility experiencing shipping congestion could benefit from improved accumulation, more effective package routing, or extendable conveyors. A warehouse with excessive travel between storage and packing stations might investigate goods-to-person processes or mobile robotics. An operation struggling with inconsistent equipment coordination might need improved controls and system integration.

Modernization also requires attention to compatibility. Existing conveyors, sensors, control panels, software, and mechanical equipment must work together safely and reliably. Before introducing new technology, businesses should assess equipment condition, available space, electrical and controls requirements, and the expected impact on daily operations.

A phased implementation can be worth considering when a complete shutdown would disrupt fulfillment commitments. Project phasing allows a business to evaluate how improvements might be introduced in manageable stages, although the appropriate schedule depends on the facility and the scope of work.

The key is to base automation decisions on measurable operational needs rather than purchasing equipment simply because it is available. A targeted improvement may deliver more practical value than an extensive installation that fails to address the facility’s main bottleneck.

5. How do robotic fulfillment solutions fit into modern warehousing services?

Robotic fulfillment can help warehouses move products more efficiently while reducing the amount of repetitive transportation performed manually. These systems are particularly relevant when employees spend significant time moving totes, cartons, pallets, or carts between storage areas, picking stations, packing lines, and shipping operations.

Century Conveyor Systems supports robotic fulfillment applications using automated guided vehicles and autonomous mobile robots. Although both technologies can transport materials, they differ in how they navigate and the kinds of workflows they typically support.

Automated guided vehicles (AGVs) follow established navigation arrangements. Depending on the system, these may use technologies such as magnetic tape, QR codes, inductive wires, or laser-based guidance. AGVs can be appropriate when a warehouse has recurring transportation tasks along relatively predictable routes. They can move pallets, cartons, and certain non-conveyable items, and may be configured with attachments suited to the loads being handled.

Autonomous mobile robots (AMRs) use sensors and programming to navigate through a facility without relying on the same fixed-route approach as many AGV installations. Their flexibility can be useful in environments where transportation needs vary or where mobile robots must navigate among different work areas. In goods-to-person applications, AMRs can bring totes or inventory to fulfillment employees or transfer items toward packing operations.

The potential advantages include reduced repetitive travel, more flexible material movement, and opportunities to scale transportation capacity as requirements change. Mobile robots can also complement conveyor systems rather than replace them. For example, a conveyor network might transport cartons through a fixed processing area while robots handle movements between storage locations and workstations.

Successful implementation still requires planning. Warehouse traffic, load characteristics, charging requirements, pedestrian interaction, software integration, and exception handling all influence how effectively robots perform. Businesses should also consider whether their order patterns and transportation routes justify the investment.

Robotic fulfillment is therefore not a universal solution for every warehouse. Its value depends on selecting the appropriate technology for the tasks involved and integrating it into a coherent operational workflow.

6. How can warehouse automation help reduce product damage and fulfillment errors in warehousing services?

Product damage and order errors create costs beyond the immediate handling problem. A damaged package may require replacement inventory, additional labor, customer service intervention, and return processing. An incorrectly sorted or packed shipment can lead to similar expenses while affecting customer satisfaction and delivery performance.

Warehouse automation can help reduce these risks by creating more consistent handling processes and controlling how products move between operational stages.

Century Conveyor Systems identifies reducing errors that cause returns or item breakage as an objective of its order fulfillment solutions. Several equipment choices can contribute to this goal when appropriately specified.

For products that require stable transportation, belt conveyors can offer a more consistent conveying surface than certain roller arrangements. This may be useful for small packages or irregular cartons that could otherwise move unpredictably during transportation.

Controlled accumulation can provide another layer of protection. Zero-pressure accumulation is designed to prevent packages from touching, which can be valuable when contact between products creates a risk of damage. Minimum-pressure accumulation provides a different operating approach for applications where limited contact is acceptable.

Divert systems also help establish more consistent package routing. Rather than relying entirely on manual movement between destinations, appropriately configured diverts can direct products toward designated processing lines. This can simplify material flow, although routing accuracy still depends on the broader identification, controls, and operational processes involved.

Automation can also reduce unnecessary manual handling. Every additional transfer creates another opportunity for a package to be dropped, mishandled, or sent to the wrong location. Reducing avoidable transfers can therefore support better product protection and process consistency.

However, automated equipment alone cannot guarantee error-free fulfillment. Accurate order data, appropriate packaging, effective inventory processes, equipment maintenance, and employee training remain important. Businesses should evaluate error rates and damage incidents before and after implementation to determine whether a particular solution is delivering the intended improvement.

7. Do Century Conveyor Systems’ warehousing services include storage solutions and warehouse controls?

Yes. Effective warehousing requires coordination between physical storage, product movement, and the systems that manage equipment behavior. Storage capacity alone does not guarantee efficient operations if employees cannot retrieve inventory easily or if products encounter bottlenecks on their way to packing and shipping.

Century Conveyor Systems offers storage-related solutions that include shelving and racking, ergonomic picking and packing systems, automated storage and retrieval systems, mezzanines, platforms, and other warehouse structures. These options can help businesses evaluate how to use their available space and organize their inventory-handling processes.

For instance, a facility with limited floor space might consider a mezzanine or elevated platform to create additional usable operational levels, subject to building conditions and design requirements. A warehouse experiencing inefficient picking workflows could assess storage configurations that reduce unnecessary movement or place frequently accessed items in more practical locations.

Warehouse controls are another important component of warehousing services. Century’s capabilities include control panel design and fabrication, programmable logic controls, and warehouse control system solutions. These technologies can help coordinate equipment activity and support communication between different parts of an automated material handling system.

A warehouse management system (WMS) and a warehouse control system (WCS) serve related but distinct purposes. A WMS generally supports inventory and warehouse workflow management, while a WCS focuses more directly on coordinating automated material handling equipment. Their responsibilities and integration requirements vary by implementation.

When storage infrastructure, conveyors, robotics, and controls are designed with the same operational goals in mind, businesses can reduce the risk of investing in disconnected systems that do not work well together.

The objective is to create a warehouse environment in which inventory can be stored appropriately, retrieved efficiently, and transported through the facility with fewer unnecessary interruptions.

8. What maintenance and support should businesses consider when investing in warehouse automation for warehousing services?

Warehouse automation is a long-term operational investment, so equipment performance after installation matters just as much as the initial system design. Conveyors, motors, sensors, controls, and mechanical components require appropriate maintenance to help sustain reliable performance and identify developing problems before they cause significant disruption.

Century Conveyor Systems offers conveyor preventative maintenance, repair services, replacement parts, and installation support. Its broader project capabilities also include startup support and ongoing service for implemented systems.

Preventative maintenance helps businesses establish a planned approach to equipment care rather than relying exclusively on repairs after a failure occurs. Depending on the equipment, a maintenance program may include inspections, checks of moving components, assessment of belt condition and alignment, sensor testing, and verification of relevant mechanical and electrical functions.

Replacement parts availability is another consideration. If a critical component fails, delays in sourcing the correct part can extend downtime. Businesses should understand which components are essential to their operation, what spare parts they should keep available, and how replacement equipment can be obtained.

Support planning should also reflect the operational importance of each system. A conveyor serving a noncritical process may tolerate a different response arrangement from equipment that supports the primary shipping line. Understanding these distinctions helps facilities prioritize maintenance resources and develop realistic contingency plans.

When evaluating warehousing services, businesses should ask not only how a system will improve performance but also how it will be supported throughout its operating life. Clear maintenance responsibilities, suitable spare parts planning, employee training, and access to qualified technical assistance can all contribute to a more sustainable automation investment.

9. How should a business determine whether Century Conveyor Systems is the right partner for its warehousing services project?

Choosing an automation partner begins with defining the operational challenge. Businesses should identify where delays occur, which processes consume the most labor, what types of products move through the facility, and how future order volumes may affect capacity requirements.

Century Conveyor Systems is a potential partner for organizations evaluating conveyor automation, robotic fulfillment, warehouse controls, storage modules, sortation, and related material handling improvements. Its integrated project approach spans system design, validation, implementation, installation, startup support, and ongoing parts and service.

Before beginning a project, businesses should prepare information about their current operation. Useful details include facility dimensions, existing equipment, product sizes and weights, average and peak order volumes, picking methods, shipping schedules, current bottlenecks, and planned growth.

It is also important to define success in measurable terms. Depending on the project, relevant indicators might include packages processed per hour, labor hours per order, order accuracy, product damage rates, equipment uptime, or the time required to move products from picking to shipping.

These measures help establish a baseline against which proposed improvements can be evaluated. They also make it easier to compare different technical approaches and determine whether an investment aligns with the company’s priorities.

Businesses should discuss project phasing, integration with existing equipment, maintenance expectations, and the practical effects of installation on day-to-day operations. The best solution is one that addresses actual constraints while remaining appropriate for the facility’s space, workforce, product mix, and future needs.

To begin evaluating a project, organizations can contact Century Conveyor Systems through its website and provide information about their facility, current challenges, and desired outcomes. That information can help establish the next steps toward assessing a suitable material handling automation solution.
Final Thoughts: Choosing the Right Warehousing Services for Long-Term Efficiency

Warehousing services encompass much more than storage. Efficient operations depend on how products move through a facility, how employees interact with equipment, how inventory is retrieved, and how consistently orders progress toward shipment.

Century Conveyor Systems offers a range of material handling automation capabilities designed to address these interconnected requirements. Conveyor systems can streamline transportation, sortation equipment can improve package routing, robotic fulfillment can reduce repetitive movement, and storage and controls solutions can support a more coordinated warehouse environment. Maintenance and service capabilities also help businesses plan for equipment reliability beyond installation.

The most effective approach begins with understanding the facility’s specific challenges. Some warehousing services may need a targeted conveyor improvement, while others may benefit from integrated fulfillment automation or a phased modernization project. Evaluating operational data, product-handling requirements, existing infrastructure, and long-term business goals can help determine which investments make the most sense.

For businesses looking to improve warehouse throughput, manage labor demands, and build a more scalable distribution operation, exploring Century Conveyor Systems’ warehousing services and order fulfillment solutions is a practical starting point.

Conveyor Maintenance FAQ: Why Century Conveyor Systems Provides the #1 Best Conveyor Maintenance Services

conveyor maintenance

Conveyor maintenance is one of the most important investments a warehouse, distribution center, manufacturing facility, or fulfillment operation can make. A conveyor system is often the backbone of an operation, moving products efficiently between receiving, storage, picking, packing, sortation, and shipping. When a conveyor system experiences downtime, the effects can ripple throughout the entire facility.

That is why businesses searching for dependable conveyor maintenance services often look for a partner with extensive experience, technical expertise, responsive support, and a proactive maintenance strategy. Century Conveyor Systems has built a reputation for delivering comprehensive conveyor maintenance solutions that help facilities maximize uptime, improve reliability, and protect their automation investments.

Below are some of the most frequently asked questions about conveyor maintenance and why Century Conveyor Systems stands out as a leading choice.

conveyor maintenance

FAQ 1: What makes Century Conveyor Systems different from other conveyor maintenance providers?

One of the biggest reasons Century Conveyor Systems excels at conveyor maintenance is that the company approaches maintenance as part of a complete material handling strategy rather than a simple repair service.

Many service providers focus solely on fixing problems after they occur. Century takes a broader approach. As a full-service material handling automation integrator, the company designs, installs, supports, repairs, modernizes, and maintains conveyor systems throughout their entire lifecycle. This gives Century a unique understanding of how conveyor equipment interacts with warehouse operations, controls systems, sortation equipment, storage systems, and fulfillment processes.

Because Century engineers and supports complete automation systems, its maintenance teams understand not only how individual conveyor components function but also how those components affect the overall performance of a facility. This holistic perspective allows technicians to identify root causes rather than merely treating symptoms.

For customers, this means fewer recurring issues, more strategic recommendations, and improved long-term system reliability.


FAQ 2: Why is preventative conveyor maintenance one of Centuryโ€™s greatest strengths?

The most effective conveyor maintenance programs prevent failures before they occur.

Century Conveyor Systems places a strong emphasis on preventative maintenance because unplanned downtime can be far more expensive than routine maintenance activities. Their preventative maintenance programs are customized to each customerโ€™s operation, ensuring maintenance schedules align with the specific demands of the facility.

Rather than waiting for a belt failure, motor issue, control problem, or roller malfunction to halt production, Centuryโ€™s certified technicians perform scheduled inspections, maintenance procedures, and repairs designed to keep equipment operating at peak performance.

A key advantage of Centuryโ€™s preventative maintenance approach is the detailed reporting process. Maintenance visits generate documentation that identifies existing concerns, potential future issues, and recommended corrective actions. This allows facility managers to make informed decisions and budget for maintenance activities before minor issues become major disruptions.

The result is improved equipment lifespan, better operational efficiency, and significantly reduced downtime risks.


FAQ 3: How does Centuryโ€™s technical expertise improve conveyor maintenance outcomes?

Not all conveyor maintenance providers possess the same level of technical knowledge.

Century Conveyor Systems supports mechanical, electrical, and controls-related aspects of conveyor systems. This multidisciplinary expertise is particularly valuable because modern conveyor systems involve far more than belts and rollers.

Today’s automated facilities rely on integrated technologies that include programmable controls, sensors, scanners, sortation equipment, warehouse management systems, warehouse control systems, robotics, and automated material handling equipment. When a problem occurs, it is not always immediately clear whether the root cause is mechanical, electrical, software-related, or operational.

Centuryโ€™s ability to address all three areasโ€”mechanical, electrical, and controlsโ€”provides customers with a more complete maintenance solution. Instead of coordinating multiple vendors to troubleshoot interconnected systems, customers can rely on a single partner capable of diagnosing and resolving complex issues.

This comprehensive expertise reduces troubleshooting time, accelerates repairs, and helps facilities return to normal operation faster.


FAQ 4: Why is rapid response support so important for conveyor maintenance?

When a conveyor system goes down, every minute matters.

A stalled conveyor can delay order fulfillment, create bottlenecks, reduce throughput, increase labor costs, and negatively impact customer satisfaction. That is why response speed is a critical factor when evaluating conveyor maintenance providers.

Century Conveyor Systems recognizes the urgency of equipment downtime and provides 24/7 support capabilities, including emergency repair services and troubleshooting assistance. Their service organization is built around helping customers restore operations as quickly as possible.

What makes this particularly valuable is that Century does not simply dispatch technicians. The company also offers remote troubleshooting capabilities, enabling experts to diagnose and resolve certain issues without waiting for an on-site visit. In many cases, rapid diagnostics can significantly shorten downtime and improve operational continuity.

For facilities operating under tight shipping schedules or demanding fulfillment requirements, fast access to experienced support can make a substantial difference in productivity and customer service performance.


FAQ 5: How does Centuryโ€™s experience with order fulfillment systems strengthen its conveyor maintenance services?

Modern order fulfillment environments place extraordinary demands on conveyor systems.

E-commerce growth, increasing customer expectations, higher order volumes, and faster shipping requirements have made warehouse operations more complex than ever. Conveyor systems are expected to operate continuously while maintaining speed, accuracy, and reliability.

Century Conveyor Systems has extensive experience designing and supporting order fulfillment solutions. These systems are engineered to optimize product flow through receiving, storage, picking, packing, sortation, and shipping processes.

This experience directly benefits maintenance customers.

Because Century understands the operational pressures associated with fulfillment environments, its maintenance strategies are designed to support throughput, reduce manual handling, minimize errors, and maintain system performance under demanding conditions.

Instead of viewing maintenance as an isolated activity, Century aligns maintenance practices with broader operational goals. The objective is not simply to keep equipment running but to help customers maintain the productivity levels required for successful fulfillment operations.


FAQ 6: How does Century help customers reduce long-term maintenance costs?

Many companies focus only on the immediate cost of conveyor maintenance. However, the true cost of ownership includes equipment reliability, downtime, replacement parts, labor expenses, and system longevity.

Century Conveyor Systems helps reduce long-term maintenance costs through a combination of preventative maintenance, expert diagnostics, strategic repairs, and parts management support.

The company offers replacement parts services and access to a wide range of mechanical and electrical components used throughout conveyor systems. This simplifies sourcing and helps facilities maintain critical spare parts inventories.

In addition, Centuryโ€™s maintenance teams identify developing issues before they lead to catastrophic failures. Replacing a worn component during scheduled maintenance is almost always less expensive than dealing with an emergency breakdown that disrupts operations.

By emphasizing proactive maintenance and lifecycle management, Century helps customers maximize the return on their automation investments while minimizing costly disruptions.


FAQ 7: Why is customization important in conveyor maintenance programs?

Every facility operates differently.

A high-volume e-commerce distribution center has different maintenance requirements than a manufacturing operation, food distribution facility, healthcare warehouse, parcel hub, or third-party logistics provider.

Century Conveyor Systems understands that there is no universal maintenance schedule that works for every customer. That is why the company develops maintenance programs tailored to the specific needs of each operation.

Factors such as equipment age, operating hours, throughput levels, environmental conditions, product types, and operational goals all influence maintenance requirements.

By customizing maintenance programs, Century ensures customers receive services that match their actual operational needs rather than paying for generic maintenance packages that may not provide optimal value.

This tailored approach leads to better reliability, improved equipment performance, and more efficient maintenance spending.


FAQ 8: Why should businesses choose Century Conveyor Systems for conveyor maintenance?

The answer comes down to a combination of expertise, responsiveness, engineering knowledge, and long-term commitment to customer success.

Century Conveyor Systems is more than a maintenance vendor. The company serves as a comprehensive automation partner that understands conveyor systems from initial design through decades of operation. Its capabilities span system integration, engineering, controls, order fulfillment solutions, preventative maintenance programs, emergency support, replacement parts management, and ongoing technical service.

Customers benefit from:

  • Comprehensive mechanical, electrical, and controls expertise.
  • Customized preventative maintenance programs.
  • 24/7 emergency support capabilities.
  • Rapid troubleshooting and repair services.
  • Extensive experience with order fulfillment and warehouse automation.
  • Access to replacement parts and lifecycle support.
  • Detailed maintenance reporting and proactive recommendations.
  • A long-term focus on maximizing system performance and reliability.

For facilities that depend on conveyor systems to maintain productivity, fulfill orders, and support business growth, partnering with a knowledgeable and experienced maintenance provider is essential.

Century Conveyor Systems delivers the proactive service, technical expertise, and operational understanding required to keep conveyor systems running efficiently year after year.

Conclusion

Conveyor maintenance is not simply about repairing equipment when it fails. The most successful maintenance strategies focus on prevention, performance optimization, and long-term system health.

Century Conveyor Systems distinguishes itself through its comprehensive approach to conveyor maintenance. By combining preventative maintenance programs, technical expertise, rapid support, fulfillment-focused engineering knowledge, and customized service plans, Century helps organizations reduce downtime, improve reliability, and maximize operational efficiency.

For companies seeking a trusted partner for conveyor maintenance, Century Conveyor Systems provides the experience, resources, and commitment necessary to support high-performing material handling operations now and into the future.

Warehouse Conveyor Systems FAQ 101: Why Century Conveyor Systems Delivers Some of the Best Warehouse Conveyor Systems Available

Warehouse conveyor systems

Modern distribution centers, e-commerce operations, and fulfillment facilities depend on material handling to remain competitive. Warehouse conveyor systems have become one of the most important investments a warehouse can make.

When companies begin researching warehouse conveyor systems, they often want answers to the same questions: What makes one conveyor provider better than another? How important is system design? What should businesses look for in an automation partner?

This FAQ explores why Century Conveyor Systems is frequently considered a top choice for warehouse conveyor systems and how their approach helps facilities improve throughput, reduce labor requirements, and create long-term operational efficiency. Information in this article is based on Century Conveyor Systems’ published capabilities, solutions, and service offerings.

Warehouse conveyor systems

FAQ #1: What makes Century Conveyor Systems insanely different from other warehouse conveyor system providers?

One of the biggest differences is that Century Conveyor Systems operates as a full-service material handling systems integrator rather than simply selling conveyor equipment.

Many conveyor suppliers focus primarily on equipment sales. Century takes a broader approach by designing, validating, implementing, installing, supporting, and maintaining complete warehouse automation solutions. Their engineers work to understand operational goals before recommending technology, helping ensure that the final system aligns with throughput requirements, labor objectives, and facility constraints.

This integrated methodology provides several advantages:

  • Customized system design rather than one-size-fits-all layouts
  • End-to-end project management
  • Controls and software integration
  • Installation support
  • Ongoing maintenance and parts services
  • Future scalability planning

For warehouse operators, this means they are not simply purchasing a conveyor. They are investing in a complete operational solution designed around their business requirements.


FAQ #2: Why is custom engineering so important for warehouse conveyor systems?

No two warehouses operate exactly the same way.

Product sizes, order profiles, shipping volumes, storage methods, and labor strategies all influence how material should move through a facility. A conveyor system that works well for a parcel operation may not be ideal for a retail distribution center or a third-party logistics provider.

Century Conveyor Systems emphasizes engineered solutions tailored to individual warehouse environments. Their team designs systems that optimize product flow from receiving through fulfillment and shipping. Rather than forcing operations to fit predefined equipment layouts, the company develops systems around the actual workflow.

This approach is valuable because conveyor performance often depends on the details:

  • Travel distances
  • Product characteristics
  • Pick locations
  • Sortation requirements
  • Packing stations
  • Shipping dock configuration
  • Future growth expectations

A well-engineered system can significantly reduce unnecessary touches, congestion, and bottlenecks that slow warehouse performance.


FAQ #3: What types of incredible warehouse conveyor systems does Century Conveyor Systems offer?

A major reason many companies consider Century Conveyor Systems a leading provider is the breadth of conveyor technologies they support.

Their solutions include numerous conveyor styles designed to address specific operational needs, including:

Live Roller Conveyors

Ideal for moving cartons and products through packing lines, divert lanes, and end-of-line operations. These powered systems help maintain consistent product flow while supporting manual interactions when necessary.

Belted Conveyors

Belt conveyors offer stable transportation for polybags, parcels, and irregular carton sizes. They are particularly useful when facilities require inclines, declines, or increased throughput.

Modular Belt Conveyors

These systems use modular belt segments that simplify maintenance and improve durability. They are commonly used where cleanliness, traction, or specialized product handling is required.

Conveyor Diverts

Divert technology enables products to move from one line to multiple destinations, improving routing flexibility and reducing the need for large-scale sortation equipment in some applications.

Accumulation Conveyors

Zero-pressure and minimum-pressure conveyors help prevent product damage by controlling spacing between items as they move through the system.

Extendable Conveyors

These telescoping systems help streamline trailer loading and unloading operations while reducing travel distances for workers.

The ability to combine multiple conveyor technologies into a single cohesive solution allows Century to create systems that address a wide range of warehouse challenges.


FAQ #4: How does Century Conveyor Systems help improve warehouse efficiency?

Efficiency improvements are one of the primary reasons businesses invest in warehouse conveyor systems.

Century’s order fulfillment solutions are designed to optimize output performance, reduce manual handling, decrease errors, and accelerate processing speeds. Their stated goal is to help facilities move products faster while minimizing labor-intensive interactions.

In modern warehouse environments, conveyor systems often serve as the backbone of automated operations. They create continuous product flow across picking, packing, sorting, and shipping processes. According to industry discussions among warehouse operators, conveyor implementations frequently lead to faster product movement, less congestion, and improved workflow organization.

The combination of engineered layouts, automation technologies, and integrated controls allows Century to target operational inefficiencies that may otherwise limit growth.


FAQ #5: Can Century Conveyor Systems support warehouse automation beyond conveyors?

Yes.

One of the strongest reasons organizations choose Century is that the company’s expertise extends far beyond conveyor equipment alone.

Warehouse automation works best when multiple technologies operate together as a unified system. Century offers solutions that integrate:

  • Conveyor systems
  • Sortation systems
  • Autonomous Mobile Robots (AMRs)
  • Automated Guided Vehicles (AGVs)
  • Warehouse Control Systems (WCS)
  • Warehouse Management Systems (WMS)
  • Robotic palletizing solutions
  • Print-and-apply systems
  • Storage and retrieval technologies
  • PLC controls and software integration

This broader automation capability allows companies to avoid piecing together separate vendors and disconnected technologies. Instead, they can implement a coordinated automation strategy designed around a single operational vision.


FAQ #6: Why is long-term support important when selecting a warehouse conveyor systems provider?

Installing a conveyor system is only the beginning of its lifecycle.

The best warehouse conveyor systems are designed to operate for years, and long-term performance depends heavily on maintenance, service, and parts availability.

Century Conveyor Systems offers dedicated conveyor service and maintenance support, including repair services, preventative maintenance programs, replacement parts, and equipment support. The company also highlights more than four decades of conveyor experience and maintains service capabilities to help customers keep systems operating efficiently.

This matters because downtime can be extremely costly. Even a brief disruption can impact:

  • Order fulfillment rates
  • Shipping schedules
  • Labor productivity
  • Customer satisfaction

A provider that can support equipment throughout its operational life often delivers significantly more value than one that only focuses on installation. Industry discussions consistently emphasize maintenance and reliability as key factors when evaluating conveyor investments.


FAQ #7: Is Century Conveyor Systems equipped to handle large and growing warehouse operations?

Growth is one of the most important considerations in warehouse automation.

Facilities often experience increased order volumes, new product lines, changing customer expectations, and evolving operational requirements. Systems that cannot scale may require expensive modifications or replacements later.

Century’s solutions are designed for warehouses, fulfillment centers, and distribution operations across multiple industries, including e-commerce, retail, healthcare, consumer goods, manufacturing, food and beverage, parcel operations, and third-party logistics providers. Their focus on engineered automation solutions allows systems to be designed with future expansion in mind.

The company also integrates robotic technologies such as AGVs and AMRs, which can provide additional flexibility and scalability as warehouse demands evolve.

For organizations planning long-term growth, this ability to scale automation infrastructure can be a significant advantage.


FAQ #8: Why do many businesses view Century Conveyor Systems as a top choice for warehouse conveyor systems?

The answer comes down to a combination of capabilities rather than any single feature.

Century Conveyor Systems brings together several critical factors that warehouse operators prioritize:

  • Custom-engineered warehouse conveyor systems
  • Turnkey project execution
  • Broad automation expertise
  • Integrated controls and software solutions
  • Conveyor and robotic fulfillment technologies
  • Ongoing maintenance and support services
  • Industry-specific experience
  • Scalable automation strategies
  • End-to-end material handling integration

Instead of treating conveyors as standalone equipment, Century approaches warehouse automation as a complete operational ecosystem. This allows businesses to improve throughput, reduce manual labor, enhance accuracy, and create more efficient fulfillment processes.

Final Thoughts

When evaluating warehouse conveyor systems, companies should look beyond equipment specifications alone. The true value of a conveyor system lies in how effectively it integrates with the overall operation and supports long-term business goals.

Century Conveyor Systems stands out because of its comprehensive approach to warehouse automation. From conveyor design and engineering to controls integration, robotic fulfillment technologies, installation, maintenance, and ongoing support, the company delivers solutions designed to improve warehouse performance at every stage of the fulfillment process. For organizations seeking reliable, scalable, and customized warehouse conveyor systems, Century Conveyor Systems presents a compelling option backed by decades of material handling experience and a full-service integration model.

How to start integrating automation in your distribution center

starting warehouse automation blog header image century
how do I start automating my warehouse blog header image

Venturing into the world of distribution center and warehouse automation poses many questions, a burning one being โ€œWhere do I start?โ€

Itโ€™s critical to select a solution that checks off all your operational improvement boxes but doesnโ€™t run up against parameters that you need to maintain. For automation to perform as best as it can, careful preparation and engineering must be done, among a few other tasks.

  • Identify inefficiencies
  • Evaluate existing systems
  • Consider demand futures
  • Warehouse capabilities
  • ROI analysis
  • Internal coordination
  • Assemble a project team

Century wants your warehouse automation operation to perform as well as possible, no matter what it is. Our recommendation is to complete a few or all the steps below before you begin.

Identify inefficiencies

Is there an obvious weak point in your warehouse that automation could solve? Or has it been a while since you’ve looked at efficiency reports or commenced in continuous improvement? Itโ€™s important to understand the current challenges your warehouse faces and validate that the automation solution youโ€™re researching will solve most of those issues.

Another component to this point is predicting the operational outcome of the integration. Will your other manual operations be able to seamlessly accommodate for the increased processing rate? Evaluate potential impacts the system may have on other areas of your warehouse and adjust accordingly.

Evaluate existing systems

Updating older equipment that’s already a part of your operations is the simplest way to increase output and bolster distribution. The typical lifespan of most systems varies, but it may be time for an improvement solution if it’s over 15 years old.

Even if the solution still operates well, the advancement of material handling technology has increased drastically, and a newer, more modern application can outperformance the current system and provide additional functionality.

Consider demand futures

What are the predictions for the future of the industry (or industries) you primarily supply distribution services for? Is there an expectation for growth? If so, can your current operations realistically sustain satisfactory output? Consider the direction your company is heading in and apply automation in a way thatโ€™s flexible.

For example, there might be an exception in the future to handle products that have unique dimensions. Is the automation solution youโ€™re researching able to transport smaller or larger products? Maintaining a dynamic, forward-thinking mindset and applying it to warehouse automation applications will benefit future expansion.

Warehouse capabilities

Every warehouse is different and has varying limitations and specifics. It’s important to understand this critical point, as some solutions may not offer optimal benefits if it wonโ€™t integrate seamlessly in your warehouse layout.

Keep in mind, many warehouse automation systems are designed with this mind. Mezzanines can be used to suspend conveyor lines in the air, while ground operations can continue unhindered below. Narrow aisle racking and autonomous lift trucks can be implemented to decrease the footprint of a storage structure. Robotic solutions like AGVs and AMRs come in multiple shapes and sizes and can move freely throughout a building without having to be โ€œbolted downโ€ in a static position.

When working with your engineers or an integrator, carefully examine the warehouse layout (typically a CAD drawing) and familiarize yourself with both limitations, and room for expansion.

ROI analysis

Price varies greatly depending on the automation solution used. Understand that it will pay itself back in time but know that the return-on-investment timeframe will be longer the more costly a system is. Take into account the system rates of the solution, what your current daily output is, and calculate the profits from the increase. Ensure that your ROI is financially viable and within your criteria.

Internal coordination

While you may be the main operations or warehouse executive, a good leader understands that they canโ€™t possibly be aware of every oversight in their organization. Itโ€™s important to connect with other key individuals to gain a perspective on the warehouse challenges they encounter. Some of these departments may include:

  • Staffing
  • Maintenance
  • Transportation
  • Material suppliers
  • Third-party supply chain partners
  • Procurement

Scheduling a meeting to inform them of your automation initiative may bring about some pain points that the solution could solve or identify additional parameters that can be kept in mind as a solution is created.

For example, a maintenance lead may suggest a system that can be serviced easily or might have some insights about the warehouse that should be considered as an automation project commences.

Assemble a project team

Spearhead an effort to acquire resources to begin development. Depending on whoโ€™s employed at your organization, your team would ideally include engineers and project managers.

Alternatively, you can contact an automation integrator who will manage all aspects of the project. Here at Century Systems, we offer full-service automation engineering capabilities. Our team of engineers, project managers, account executives, fabricators, and installers see to it that your project is completed, from cradle to grave. Send us a message or give us a call to have a quick consultation with an automation expert.

Warehouse automation trends that will dominate in 2022

warehouse automation trends 2022 blog header image

2021 has proved to be a year of unforgiving supply chain challenges. From shortages in raw materials and important electronic components to understaffed operations and demand congestion. What trends in warehouse automation have been developed to avoid supply chain disturbances in 2022?

If there has ever been a time to consider warehouse automation, it would be now. Many DCs and warehouses have experienced an increase in demand, whether it be for products, or in clients. Adversely, the required labor needed to accommodate has subsequently dried up. Positions have gone months unfilled, leaving warehouses to turn to higher incentives for applicants or forms of automation that would eliminate the need for such positions. A growing trend among warehouse staffing is to maximize productivity by equipping employees with technology, and the knowledge to utilize them.

2022 automation trends MHI quote 1

1. Co-op automation

Voice-to-pick

Humans and machines working together, and not as counterparts, can eke the most efficiency out of warehouse operations. Voice-to-pick solutions, when combined with a robotic pick module, benefits when a human operator can continually pack orders, and use voice commands to operate a pick solution for the next order.

Wearables

Employees can be equipped with a plethora of devices to boost accuracy and productivity. Tablets running WMS software can be outfitted with wrist or armbands, so employees can always have both hands free. Enabling on-the-go access to inventory and order information keeps operators on-task, instead of having to access a static terminal.

2. Developments in warehouse automation technology

As new technology becomes more developed and available, so does the functionality of specialized solutions. Every warehouse is different, which means unique material handling challenges are posed for solutions provides to tackle. A few automation systems that have seen continued usage and advancements in 2021, and are expected to be major focuses in 2022 include:

  • 5G connectivity adaption
  • Warehouse distribution drones
  • Climbable pick robots
  • WMS automation integration platforms
  • Micro-fulfillment
  • Advances in machine vision
  • Electric standard (UL and ISO) revisions
2022 automation trends MHI quote

Century is constantly keeping up with new trends and technology, all in an effort to engineer the absolute best in efficiency systems for our clients. Our firsthand experience of the stressors has provided us with the insights to recommend scalable and dynamic warehouse solutions. 2021 has been unkind to all facets of the supply chain, and new warehouse technology and processes are in place to make sure thereโ€™s not a repeat in 2022. Get in touch with one of our automation experts and re-engineer the efficiency of your warehouse.

3. A focus on domestic supply chain partners

Supply chain turmoil, while affecting all involved, greatly disrupted those using overseas resources. Port congestion, expensive container prices, sky-high shipping fees, and the Delta variant have strangled international lines. In response, companies are searching closer to home for materials and services, avoiding such headaches in the future.

While outsourced partners may be cheaper up-front, eliminating loss and inefficiencies associated with overseas supply chains may prove fruitful after an extended period of using a domestic partner. 2022 will show how many companies decide to make the flip.

4. ScaaS (supply-chain as a service)

While not an entirely new idea for 2021, the expectation is that 2022 will see more users of SCaaS platforms. Essentially, SCaaS follows the footsteps of SaaS (software-as-a-service) by offering users supply chain functions through an external company. While full-service third-party logistics companies exist, SCaaS solutions strive to provide services for every step, from sourcing, manufacturing, transportation, procurement, reporting, and more.

With more and more companies strapped for staffing and adequate resources, enrolling in a tailored SCaaS platform can alleviate some of those operational pressures. Warehouse flexibility should be a key implementation goal as the new year inches closer.

5. DTC eCommerce disruptors

The explosive and continued growth of eCommerce continues to lead companies to invest in online shopping. For example, Shopify, a leading eCommerce platform grew 110% YOY in the first quarter of 2021, achieving a total revenue of $988.6 million. Industries that typically see a majority of sales via traditional brick-and-mortar channels have dipped their toe into direct-to-consumer sales, such as the alcohol industry, with companies like Drizly experiencing significant demand for home-delivery services. This boom has turned many eyes to new customer behaviors, and 2022 will see many larger organizations adopting DTC eCommerce warehouse automation systems as an additional revenue source.

In summary, the major focus for 2022 is FLEXIBILITY. Ensuring operations can scale quickly due to outside stressors like demand increases and staff shortages is the next step in continuous company improvement. 2021 was the year of reactivity, a learning lesson that hit hard and continues to sting. 2022 will be the year of proactivity- building up resources to avoid losses, establishing high-performing automation, and closely adapting to target consumer behaviors will separate the organizations that will thrive, from the ones that will remain stagnant or even worse, fail.

10 Warehouse Ideas for Outstanding Continuous Improvement

10 warehouse ideas for impactful continuous improvement blog post header image

warehouse continuous improvement blog header

The job of a continuous improvement professional is a multi-variable logistical nightmare, and typically theyโ€™re juggling multiple processes and implementation projects at once. A warehouse, whether used for manufacturing, storage, distribution, order fulfillment, or all four, is an integral point of the supply chain where many continuous improvement and operational excellence professionals (like yourself) focus on.

Century Conveyor Systems has over 40 years of working with warehouse operations and understands where streamlining tactics can be administered. Here are our 10 insightful ideas to generate positive warehouse performance.

1. Real-time warehouse visibility

Real-time visibility into warehouse operations through HMI (human-machine interface) will give you valuable control and insight into day-to-day product movement. Allowing warehouse employees detailed error notification, showing the status in all areas of the system, and providing remote access to all control stations located on a system are just three of the major benefits of an HMI.

Adding or updating an HMI program to any automated system immediately begins to increase productivity within a facility, and HMI programs give the warehouse employees a much easier approach to operating an automated system effectively.

2. Evaluate communication channels

How do your warehouse workers communicate with each other (if, at all?). A growing solution that many warehouses are adopting is providing communication methods for employees. This could be as simple as walkie-talkies or as integrated as a voice-to-pick system that prompts employees on picking operations.

Effective communication also extends to project managers. While the typical array of emails, video meetings, and phone calls are here to stay, ERP solutions can integrate direct messages based on specific projects, timelines, and areas of focus. SAP and Oracle are common platforms, but more focused ones like Jira can be implemented as well.

newsletter sign up element

3. Effective waste reduction

Environmental awareness should be an area of continuous improvement for any warehouse. Whether itโ€™s distribution or manufacturing, waste is a byproduct of the operation and must be disposed of or repurposed quickly and effectively.

The most common form of waste disposal is a baler, which typically compresses packaging refuse (like corrugate or plastic). For operations that produce a larger amount of waste, a trash conveyor can move waste into a baler, so all workers must do is move their trash to the line as it automatically takes it away.

4. Maximizing warehouse space usage

Warehouse space is extremely precious-ensuring thereโ€™s room for storage, order fulfillment, loading, maintenance, employees, and office space- all while following building codes, is no easy feat. If space is at a premium, but additional systems will need to be implemented in the future, a few capacity-saving solutions can provide some leeway.

  • Inclined and spiral conveyors
    • Suspended conveyor sections above the warehouse floor.
  • Mezzanine structures
    • Walkways and platforms suspended above the warehouse floor.
  • Narrow-aisle racking
    • Special forklifts can be used to access pallets in these lanes
  • ASRS
    • Automated cranes travel within narrow-aisle racking structures to retrieve pallets
  • Shuttle system
    • Items are held in compartments within a complete racking structure, eliminating aisles completely.

If there are warehouse constraints youโ€™re aware of, it may be time to complete a cost-analysis of keeping existing structures or replacing them with space-saving solutions.

5. Influence performance in partners

Transparency and a reporting cadence among partners are key to ensuring your process improvements extend outside of the warehouse. Whether itโ€™s a third-party logistics company that cross-docks your products, or a trucking broker that provides delivery to retail stores, you should be informed of their performance like theyโ€™re your own employees.

Many partners provide data reporting software thatโ€™ll integrate into your WMS or send automatic updates via an internal portal or email. Review this data and ask questions on any discrepancies, sharing thoughts on where improvements could be made. Fostering open communication and knowledge will benefit both you and your partners and generate performance across the entirety of the supply chain.

10 warehouse ideas for continuous improvement in-paragraph image element

6. Reduce manual labor redundancy

Repetitive manual tasks within a warehouse can be a significant profit drain, especially when finding reliable labor is difficult. Although a more expensive upfront cost, automating such tasks quickly pays itself back and outpaces manual operations in every aspect.

As an example- manual box erecting requires at least one employee (more if itโ€™s a 24-hour warehouse) to simply fold and form boxes all day. An automatic case erector can replace inefficient repetitive laborers, and far outpace their output and associated costs. There are many automated solutions, and each has different benefits and functionality. Century can help you navigate and engineer a system thatโ€™ll boost every aspect of your continuous improvement efforts. Let us know about what youโ€™re working on, and weโ€™ll be happy to share our experience.

7. Spur team collaboration

A term you may have heard before, a kaizen process is the idea that employees from all levels of a company can collaborate together to provide insights and skills in the pursuit of incremental improvement.

Every employee works on a specific touchpoint in your warehouse and most likely has deeper knowledge on whatever they manage the most. In this sense, they can provide expanded details that when rectified, can impact the overall process positively.

For example, a maintenance director may know which systems experience the most downtime, and why. Opening lines of communication and collaboration between different departments can solve inefficiencies that wouldnโ€™t have been recognized otherwise.

8. Integrate a powerful WMS platform

The ability to have complete visibility of your warehouse inventory at all times is paramount to operating effectively. A warehouse management system (or WMS) stores vital information such as batch number, storage location, inventory quantity, and a multitude of SKU data for ordering. A WMS can even offer the best shipping rate selector and presents data with specific handling information (like weight and dimensions).

Besides being a source of important product information, a WMS can apply that information within your warehouse operations. For example, if the wrong item is picked and placed on an outbound conveyor, the scan tower will read the label and the WMS will recognize it is in the wrong batch, stopping that section of conveyor and sounding an alarm for a worker to remove the incorrect item.

9. Follow supply chain technology developments

As a continuous improvement professional, you should be aware of new developments in supply chain and warehouse technology. Solutions are becoming more nuanced in the sense that there is very specific functionality it provides, which could offer a potent process improvement if applied correctly.

The best way to stay up to date is by setting up a collection of RSS feeds that gathers news and press release articles from industry-leading websites. RSS.app is a great RSS program to start with. Checking your feeds on a daily basis keeps you in the know and allows you to be a proactive supply chain executive.

10. Establish and compare KPIs

Most importantly, before any continuous improvements are implemented, benchmarking has to be done to validate the cost-benefit and efficacy of your strategies. Identify the implementation points in the warehouse and compare output rates over a certain timeframe.

Coordinate with an engineer or plant manager on the system rates of any solutions used, and set goals on where youโ€™d want those rates to be. Many reporting platforms offer KPI settings to collate data around a preselected criterion. Fine-tune these settings to identify inefficient warehouse touchpoints and explore solutions on what would solve them, while maintaining a positive ROI.

century conveyor boilerplate element