Warehouse Fulfillment 101: Frequently Asked Questions About Century Conveyor Systems’s Amazing Services

warehouse fulfillment

Warehouse fulfillment is a critical part of modern supply chain operations. As customer expectations for faster deliveries, accurate orders, and reliable shipping continue to grow, warehouses and distribution centers must find ways to improve productivity without continually increasing labor costs. Efficient warehouse fulfillment requires more than simply picking products and preparing packages. It involves coordinating inventory movement, order processing, sorting, packing, and shipping through a well-designed material handling system.

Century Conveyor Systems helps businesses improve warehouse fulfillment through engineered conveyor systems, robotic automation, material handling equipment, and integrated warehouse technologies. By designing solutions around the specific needs of each facility, Century helps warehouses increase throughput, reduce unnecessary manual handling, and create more efficient fulfillment operations.

Below are some frequently asked questions about Century Conveyor Systems and its approach to warehouse fulfillment.

warehouse fulfillment

1. What Is Warehouse Fulfillment, and How Does Century Conveyor Systems Improve the Process?

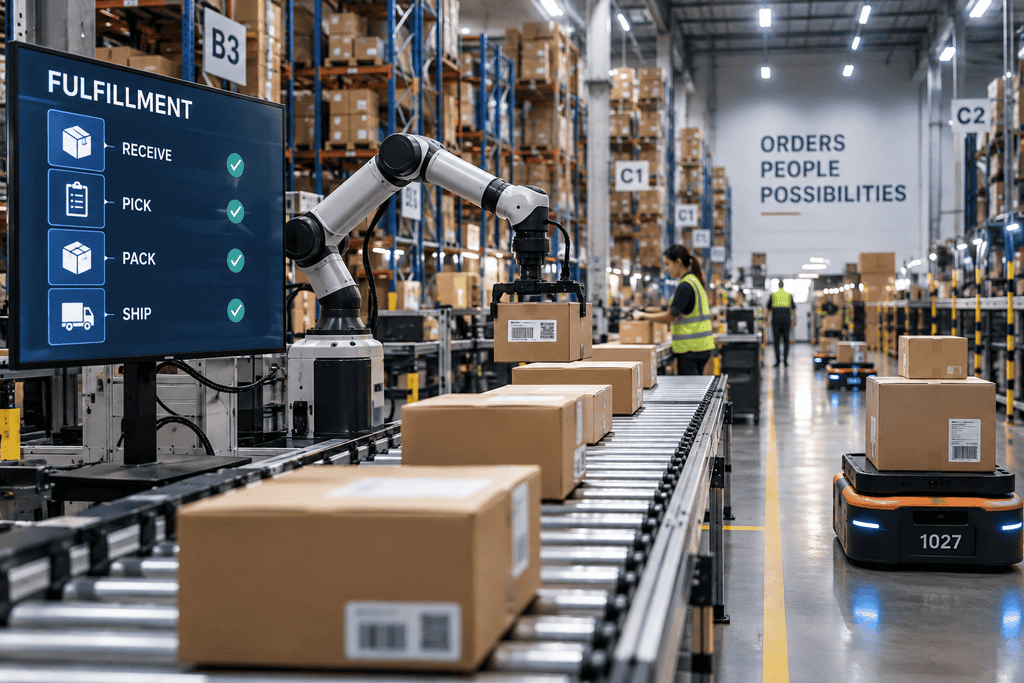
Warehouse fulfillment refers to the complete process of receiving, processing, picking, packing, sorting, and preparing customer orders for shipment. It begins when an order enters the fulfillment operation and continues until the products reach the shipping area, where they are loaded for delivery.

Every step must work together to ensure orders are processed accurately and efficiently. When a warehouse relies heavily on manual transportation, repetitive handling, or disconnected processes, bottlenecks can develop. These inefficiencies can slow down order processing, increase labor requirements, and create opportunities for shipping errors.

Century Conveyor Systems addresses these challenges by engineering automated material handling solutions that connect different stages of warehouse fulfillment. Its solutions include conveyor systems, robotic fulfillment equipment, sortation systems, warehouse controls, and storage modules.

Rather than treating each piece of equipment as an isolated improvement, Century approaches warehouse automation as an integrated operation. Its engineers design, validate, and implement systems that support the movement of products throughout the facility.

This approach helps businesses improve productivity at multiple points in the fulfillment process. Products can move between workstations with fewer manual transfers, orders can be directed toward the appropriate processing areas, and warehouse employees can focus on tasks that require more direct involvement.

The ultimate objective is to create a warehouse fulfillment operation that processes more orders while minimizing unnecessary labor, handling, and operational delays.

2. Why Are Conveyor Systems Important for Warehouse Fulfillment?

Conveyor systems are one of the most important components of an automated warehouse fulfillment operation because they provide a consistent way to transport products throughout a facility.

Without an effective transportation system, employees may need to move cartons, totes, and pallets manually between picking, packing, sorting, and shipping areas. This can consume valuable labor hours and create unnecessary travel throughout the warehouse.

Century Conveyor Systems engineers conveyor solutions designed to match the layout, product characteristics, and processing requirements of individual facilities.

Depending on the application, a conveyor system can transport small parcels, irregular cartons, heavy products, or full pallets. Different conveyor sections can also perform specific functions, including accumulation, product transfers, diverting, and elevation changes.

One important advantage of conveyor automation is its ability to create a continuous flow of products. Instead of relying on employees to transport every item between workstations, conveyors move products along predetermined routes.

Century offers several conveyor technologies for different warehouse fulfillment applications, including:

  • Live roller conveyors: Powered roller conveyors that move cartons through packing lines, divert areas, and end-of-line operations.
  • Gravity conveyors: Non-powered conveyors that use gravity to move products, making them useful for staging and manual handling applications.
  • Belt conveyors: Provide stable transportation for small parcels, polybags, and irregularly sized cartons.
  • Modular belt conveyors: Feature removable belt sections that can simplify cleaning, maintenance, and modifications.
  • Pallet conveyors: Provide durable transportation for pallets and heavier loads.
  • Extendable conveyors: Extend directly into trailers to help move packages toward loading associates.

Selecting the appropriate conveyor technology allows businesses to create a transportation system that supports their specific fulfillment requirements.

3. How Can Warehouse Automation Reduce Labor Costs?

Labor is one of the most significant operational expenses for many warehouses and distribution centers. As fulfillment volumes increase, businesses often need additional employees to transport products, move materials, sort packages, and complete repetitive handling tasks.

However, adding more employees does not necessarily solve the underlying inefficiencies in a warehouse. If workers spend a considerable amount of time walking between stations or moving products manually, productivity can remain limited.

Warehouse automation helps address this problem by reducing the amount of repetitive manual work required to process orders.

Century Conveyor Systems focuses on designing systems that allow products to move efficiently between different stages of the fulfillment process. Conveyor equipment can automate transportation, while robotic systems can assist with moving cartons, totes, and pallets.

For example, an automated conveyor network can transport packages from packing stations to sorting equipment without requiring employees to manually move each carton. Similarly, automated mobile robots can retrieve products or transport materials between designated areas.

These improvements allow employees to spend more time on activities that require decision-making, quality control, and direct supervision.

The goal is not necessarily to eliminate employees from warehouse operations. Instead, it is to make better use of available labor by reducing repetitive transportation and handling responsibilities.

For facilities experiencing labor shortages, rising labor expenses, or increasing order volumes, this can be an important component of a long-term warehouse fulfillment strategy.

4. What Role Do Robotics Play in Century Conveyor Systems’ Warehouse Fulfillment Solutions?

Robotics provide another layer of automation that can improve warehouse fulfillment by handling transportation activities that would otherwise require manual equipment or employee involvement.

Century Conveyor Systems offers robotic fulfillment solutions using two primary technologies: Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs).

Although both technologies transport materials throughout a facility, they operate differently and serve different applications.

Automated Guided Vehicles (AGVs) follow established navigation paths using technologies such as magnetic tape, QR codes, inductive wires, and laser grids. They are particularly useful for predictable transportation requirements involving pallets, cartons, and other materials.

AGVs can also be equipped with carts or conveyor attachments to accommodate different types of products. They are often integrated with conveyor systems to support transportation between automated and manual processing areas.

Autonomous Mobile Robots (AMRs) offer greater navigation flexibility. Rather than following a fixed physical route, AMRs use sensors and programming to navigate throughout a facility.

This flexibility makes them particularly useful for goods-to-person operations. An AMR can retrieve a tote or container and transport it to a packing line or fulfillment employee, reducing the need for workers to travel throughout the warehouse searching for inventory.

Robotic automation also provides scalability. Businesses can introduce additional robots as fulfillment requirements change rather than committing to a completely fixed transportation infrastructure.

For warehouses seeking greater flexibility, robotics can complement conveyor automation and create a more adaptable fulfillment environment.

5. How Does Century Conveyor Systems Help Improve Order Accuracy and Reduce Product Damage?

Order accuracy and product condition are essential parts of warehouse fulfillment. Shipping the wrong product, sending an incomplete order, or damaging merchandise during transportation can lead to returns, additional expenses, and dissatisfied customers.

Many fulfillment problems originate from inefficient material handling processes. Products may be transferred between workstations multiple times, handled unnecessarily, or transported through poorly designed accumulation areas.

Century Conveyor Systems addresses these challenges through equipment designed to improve product movement and reduce unnecessary handling.

For example, conveyor diverts can automatically direct cartons toward their appropriate destinations. This reduces the need for employees to manually reposition every package as it moves through the facility.

Accumulation conveyors can also help protect products during transportation. Century offers zero-pressure and minimum-pressure accumulation solutions that use sensors and controlled spacing to manage how products move along a conveyor.

Zero-pressure accumulation prevents products from touching one another, while minimum-pressure accumulation allows products to make light contact. These technologies are particularly useful when handling fragile merchandise or products that could be damaged by excessive contact.

Belt conveyors provide another advantage by offering stable transportation for smaller parcels, polybags, and irregularly shaped cartons.

By combining appropriate conveyor equipment, automated routing, and controlled product movement, warehouses can create fulfillment processes that reduce avoidable handling errors and product damage.

6. Can Century Conveyor Systems Design a Warehouse Fulfillment System Around an Existing Facility?

Yes. Warehouse automation should reflect the physical characteristics and operational requirements of the facility where it will be installed.

Every warehouse has different constraints, including available floor space, ceiling height, product dimensions, shipping volumes, existing equipment, and employee workflows. A standardized system may not address these requirements effectively.

Century Conveyor Systems provides system design and engineering services to develop material handling solutions around individual warehouse operations.

Its approach includes evaluating the facility, determining the appropriate equipment, validating system designs, and managing implementation.

For example, a warehouse with limited floor space may benefit from vertical transportation solutions such as spiral conveyors. These systems move products between different facility levels using a compact spiral configuration.

A facility with extensive pallet transportation requirements may need a combination of pallet gravity conveyors, chain-driven live roller conveyors, and pallet drag chain systems.

Meanwhile, a fulfillment center handling smaller parcels may benefit from belt conveyors, roller conveyors, and automated sortation equipment.

The important consideration is how the equipment works together. A successful warehouse fulfillment system should support the movement of products from one operational stage to the next without creating unnecessary congestion or inefficient work patterns.

By engineering solutions around existing facility requirements, Century helps businesses pursue automation without assuming that every warehouse needs the same equipment configuration.

7. What Is the Difference Between Conveyor Automation and Robotic Fulfillment?

Conveyor automation and robotic fulfillment both improve warehouse productivity, but they solve different material handling challenges.

Conveyor systems typically move products along established transportation paths. They are particularly effective when products need to travel between predictable locations, such as packing stations, sorting equipment, accumulation areas, and shipping docks.

Robotic fulfillment equipment provides more flexible transportation capabilities. AGVs and AMRs can move products, totes, and pallets through warehouse environments without requiring every transportation route to be built into a fixed conveyor network.

The main difference is how products are transported.

Conveyors provide continuous movement along an engineered pathway, while mobile robots offer point-to-point transportation and greater flexibility when navigating changing warehouse environments.

Neither technology is automatically the better choice for every application.

A high-volume distribution center may benefit from conveyors because they can continuously transport large quantities of products through established processing areas. Another facility may benefit more from AMRs because its inventory movement requirements involve multiple destinations and changing transportation needs.

In many cases, combining both technologies produces the most effective result.

Century Conveyor Systems offers conveyor and robotic fulfillment solutions that can work together as part of a broader warehouse automation strategy.

8. How Does Century Conveyor Systems Support Different Types of Products and Order Volumes?

Warehouses rarely handle only one type of product. Depending on the industry, a fulfillment operation may process small polybags, standard cartons, irregular packages, drums, oversized products, or heavy pallets.

Each product category creates different material handling requirements.

Small packages may require stable belt transportation, while heavier products may need roller conveyors or specialized pallet handling equipment. Fragile items may require controlled accumulation to prevent products from colliding during transportation.

Century Conveyor Systems offers different equipment configurations to accommodate these varying requirements.

For example, modular belt conveyors are useful for applications that require specialized belt characteristics, easy cleaning, or simplified maintenance. Live roller conveyors provide powered transportation for cartons, while gravity conveyors can support staging and manual processing areas.

For larger loads, pallet conveyors provide stable transportation based on the weight and characteristics of the materials being handled.

System flexibility also matters when order volumes fluctuate. A warehouse may experience significant seasonal demand, promotional surges, or long-term business growth.

An appropriately engineered warehouse fulfillment system should account for these changes. Businesses can benefit from selecting equipment that supports current operations while allowing opportunities for future expansion.

Century’s robotic fulfillment solutions also offer scalability, allowing additional mobile robots to be introduced as operational requirements increase.

9. Does Century Conveyor Systems Provide Warehouse Controls and Software Integration?

Yes. Warehouse automation requires more than physical equipment. Controls and software help coordinate the movement of products and ensure that different components of an automated system operate together.

Century Conveyor Systems provides controls and software solutions that include control panel fabrication, Programmable Logic Controls (PLC), Warehouse Management Systems (WMS), and Warehouse Control Systems (WCS).

These technologies support the coordination of warehouse equipment and operational processes.

Programmable Logic Controls help manage equipment behavior, including conveyor movement, sensors, product transfers, and automated sequences.

Warehouse Management Systems support broader warehouse activities, including inventory management and order processing.

Warehouse Control Systems help coordinate automated material handling equipment and direct product movement throughout the facility.

Integrating the appropriate controls and software is important because disconnected systems can create operational inefficiencies. Equipment may function independently while failing to support the overall movement of products through the warehouse.

A properly designed automation solution considers both the mechanical equipment and the controls responsible for coordinating its operation.

For businesses investing in warehouse fulfillment automation, this integrated approach can help establish a more consistent and manageable operation.

10. How Does Preventative Maintenance Affect Warehouse Fulfillment Performance?

Even a well-designed warehouse automation system requires regular maintenance to maintain reliable performance.

Conveyor breakdowns, worn components, electrical problems, and equipment malfunctions can interrupt product movement and create bottlenecks throughout a fulfillment operation.

Because conveyor systems often connect multiple warehouse processes, a problem in one section can affect several downstream operations.

Preventative maintenance helps reduce the likelihood of unexpected equipment failures by identifying potential problems before they develop into major disruptions.

Century Conveyor Systems offers conveyor preventative maintenance, repair services, replacement parts, and ongoing support.

Its service capabilities include mechanical and electrical installation, conveyor repairs, and maintenance programs designed to support material handling equipment.

Century also provides 24/7 support services and parts assistance for conveyor systems.

The company highlights more than 40 years of conveyor experience and maintains a service department with technicians serving the New Jersey, Pennsylvania, and New York metropolitan area.

Maintenance should be considered during the initial planning of a warehouse fulfillment project rather than treated as an afterthought. Equipment accessibility, replacement components, and service requirements can all influence the long-term performance of an automated system.

A proactive maintenance strategy helps businesses protect their automation investment and maintain consistent warehouse operations.

11. Can Century Conveyor Systems Help a Warehouse Expand Its Automation Capabilities Over Time?

Yes. Warehouse automation does not always need to happen as one large installation.

Many businesses prefer to introduce automation in phases, particularly when they need to maintain existing operations during implementation or manage capital expenditures carefully.

Century Conveyor Systems offers project management, system design, project phasing, and installation services that support warehouse automation projects.

A phased approach allows businesses to prioritize the areas experiencing the greatest operational challenges.

For example, a distribution center might begin by automating transportation between packing stations and shipping areas. Once that system is operating effectively, the business may introduce additional sortation equipment or robotic transportation.

Another facility may prioritize pallet movement before investing in smaller-package fulfillment automation.

The advantage of this approach is that businesses can address immediate operational needs while planning for future improvements.

However, future expansion should be considered during the initial system design. Equipment placement, available floor space, control architecture, and transportation pathways can all affect how easily additional automation can be introduced.

Century’s scalable conveyor and robotic fulfillment solutions provide opportunities for businesses to develop their automation capabilities as their operational needs evolve.

12. Why Choose Century Conveyor Systems for Warehouse Fulfillment Automation?

Choosing an automation partner is an important decision because warehouse fulfillment equipment affects productivity, labor requirements, shipping performance, and long-term operating costs.

Century Conveyor Systems positions itself as a full-service material handling automation integrator for warehouses, distribution centers, and fulfillment facilities.

One of its main advantages is its ability to support multiple aspects of an automation project through a single provider.

Rather than focusing exclusively on conveyor installation, Century offers a broader range of capabilities, including:

  • System engineering: Designing material handling solutions around warehouse layouts, product characteristics, and operational requirements.
  • Conveyor automation: Providing belt, roller, pallet, extendable, and specialized conveyor systems.
  • Robotic fulfillment: Integrating AGVs and AMRs for automated transportation and goods-to-person applications.
  • Sortation solutions: Helping warehouses direct packages toward appropriate processing and shipping destinations.
  • Controls engineering: Providing PLC systems, control panels, and warehouse software integration.
  • Storage solutions: Offering shelving, racking, picking modules, mezzanines, and automated storage solutions.
  • Project management: Coordinating project design, validation, installation, and implementation.
  • Maintenance and service: Supporting conveyor equipment through repairs, preventative maintenance, and replacement parts.

This range of capabilities allows Century to consider the entire warehouse fulfillment process when developing an automation strategy.

The company also emphasizes a turnkey project approach, managing activities from system design and validation through installation and start-up support.

For businesses looking to improve fulfillment performance, working with an integrator that understands both individual equipment and the larger material handling system can make a meaningful difference.

Final Thoughts: Improving Warehouse Fulfillment With Century Conveyor Systems

Warehouse fulfillment is becoming increasingly demanding as businesses work to process orders faster, manage labor expenses, and maintain reliable shipping operations. Improving performance requires more than adding individual pieces of equipment. It requires an integrated approach to material handling, transportation, automation, and warehouse controls.

Century Conveyor Systems provides engineered warehouse fulfillment solutions that combine conveyor technology, robotic automation, sortation equipment, controls, and ongoing service capabilities.

Whether a facility needs to automate carton transportation, improve pallet handling, introduce goods-to-person robotics, or modernize an existing conveyor system, the right automation strategy starts with understanding the specific challenges within the operation.

By designing systems around individual warehouse requirements and considering opportunities for future expansion, Century helps businesses build more efficient material handling operations.

For organizations evaluating their next warehouse fulfillment project, Century Conveyor Systems offers an opportunity to work with an experienced automation integrator focused on improving warehouse performance from design through implementation and ongoing support.
Warehouse automation trends that will dominate in 2022

warehouse automation trends 2022 blog header image

2021 has proved to be a year of unforgiving supply chain challenges. From shortages in raw materials and important electronic components to understaffed operations and demand congestion. What trends in warehouse automation have been developed to avoid supply chain disturbances in 2022?

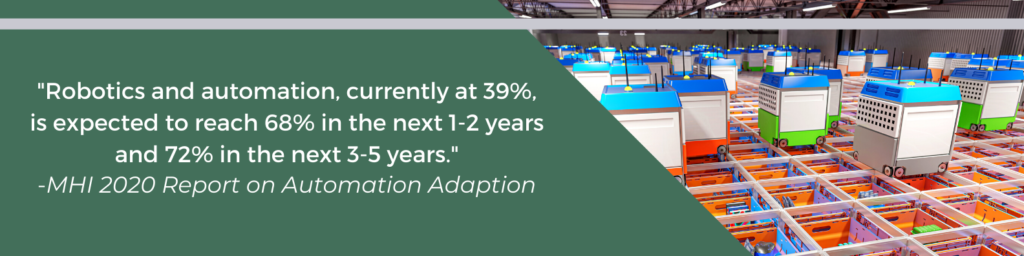
If there has ever been a time to consider warehouse automation, it would be now. Many DCs and warehouses have experienced an increase in demand, whether it be for products, or in clients. Adversely, the required labor needed to accommodate has subsequently dried up. Positions have gone months unfilled, leaving warehouses to turn to higher incentives for applicants or forms of automation that would eliminate the need for such positions. A growing trend among warehouse staffing is to maximize productivity by equipping employees with technology, and the knowledge to utilize them.

2022 automation trends MHI quote 1

1. Co-op automation

Voice-to-pick

Humans and machines working together, and not as counterparts, can eke the most efficiency out of warehouse operations. Voice-to-pick solutions, when combined with a robotic pick module, benefits when a human operator can continually pack orders, and use voice commands to operate a pick solution for the next order.

Wearables

Employees can be equipped with a plethora of devices to boost accuracy and productivity. Tablets running WMS software can be outfitted with wrist or armbands, so employees can always have both hands free. Enabling on-the-go access to inventory and order information keeps operators on-task, instead of having to access a static terminal.

2. Developments in warehouse automation technology

As new technology becomes more developed and available, so does the functionality of specialized solutions. Every warehouse is different, which means unique material handling challenges are posed for solutions provides to tackle. A few automation systems that have seen continued usage and advancements in 2021, and are expected to be major focuses in 2022 include:

  • 5G connectivity adaption
  • Warehouse distribution drones
  • Climbable pick robots
  • WMS automation integration platforms
  • Micro-fulfillment
  • Advances in machine vision
  • Electric standard (UL and ISO) revisions
2022 automation trends MHI quote

Century is constantly keeping up with new trends and technology, all in an effort to engineer the absolute best in efficiency systems for our clients. Our firsthand experience of the stressors has provided us with the insights to recommend scalable and dynamic warehouse solutions. 2021 has been unkind to all facets of the supply chain, and new warehouse technology and processes are in place to make sure thereโ€™s not a repeat in 2022. Get in touch with one of our automation experts and re-engineer the efficiency of your warehouse.

3. A focus on domestic supply chain partners

Supply chain turmoil, while affecting all involved, greatly disrupted those using overseas resources. Port congestion, expensive container prices, sky-high shipping fees, and the Delta variant have strangled international lines. In response, companies are searching closer to home for materials and services, avoiding such headaches in the future.

While outsourced partners may be cheaper up-front, eliminating loss and inefficiencies associated with overseas supply chains may prove fruitful after an extended period of using a domestic partner. 2022 will show how many companies decide to make the flip.

4. ScaaS (supply-chain as a service)

While not an entirely new idea for 2021, the expectation is that 2022 will see more users of SCaaS platforms. Essentially, SCaaS follows the footsteps of SaaS (software-as-a-service) by offering users supply chain functions through an external company. While full-service third-party logistics companies exist, SCaaS solutions strive to provide services for every step, from sourcing, manufacturing, transportation, procurement, reporting, and more.

With more and more companies strapped for staffing and adequate resources, enrolling in a tailored SCaaS platform can alleviate some of those operational pressures. Warehouse flexibility should be a key implementation goal as the new year inches closer.

5. DTC eCommerce disruptors

The explosive and continued growth of eCommerce continues to lead companies to invest in online shopping. For example, Shopify, a leading eCommerce platform grew 110% YOY in the first quarter of 2021, achieving a total revenue of $988.6 million. Industries that typically see a majority of sales via traditional brick-and-mortar channels have dipped their toe into direct-to-consumer sales, such as the alcohol industry, with companies like Drizly experiencing significant demand for home-delivery services. This boom has turned many eyes to new customer behaviors, and 2022 will see many larger organizations adopting DTC eCommerce warehouse automation systems as an additional revenue source.

In summary, the major focus for 2022 is FLEXIBILITY. Ensuring operations can scale quickly due to outside stressors like demand increases and staff shortages is the next step in continuous company improvement. 2021 was the year of reactivity, a learning lesson that hit hard and continues to sting. 2022 will be the year of proactivity- building up resources to avoid losses, establishing high-performing automation, and closely adapting to target consumer behaviors will separate the organizations that will thrive, from the ones that will remain stagnant or even worse, fail.

The Lifesaving Importance of a Responsive Medical Device Distribution Operation

medical device and equipment blog post header
medical device distribution blog header post

If the pandemic taught us anything, itโ€™s that distribution operations for medical devices and equipment MUST be poised to accommodate for fluctuations in demand and in supply chain shortages. A multitude of factors can cause important distribution of key medical items to slow:

  • Manufacturing material shortages
  • Shortages in unskilled labor
  • Distribution that cannot handle significant demand
  • Additional safety protocol and procedures
  • Local government enforced restrictions
  • Use of manual operations where automation could be integrated
  • Outdated or ineffective inventory management systems
  • Inaccurate item storage and replenishment

Ensuring stable operations and quick delivery of medical products is paramount to the health and safety of its users, and the integrity of the company providing the distribution. Hospitals and practices are depending on their shipments to treat their patients, and an ineffective distribution system simply wonโ€™t cut it.

Dynamic inventory visibility


The first step to updating medical device and equipment distribution is always knowing the status of inventory items. Warehouse visibility is critically important for fulfilling orders, tracking output rates, and replenishing stock.

A warehouse management system (WMS) like SAP or Oracle. These platforms provide insight into inventory, quality procedures, production supply, delivery and transportation specifications, and labor management. The WMS collects data throughout your warehouse by utilizing process touchpoints, like an order manifest or a shipping label scan, to accurately track and provide details on all movements.

Depending on the solutions integrated within a facility, program integrations can be added to provide additional functionality. For example, Hytrol provides their Pivot software, so that their systems can more easily communicate and provide data to the entirety of the WMS.

Itโ€™s important to accurately have a grasp on the daily ongoings of every warehouse operation, and before investing in any automation, having full visibility of your operations is a must.

Reliable and quick order fulfillment


With medical devices and equipment, the time when an order is manifested, to when it ships out should always be analyzed for continuous improvement. What manual operations do you currently employ that could be automated? Essentially, every link in an order fulfillment process has an equivalent automated solution that will greatly outpace manual labor.

With medical devices and equipment, the time when an order is manifested, to when it ships out should always be analyzed for continuous improvement. What manual operations do you currently employ that could be automated? Essentially, every link in an order fulfillment process has an equivalent automated solution that will greatly outpace manual labor.

  • Box forming- case formers and erectors, robotic arm formers
  • Box sealing- case sealers, tapers
  • Movement and picking of items- conveyors, shuttles, AGVs/AMRs
  • Print and Apply- Automatic shipping label printers and applicators
  • Sortation- Sorter conveyors and shuttles
  • Palletizing- Automatic robot-arm palletizers/depalletizers
  • Storage- canted racking systems, ASRS units
  • And much more

System downtime avoidance


System downtime is a constant threat to a continuously profitable operation. The importance of proper maintenance and ongoing support is paramount to keeping orders shipping on time and clients satisfied. Unplanned downtime can cost companies up to $250,000 per hour, with 82% of businesses experiencing at least one system outage over the past three years (source).

In the medical devices and equipment vertical, unexpected downtime should be prevented at all costs, considering the importance of the contents being handled. Before a new solution is engineered and installed, plan a routine maintenance schedule. This may include technicians visiting your site a few months out of the year to do a check-up and replace anything that may be worn or broken. Itโ€™s also good practice to maintain a parts supply, in the event a critical part fails, and an immediate replacement is needed

Automation for sterile environments


In the wake of the pandemic, various companies have fortified their approach to employee safety and facility cleanliness. In a distribution facility for medical devices and equipment, where sanitization is a necessary step in the supply chain, automation can integrate as well.

AMRs (autonomous mobile robots) have recently been implemented with sanitization functionality. Tooling is switched out for bacteria-killing UV lights, or a disinfecting spray. Autonomous floor cleaning robots are also common, providing reliable, routine cleaning while forgoing the need for an employee to operate a cleaner manually.

Flexible warehouse engineering


Warehouse distribution processes can experience a significant downward trend of output efficiency by a variety of outside factors if future-focused automation options arenโ€™t accounted for in the engineering phase. When selecting a solution, always ensure that your engineer leaves room for future systems to be installed or additional functionality for existing systems (retrofitting)

Consider the trajectory of your business. Are you expecting a new product line or special handling process (such as cold storage) to be integrated in the future? Careful evaluation should be practiced, as warehouse space is precious.


Century Systems has had experience with engineering distribution systems for medical devices and equipment companies (hereโ€™s a case study on a past client of ours), and we understand the importance of reliable and stable output rates. All of our projects are designed to be as efficient, turnkey, and results-driven as possible.

10 Tips on How to Implement Powerful Automation for Wholesale Distribution

wholesale automation solutions blog header image
10 powerful automation solutions for wholesale distribution blog header image

Operating a wholesale distribution process is a complex series of moving parts. Each organization has a mix of inventory and typically involves itself in the process of purchasing, storing, and selling products to end buyers like retailers or other wholesalers. With the number of items wholesalers handle daily, itโ€™s no surprise that many invest in automated solutions to enhance operations.

โ€œProduct availability and quality is a key element, together with a delivery service that is accurate and efficient is a driving force for businesses.โ€

Sedat Kaan Hendekli
Head of Operations at JJ Foodservice
Source: BetterWholesaling.com

The burning question is, what automation works best for the wholesale industry? Weโ€™ve compiled a list of 10 automation applications that weโ€™ve experienced integrating in the past for some of our wholesale clients.

1. Robust inventory management system


The ability to have complete visibility of a wholesale operation at all times is paramount to effective distribution. A warehouse management system (or WMS) stores vital information such as scan dates, storage location, supply quantities, and a multitude of SKU data for ordering. Depending on the manufacturer, automation systems can integrate with a WMS and provide even more functionality and reporting data.

Besides being a source of important product information, a WMS can apply that information within your warehouse operations. For example, if the wrong item is picked and placed on an outbound conveyor, the scan tower will read the label and the WMS will recognize it is in the wrong batch, stopping that section of the conveyor and sounding an alarm for a worker to remove the incorrect item.

2. Robotic palletizing for redistribution


For wholesalers who use pallets, either robotic palletizing solutions automatically build and break a pallet. A wide variety of robots and end of arm tooling can accommodate most carton sizes and complex layer build configurations for pallets.

The speed and stability of robotic palletizing greatly outpace that of manual pallet building and even lift trucks. For further automation, completed pallets can be conveyed from a robotic cell to an inline stretch wrap operation, replacing tedious manual wrapping.

3. Rapid order fulfillment


Delivery expectations have greatly increased in recent years, primarily due to the prevalence of same or one-day shipping offerings online. Those expectations have extended to wholesaler clients, whose operations must match a competitive wholesale e-commerce landscape. Much like adjacent markets (third-party logistics, for example), automating order fulfillment is key to satisfying customers, while also offering an edge over the competition who donโ€™t have quick shipping incentives.

A tried-and-true conveyor system is best suited for order fulfillment. Depending on the size of the warehouse itโ€™s installed in, and the product being transported, a conveyor system can include a variety of automation:

  • Pack Tables
  • Carton Forming
  • Carton Sealing
  • Label Printing and Application
  • Destination Sortation
  • Loading Assistance

4. Automation-aided picking


For most wholesale operations, an inventory boasting thousands of different products and items is normal. Order picking is usually where inefficiencies are identified, as manual labor is greatly outpaced by a variety of automation solutions.

  • ASRS
    • An ASRS (Automatic Storage and Retrieval System) uses a crane attached to a horizontal and vertical track, scaling the racking structure, and using extendable forks to handle pallets. The operator terminal provides information on what product is stored where, and the ASRS operates when a retrieve or store command is inputted.
  • AMR/AGV
    • Automated Guided Vehicles (AGV) and Autonomous Mobile Vehicles (AMR) both provide a multitude of functions, typically moving items from one area of the facility to another, absent of human interaction. The difference between the two is in the way it senses the environment. AGV’s move by using a sensor that follows a set path (typically a form of sticker or tape on the ground). AMRs move by sensing objects around them, and learning an optimal path. In this sense, both have applications that one or the other is better suited to.
  • Shuttle Systems
    • For the best of both worlds, a shuttle system utilizes pick robots within a racking structure. When an order is being fulfilled, the robot navigates to the compartment where the item is held, retrieves it, and brings it to the workerโ€™s pack station or an item dispenser receptacle.

5. Flexible packaging


It goes without saying that a massive catalog of products varying in weight and size would need packaging solutions just as versatile.

Automation systems, such as conveyors, are manufactured in different dimensions and applications and can be engineered in a warehouse layout to accommodate cartons of varying sizes and fragility.

We go in-depth on carton packing solutions in our 3PL Automated Box Packing Solutions for Powerful and Profitable Order Fulfillment post.

6. Reliable sortation


Sortation systems separate products for induction into individual lanes typically associated with an outbound destination. Various types of sortation and conveyor systems are often connected to comprise a fully functioning material handling solution.

Wholesalers supply a diverse range of customers from all over, so quick, and accurate diverts are required to keep items moving and heading to the right destination. Selecting the correct type of sortation system is where the most thought should be put, as it all matters on the dimensions of the product being moved.

7. Effective pallet handling


Pallets can be cumbersome to transport throughout a warehouse, so offering simple solutions to warehouse workers to decrease human touchpoints with pallets can prove effective.

  • Pallet conveyor
  • Pallet flow rails
  • Pallet lifters
  • Pallet positioners
  • Gravity racking
  • Tugger and dolly attachments for AGVs

8. Maximize warehouse space


Wholesale warehouse space is extremely precious. Ensuring thereโ€™s room for storage, order fulfillment, loading, maintenance, employees, and office- all while following building codes, is no easy feat. If space is at a premium, but additional systems will need to be implemented in the future, a few capacity-saving solutions can provide some leeway.

  • Inclined and spiral conveyors
    • Suspended conveyor sections above the warehouse floor.
  • Mezzanine structures
    • Walkways and platforms suspended above the warehouse floor.
  • Narrow-aisle racking
    • Special forklifts can be used to access pallets in these lanes
  • ASRS
    • Automated cranes travel within narrow-aisle racking structures to retrieve pallets
  • Shuttle system
    • Items are held in compartments within a complete racking structure, eliminating aisles completely.

9. Accurate reverse logistics


Returns are a constant area of disconnect in operations when it comes to order fulfillment. There needs to be a planned intake process to return the items to storage and re-fulfill the order with the correct products.

When returns enter back into a warehouse, theyโ€™re put in a separate staging area. Depending on the condition of the item, or whatever the nature of the return is, it may be returned to inventory, sent to another distributor who sells discount items or discarded.

Once a return item has been rescanned in the system, the customerโ€™s order will either be marked as fulfilled (so they can receive their money back) or another order will be placed (in the event they were sent the wrong item, but they still need the correct item sent to them).

10. Forecast planning and optimization


Warehouse automation continues to improve as newer technologies are created and adapted. Artificial intelligence (AI), drones, machine vision, voice-to-robotic-pick, and warehouse data-driven learned actions are just a few examples of whatโ€™s on the horizon.

The wholesale industry is only going to grow, and understanding the current constraints of your warehouse, and the projected sales volume per quarter should be your guiding logic as to what automation can be implemented, and when.


Century Systems has had experience engineering systems for the wholesale industry (hereโ€™s a case study on a past client of ours), and we understand the importance of reliable and stable output rates. All of our projects are designed to be as efficient, turnkey, and results-driven as possible.

AGV and AMR vs. Conveyor Systems: Drive Efficiency With The Best Solution for your Warehouse.

agv and amr vs conveyor comparison blog post header image
agv and amr vs conveyor system comparison blog post header image

Automatic Guided Vehicles (AGV) and Autonomous Mobile Robots (AMR) have existed for years now, offering robotic material handling operations for a multitude of warehouse operations. The industry is well aware of its pros and cons, and supply chain executives are content with placing them within their arsenal of automated warehouse solutions.

The much harder decision when automating is understanding which solution will provide the most benefit, as opposed to if it will at all. In the case of AGVs and AMRs, conveyor systems are tried and true forms of automation that continue to provide exceptional output and return-on-investment. While both solutions differ in engineering and functionality, both exist for the same goal- reliable, stable, and quick movement of items. How do AGVs/AMRs stack up against traditional conveyor systems? Where does one solution shine, while another does better in a different application?

Century has experience integrating both and understands where and how these systems outperform one over the other. We wanted to share some of our insights so you can evaluate what works best for your warehouse.


newsletter sign up element

AGV and AMR

AGVs and AMRs are often grouped together, mostly because the operations they perform overlap with each other. The single main difference between the two is its form of sensing and moving throughout the environment. AGVs move by using a sensor that follows a set path (typically a form of sticker or tape on the ground-hence the word โ€œguidedโ€ in its name). AMRs move by sensing objects around them, and learning an optimal path (hence the word โ€œautonomousโ€ in its name).

This characteristic defines what operations are typically assigned to an AGV or an AMR. Essentially, AGVs work best at moving cartons and pallets across the facility with little to no variation in its traveling path. AMRs shine in picking operations, where it would not have a set path.

AGV


Effective in moving, tugging, and towing cartons or pallets from a single location to another.

  • Carts
  • Tuggers
  • Lift-Truck
  • Pallet Jack
  • Unit Load

AMR


Assistance in multi-variable operations that require diversion in movement paths.

  • Picking
  • Sortation
  • Inventory Control
  • Sanitization

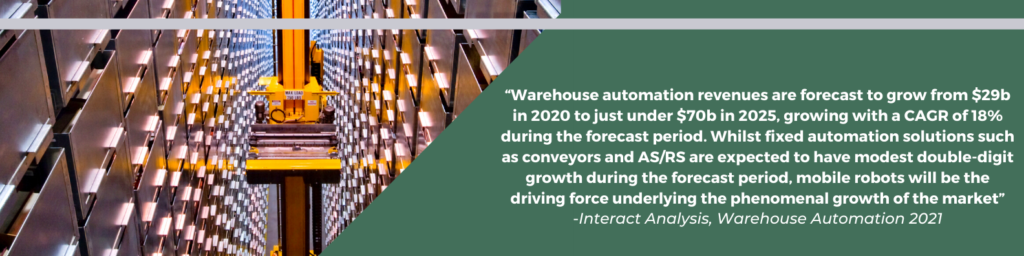
AGVs and AMRs have seen expanded use over the course of the past year, and most new warehouses are built with the notion that automation will be implemented at some point. According to Research and Markets, United States, Germany, U.K., China and Japan are going to lead the market with an annual demand of more than 200,000 mobile robots (AGV & AMR) by 2026.

To put the cost-effectiveness of an AGV and AMR into perspective, Annual costs for a forklift operator can run up to $50,000. If a forklift has to be operated around the clock, then at least 3-4 drivers are needed. Adding the invest costs of $10,000 for a forklift truck to the personnel costs, the annual costs for one forklift come to over $200,000 (ResearchAndMarkets.com). Depending on the output of the warehouse, operating AGVs and AMRs can save thousands over traditional manually operated lift trucks.

Automated robotic solutions continue to improve as newer technologies are created and adapted. Artificial intelligence (AI), machine vision, voice-to-robotic-pick, and warehouse data-driven learned actions continue to provide added functionality and benefit to AGVs and AMRs (primarily the latter). This makes AGVs and AMRs a forward-facing implementation, as abilities are added to their repertoire of functionality through the advancement of warehouse technologies and software capabilities.

Conveyor

Conveyor systems are the typical solution of any automated operation, offering a continuously moving assembly line to quickly complete the processing and distribution of a package. Conveyors use belts or rollers to move cartons or pallets, powered by motors. Each warehouse that employs conveyors has a specially engineered layout, consisting of a variety of conveyor sections, depending on function.

Conveyor Section Types

  • Infeeding
  • Straight
  • Curved
  • Incline
  • Decline
  • Divert
  • Merge
  • Switch
  • Outfeeding

Conveyors produce the best results when implemented in fast-moving post-production operations such as order fulfillment, product distribution, sortation, and crossdocking. Conveyors are highly customizable, with the number of systems that can be added to the conveyor line spanning from carton forming to in-trailer loading, and everything in-between. Conveyors have proved the test of time as being the main system of reliable and quick movement in a warehouse. Thereโ€™s a reason theyโ€™re still in use for over 100 years. The output rate is unmatched and its simplicity in design help it to easily integrate with other cutting-edge automation solutions.

The Most Important Factor: Your Warehouse

If you were to ask us what system we would use, we would ask โ€œwhatโ€™s your warehouse like?โ€. This is the number one question you should ask yourself as youโ€™re exploring solutions. The effectiveness and benefit of these solutions are only relevant if integrated correctly in your distribution center, warehouse or facility.

To simply it even further- think on your answer to this question. Can your operations continue effectively if you install a โ€œbolted-downโ€ conveyor system. If the answer is a definite โ€œNOโ€, then youโ€™ll most likely benefit more from the use of AGVs and AMRs. A fully engineered conveyor system is not mobile, and if your warehouse has limited space, or needs open lanes for lift trucks to travel in, a conveyor system may not be ideal. Thatโ€™s not to say itโ€™s impossible to engineer, but an AGV or AMR would be a more realistic solution.

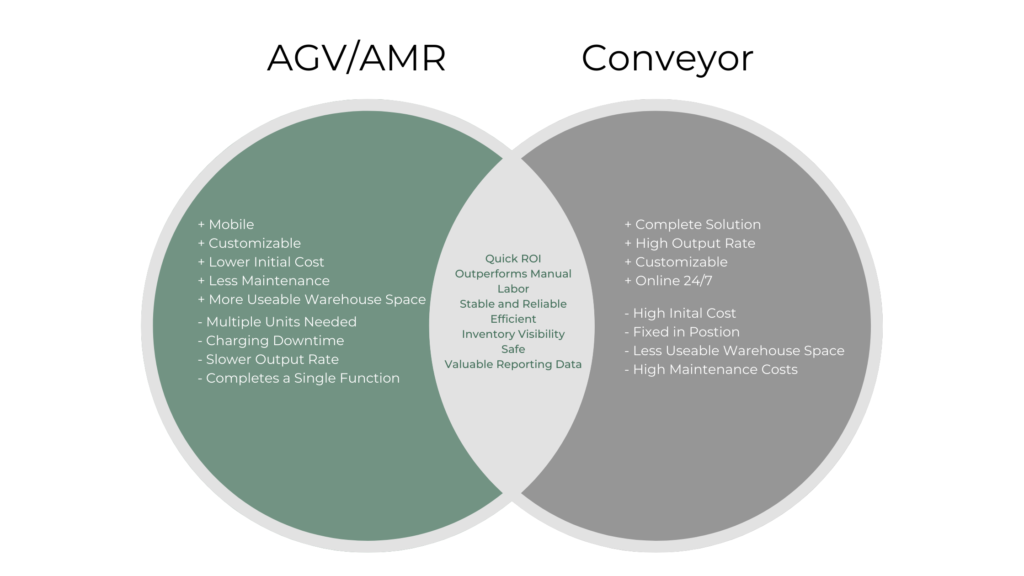
With that in mind, hereโ€™s our comparison between AGVs/AMRs and conveyor systems.

The Comparison

AGVs AMRs Vs Conveyor

Key Takeaway

Both systems will complete the task of transporting product across a warehouse, itโ€™s that your operations and facility space will determine which one will work better.

AGVs/AMRs are ideal for warehouses that have:

  • Limited space and cannot install a conveyor system.
  • Extensive pick operations
  • Forklifts transporting the majority of items
  • A healthy output rate (5,000 to 20,000 cartons shipped per day)

Conveyor systems are ideal for warehouses that have:

  • Flexible space arrangements
  • A variety of package types
  • Extensive sortation operations
  • A high-output rate (20,000+ cartons shipped per day)

Both AGVs/AMRs and conveyors can benefit in more ways than one, and in many cases, are both implemented in a facility to maximize distribution operations.


century conveyor boilerplate element

Ahead of the Trend: The Rise of eCommerce in the Wine and Spirits Industry

rise of ecommerce in wine and spirits industry blog header image
rise of ecommerce in the wine and spirits industry blog header image

Online sales directly to the consumer in the wine and spirits industry used to be a tiny niche, compared to typical distribution methods, but the newest trend, fueled by COVID, is anything but.

In 2020, bars and restaurants shut their doors, leading consumers to make the decision to shop online. U.S. E-commerce sales of alcohol increased more than 80% in value during the pandemic (IWSR). A year later, the sales have plateaued, but are still 15% to 20% higher than pre-pandemic levels. Consumers turned to online shopping because of an external factor, and a surprising number have stuck around after that factor has been eased.

Online liquor stores have seen increases in sales, spurring investor interest. Last February, Uber purchased Drizly for $1.1 billion (Barrons). Consumer interest is certain to increase in eCommerce purchasing as users adopt the buying behavior, and experience the benefits over traditional liquor store visits. Along with Drizly, a few other online liquor stores run in the races, including:

Uptown Spirits

ReserveBar

Thrive Market

Wine.com

Bright Cellars

Nestor Liquor

Minibar

Flaviar

Wine.com

How does this affect the wine and spirits industry? Supply chains will have to accommodate for order fulfillment, that is having the necessary material handling solutions in place to ensure an order gets packed, labeled, and sorted to its end destination. This is quite different from what is typically processed in a wine and liquor distribution operation.

Cartons (usually packed within 6 bottles) are sent to be palletized or loaded in a truck, which makes deliveries to liquor stores, bars, and restaurants. With an online order, each package is customized and can contain a variety of items (kitting).

Wine and liquor warehouses will have to store individual items, accurately pick and pack them, apply a shipping label, and send them to the customerโ€™s doorstep safely and within a few daysโ€™ time.

Integrating order fulfillment is a carefully planned and engineered project, but the long-term growth and profits will dwarf the initial investment once implemented fully.

Order fulfillment is one of Centuryโ€™s specialties. Weโ€™ve had experience in the past engineering systems specifically for eCommerce operations, and weโ€™d like to pass along our recommendations on the solutions that are used.

1. Storage and Pick Modules

Managing a fully stocked wine and spirits warehouse can get complicated when a large variety of products are offered. This creates a need for both short-term and long-term pallet storage. Automation in the form of an ASRS (automatic storage and retrieval system) can rapidly retrieve pallets that need to be distributed or store long-term inventory in the most optimal spot within a racking system.

An ASRS uses a crane attached to a horizontal and vertical track, scaling the racking structure, and using extendable forks to handle pallets. The operator terminal provides information on what product is stored where, and the ASRS operates when a retrieve or store command is inputted.

2. Conveyor System

A tried-and-true conveyor system will be the most accurate, simple, and efficient solution for a wine and spirits warehouse. Conveyors are dynamic in the sense that there are hundreds of additional solutions that can be integrated in the layout. Being highly customizable, each conveyor system is engineered according to the layout of the wine and spirits operation.

In the wine and spirits industry, the key to stable operations is ensuring cartons avoid damage. A zero-pressure accumulation conveyor (like this conveyor, manufactured by Hytrol) does not allow cartons to touch, by properly maintaining space between each and stopping the rollers when the accumulation zone is full. This is especially important when fulfilling specific customer orders that may include unevenly sized items.

3. Pack Tables

In order fulfillment, stations are positioned at infeeding operations so that orders can be packaged and sent to a label application. A worker or autonomous robot picks the products and brings it to a pack table. The worker checks to ensure that the order is correct in places in any invoicing documents, and places the items in the package with void-fill.

Pack tables are simple to integrate, and sit aside a main conveyor, so that workers can simply push orders from their tables onto the conveying surface.

4. Print and Apply Stations

Affixing identifiable tags on packages is crucial to ensuring their deliverability. Scanners and sensors across the line depend on a readable tag for it to make it to its destination. Print and apply systems do exactly that. However, there are multiple systems depending on the identification process use and where the box must be marked. Applications can roll-on, wipe over, corner wrap, air blow, and stamp labels.

The direction the box must be scanned also plays a role in a solution selection, but it will outpace manual operations regardless.

5. Sortation

Sortation systems separate products for induction into individual lanes typically associated with an outbound destination. Various types of sortation and conveyor systems are often connected to comprise a fully functioning material handling solution.

The type of sortation integrates highly depends on what product is being moved. For a fragile wine and spirits operation, care must be taken in selecting a stable method of diverting the packages. Sliding Shoe and Narrow Belt sorters are best suited for safely, yet quickly, sending items to where they need to be.

narrow belt sortation
Narrow belt utilizes thin belts so that rising directional skate wheels activate when a package is to be diverted down a destination lane.

sliding shoe conveyor sortation
Sliding shoe uses segmented plastic slats that gently divert cartons to an outfeeding conveyor.

6. Warehouse Management System

The ability to have complete visibility of your warehouse inventory at all times is paramount to operating effectively. A warehouse management system (or WMS) stores vital information such as alcohol percentage, storage location, best-by dates for rotation, and a multitude of SKU data for ordering. A WMS can even offer a best shipping rate selector and presents data with correct state alcohol regulations applied.

Besides being a source of important product information, a WMS can apply that information within your warehouse operations. For example, if the wrong item is picked and placed on an outbound conveyor, the scan tower will read the label and the WMS will recognize it is in the wrong batch, stopping that section of conveyor and sounding an alarm for a worker to remove the incorrect item.

7. Reverse Logistics

Returns are a constant area of disconnect in operations when it comes to order fulfillment. There needs to be a planned intake process to return the items to storage and re-fulfill the order with the correct products.

When returns enter back into a warehouse, theyโ€™re put in a separate staging area. Depending on the condition of the item, or whatever the nature of the return is, it may be returned to inventory, sent to another distributor who sells discount items or discarded.

Once a return item has been rescanned in the system, the customerโ€™s order will either be marked as fulfilled (so they can receive their money back) or another order will be placed (in the event they were sent the wrong item, but they still need the correct item sent to them).


Century Systems has extensive experience in integrating warehouse automation systems in the wine and spirits material handling industry. View the video below on a system we engineered and integrated with Fedway Associates.

7 Conveyance Solutions for Robust Handling of Various Product Types

ARB Solutions 2

Conveyor systems are versatile machines, working in tandem with a variety of material handling solutions, ensuring increase output and productivity. Besides the additions of machines in conjunction with a conveyance solution, there exists extended automation for the conveyor system itself.

Belting plays a critical role in how the product moves throughout the system, but typically, most operations use either a roller conveyor or a flat belt. What many do not realize is that belting can be upgraded to automatically position cartons in a way that simplifies various induction steps in the line.

ARB (Activated Roller Belt) technology revolutionizes the way a conveyor system functions by offering automatic aligning and positioning, precise gapping, high-speed sortation and diversion, uniform operator station package distribution, and more.

ARB equipment performs a variety of different functions on the product by utilizing free-spinning rollers that are embedded in plastic belt modules. The rollers can bi-directionally manipulate products in a variety of different angles and trajectories. The rollers can be bi-directional or omnidirectional depending on the usage of that specific belt space. The rollers reorientate themselves rapidly depending on the destination of the package.

ARB equipment can provide substantial throughput benefits while providing a quick return on investment by eliminating time-consuming manual labor and being flexible enough of a solution to apply to a variety of operations.

  • Sortation
  • Depalletizing
  • Singulators
  • Merges
  • Switching
  • Zone Picking
  • Infeeding and Outfeeding

1. Sortation Systems

DARB S4500 Sorting Belt

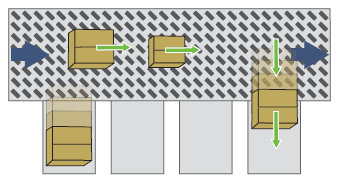
90-degree sortation

Bi-directional right-angle sortation that activates the belt rollers when the carton reaches its divert destination. This form of sortation is high speed, with rates up to 250 packages a minute, in a compact footprint. If your facility distributes a variety of packages, this sortation method can accommodate polybags, crates, top-heavy items, and more, along with typical flat-bottomed cartons.

ARB Sorter S7000

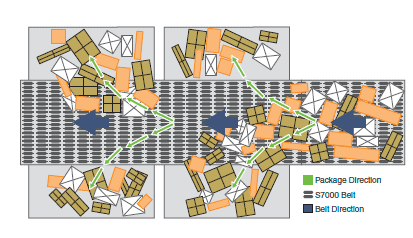
Bulk sortation

In facilities where a continuous flow of a mix of bulk packages is present, ARB equipment can be employed to sort an even volume of packages for downstream processing (operator stations, for example). Due to the bulk nature of the continuous induction, sortation rates can achieve up to 360 packages per minute, automatically avoiding jams.

2. Depalletizing Systems

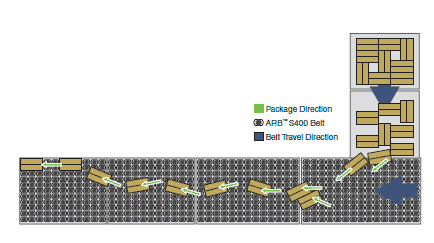
ARB Pallet Layer Descrambling S400

Depalletizing can be a laborious operation if done manually. With ARB equipment in use, omnidirectional track rollers can descramble up to 6 pallet layers per minute and place them in a uniform line, ideal for scanning or picking. By alternating packages left and right on the ARB conveyor, and using the side railing as a guide, packages line up neatly for downstream applications.

3. Singulators

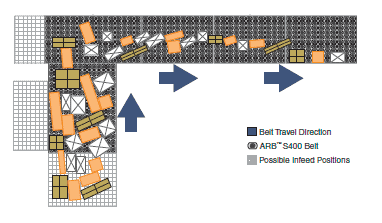
ARB Singulating Belt

Singulating, in this context, means to place the items in a single, congruent line. Depending on induction rates, this could be a continuous line, or broken up into segments (for example, one segment having four packages). ARB equipment moves the undistributed packages from left to right to acquire a straight line, using the railing of the support to gently align the items. This eliminates the need for manual clearing of side-by-sides, recirculation due to miss-sorts, and enables workers to place items on without concern for positioning.

4. Merges

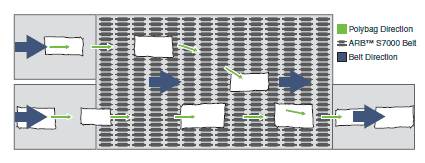
Polybag ARB Merging

Polybag merging

In a polybag-focused operation, reliable merging from multiple infeeds is paramount to downstream processes. ARB conveyor solutions merges infeed conveyors with a high-speed directional belt, while maintaining gapping, and alignment, for later scanning and sortation operations. All of this is completed in a relatively small footprint, as an ARB conveyor is designed to quickly merge the lanes.

5. Switching

Polybag Switching and Aligning

Polybag destination switching

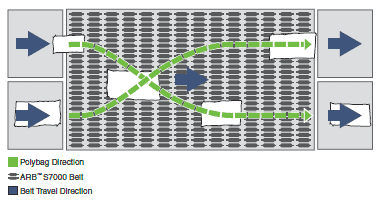
If lanes are not merging, but instead, crossing polybags over each other to their reach their destination lane, an ARB conveyor solution can achieve this efficiently. Much like the merging ARB conveyor, omnidirectional rollers quickly switch polybags into their respective destination outfeeds, while maintaining proper gapping and alignment.

6. Zone Picking

Zone picking

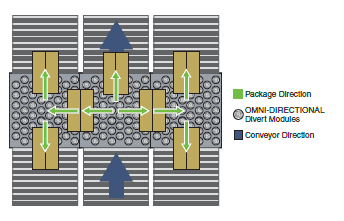
Pick and pass order fulfillment zones can also benefit from ARB equipment inclusion. Manual picking stations can be added to a central conveyor merge, utilizing an omnidirectional sorter to easily pick packages from the main line to be processed, and then re-introduced back to that same conveyor. Order fulfillment can be completed at rates greater than 25 packages per minute, and only needs one 24-volt motor to drive the rollers.

7. Infeeding and Outfeeding

Infeeding and Outfeeding ARB

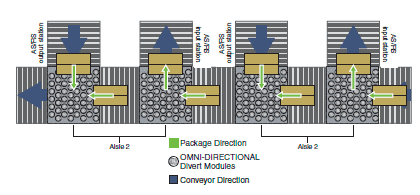
Used in conjunction with an automatic storage and retrieval system (AS/RS), this ARB conveyor combines both infeeding and outfeeding operations. Packages can both be sent to storage, while simultaneously accepting packages coming from storage. This is achieved by utilizing omnidirectional sorters in conjunction with right angle diverters, with alternating flow directions that activate depending on the cartonโ€™s destination. Sortation can achieve excess of 30 packages per minute, while infeed/outfeed rates to an AS/RS can reach 1,800 cases or totes per hour.

Intralox equipment has been successfully implemented by retail, grocery, manufacturing, and direct-to-consumer e-commerce distribution centers. The technology brings value in many applications ranging from high-speed 90-degree sorting to AS/RS infeeding and outfeeding. From increased throughput to flexible package handling and efficiency, Intraloxโ€™s conveyance technologies pick up where traditional technologies end.


Century is a longtime partner and integrator of Intralox, utilizing its innovative ARB equipment technologies throughout a wide range of clients. Together, a truly efficient system can be designed, engineered, and installed to increase output, accuracy, and ROI.